Tag Archives: Preventive Controls

Why Are Food Manufacturers Still Struggling to Prevent Recurring Food Safety Incidents

By Shammi Thakur
No Comments

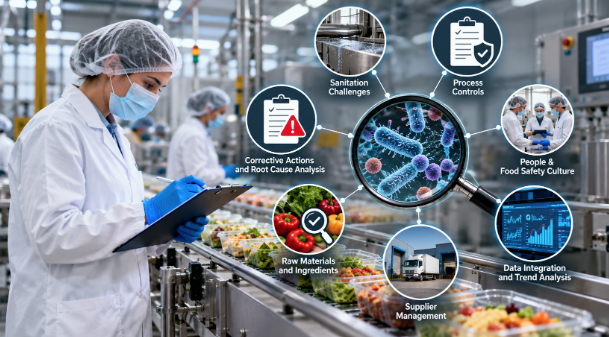
Food safety programs can generate extensive records without necessarily producing a complete explanation of why a problem occurred. A positive environmental sample, a failed sanitation inspection, or a deviation in a critical process parameter may trigger an immediate response. However, if the investigation stops after the affected product is contained and the corrective-action report is closed, the underlying risk may remain.

The challenge is not simply to detect more problems. It is to translate the available evidence into changes that prevent similar failures from recurring.
Why Existing Preventive Controls Do Not Always Work

Food manufacturers operate under established systems for hazard analysis, sanitation, process monitoring, environmental testing, and verification. Under the U.S. Food Safety Modernization Act (FSMA) Preventive Controls for Human Food rule, applicable facilities must implement preventive controls and take corrective action when controls are not properly implemented or prove ineffective. Those actions must address the problem, reduce the likelihood of recurrence, and ensure affected food is handled appropriately.¹

Yet documented procedures cannot guarantee effective execution under every production condition. Equipment changes, maintenance activities, production pressures, inconsistent sanitation practices, and supplier variations can introduce weaknesses that existing controls do not adequately address.

Correcting a Deviation Is Not the Same as Removing Its Cause

Consider a ready-to-eat food facility that repeatedly detects Listeria monocytogenes in the same processing area. Recleaning the affected surface may be necessary, but it may not resolve contamination associated with an inaccessible equipment junction, persistent moisture, ineffective sanitation access, or movement between processing zones.

The initial correction addresses the finding. Root-cause analysis investigates why the conditions that produced the finding existed and whether similar conditions remain elsewhere.

The FDA’s guidance on strengthening food safety through root-cause analysis recommends gathering relevant records, examining possible causes, documenting conclusions, and verifying whether the resulting interventions work.²

For manufacturers, this means resisting the temptation to select the first plausible explanation. Retraining an operator, replacing a component, or revising a cleaning procedure may be appropriate, but the action should follow evidence demonstrating what contributed to the incident.

Testing Has Limits

Microbiological testing and environmental monitoring are important tools for identifying potential contamination. However, a sample provides evidence about the material and location tested, not necessarily the condition of every product lot, surface, or production shift.

The FDA’s environmental sampling guidance explains how environmental sampling helps identify harmful bacteria in food-processing environments and supports risk-based investigation.³ Sampling plans, site selection, timing, and the response to findings therefore matter as much as the number of tests performed.

A negative result after corrective action may be encouraging, but its meaning depends on the hazard, sampling design, operating conditions, and other evidence. Repeated testing without investigating earlier positive findings can create a cycle of detection and recleaning without establishing that contamination has been controlled.

What Recurring Incidents Reveal About Investigations

A particularly important example appears in the FDA’s October 2026 CORE+EP 2025 Annual Report. A historical Listeria outbreak linked to frozen supplemental shakes was investigated in 2018, 2021, and 2023 before being resolved in 2025. The outbreak involved 42 illnesses across 21 states, 41 hospitalizations, and 14 deaths. FDA sampling at the manufacturer identified three positive environmental swabs from a processing area, and whole-genome sequencing found the detected Listeria closely related to the outbreak strain. New traceback information, historical illness records, updated epidemiological evidence, and laboratory findings helped investigators connect the evidence.⁴

The report does not establish that the manufacturer ignored previous warnings or repeatedly failed to implement corrective actions. Instead, the case illustrates the difficulty of resolving an outbreak when relevant evidence is distributed across different investigations and time periods.

For manufacturers, the operational lesson is to examine how information from separate activities can be connected. A laboratory result may become more meaningful when reviewed alongside maintenance records, sanitation history, ingredient traceability, production dates, and previous findings from related locations.

Useful investigation questions include:

  • Have similar findings occurred at the same location, on the same equipment, or during particular shifts?
  • Do deviations coincide with cleaning cycles, product changeovers, maintenance work, or changes in ingredients?
  • Have previous corrective actions produced only temporary improvements?
  • Could the same risk mechanism exist on another production line or at another facility?

The purpose is not to assume that every repeated result has the same cause. It is to identify patterns that warrant investigation and test possible explanations against the available evidence.

How Manufacturers Can Strengthen Root-Cause Analysis

Effective investigations require a documented process that links immediate containment to preventive action and subsequent verification.

  1. Define the problem precisely. Establish what occurred, where it happened, when it was detected, which products may be affected, and which controls were expected to prevent it. Vague descriptions such as “sanitation failure” can conceal several distinct mechanisms.
  2. Assemble cross-functional evidence. Bring together laboratory results, environmental monitoring records, sanitation logs, production data, equipment history, employee interviews, and supplier records where relevant. Involving personnel from quality assurance, sanitation, production, maintenance, and supplier management helps reveal relationships that may be missed by a single department.
  3. Test competing explanations. Use process mapping, cause-and-effect diagrams, structured questioning, and risk assessment to examine plausible causes. Distinguish confirmed causes from hypotheses that still require evidence.
  4. Design actions around the identified mechanism. Corrective measures may involve equipment redesign, improved sanitation access, changes to process controls, supplier interventions, revised procedures, or clearer responsibilities. Retraining should be used where a demonstrated knowledge or competency gap exists, rather than as an automatic response to every deviation.
  5. Define effectiveness criteria before closing the investigation. Establish what evidence will demonstrate that the problem has been addressed. Depending on the hazard, verification may involve targeted environmental sampling, process-record reviews across several production cycles, inspection of modified equipment, or reassessment of supplier controls.
  6. Reopen the investigation when evidence warrants it. A related finding, repeated deviation, or failure to meet the agreed verification criteria should trigger reassessment. Closure should follow demonstrated effectiveness, not simply completion of the assigned tasks.²

Table 1. Translating Recurring Findings Into Preventive Action


Recurring finding Why the immediate response may be insufficient More effective investigation
Repeated environmental pathogen detection Recleaning may leave a persistent source or contamination route unresolved Examine equipment design, moisture, sanitation access, traffic patterns, and related locations
Repeated process deviations Retraining may not address equipment limitations or unrealistic procedures Review process parameters, operating conditions, competency, supervision, and workload
Recurring ingredient-related failures Retesting a new delivery does not establish that supplier controls are reliable Review supplier performance, traceability, incoming verification, and corrective-action evidence
Similar audit findings across shifts Reminders may not resolve inconsistent working conditions Compare actual practices, staffing, resources, procedure usability, and supervisory expectations


As Table 1 shows, the response should target the conditions that enable a problem rather than repeat the same immediate correction.

Food Safety Culture and Organizational Accountability

Recurring incidents cannot always be resolved through technical controls alone. Employees must understand why procedures matter, recognize conditions requiring escalation, and be able to report concerns without pressure to prioritize production targets over food safety.

A deviation may appear to be a training issue when the underlying problem is a procedure that is difficult to follow, insufficient time for sanitation, inadequate equipment access, unclear responsibility, or inconsistent management expectations.

The FDA identifies food safety culture as a core element of its New Era of Smarter Food Safety blueprint. The agency emphasizes the beliefs, attitudes, behaviors, and organizational actions that support effective food safety management.⁵

Manufacturers can translate this principle into daily operations by ensuring that:

  • Employees can report hazards and deviations without fear of retaliation.
  • Supervisors reinforce safe practices during routine production, not only before audits.
  • Procedures reflect actual operating conditions and are supported by appropriate equipment and resources.
  • Quality, production, sanitation, maintenance, and procurement teams understand their responsibilities.
  • Lessons from investigations are communicated to teams working with similar processes or hazards.

Accountability should extend beyond the quality department. Quality teams may lead an investigation, but other functions often control the conditions that allowed the incident to occur. Management must ensure that assigned actions receive the resources and authority needed for implementation.

Using Food Safety Data More Effectively

Digital records, laboratory information systems, environmental monitoring databases, and production management platforms can help organizations identify recurring patterns. Their value depends on whether the information can be compared and interpreted across functions.

For example, repeated findings may become easier to investigate when an environmental sample is linked to the relevant production schedule, cleaning record, equipment maintenance history, and previous results from nearby sampling locations.

Manufacturers should prioritize a few practical capabilities:

  • Consistent records: Use comparable incident categories, location identifiers, dates, and equipment references to make similar events easier to identify.
  • Trend analysis: Review recurrence by hazard, location, process, shift, supplier, and corrective-action type where the data supports those comparisons.
  • Escalation rules: Define when repeated or higher-risk findings require broader investigation or management review.
  • Integrated review: Bring together laboratory, sanitation, maintenance, production, and complaint information where relevant to the incident.
  • Documented verification: Record what changed, how the action was assessed, and whether the evidence supports closure.

Advanced analytics may help flag unusual patterns, but they cannot independently establish a root cause. Data quality, domain knowledge, and effective follow-up remain essential.

Testing Investment Does Not Guarantee Better Outcomes

Demand for food pathogen testing is one indicator of attention to food safety controls.  Vyansa Intelligence forecast for Saudi Arabia’s food pathogen testing sector estimates that the sector will grow from USD 61.77 million in 2025 to USD 126.37 million by 2032, representing a projected compound annual growth rate of 10.77% for 2026–2032.⁶ 

These figures describe projected industry value, not a reduction in foodborne illness or proof that testing investment has improved prevention. The distinction matters because a larger testing program can generate more information without necessarily improving the decisions made from it.

Manufacturers should assess testing by its contribution to risk control: whether results prompt appropriate investigation, whether corrective actions address the identified risks, and whether follow-up evidence demonstrates that the controls work.

Technology and testing are most effective when integrated into a broader preventive system that includes sound process design, sanitation, supplier controls, employee competence, and management oversight.

Measuring Whether Recurrence Is Declining

Audit completion rates, testing volumes, training records, and corrective-action closure times can reveal whether activities are being performed. They do not necessarily establish whether food safety risks are being reduced.

A more informative assessment also tracks repeated findings, effectiveness-verification results, overdue high-risk actions, and incidents that recur after closure. These measures should be interpreted according to the facility’s hazards and operating context; no single metric demonstrates that every risk has been controlled.

The central question is whether the organization has changed the conditions that contributed to the incident and gathered sufficient evidence to support that conclusion.

Food manufacturers cannot guarantee that every hazard will be identified before it causes harm. They can, however, make recurring failures less likely by investigating beyond the immediate symptom, connecting evidence across functions, assigning meaningful corrective actions, and verifying that those actions remain effective under routine production conditions.

An investigation is complete not when its paperwork is closed, but when the organization has established what must change, implemented the change, and assessed whether it works.

References

  1. U.S. Food and Drug Administration. “FSMA Final Rule for Preventive Controls for Human Food.” FDA, Food Safety Modernization Act. https://www.fda.gov/food/food-safety-modernization-act-fsma/fsma-final-rule-preventive-controls-human-food. Accessed October 12, 2026.
  2. U.S. Food and Drug Administration. “Strengthening Food Safety Through Root Cause Analysis.” FDA, Outbreaks of Foodborne Illness. https://www.fda.gov/food/outbreaks-foodborne-illness/strengthening-food-safety-through-root-cause-analysis. Accessed October 12, 2026.
  3. U.S. Food and Drug Administration. “Environmental Sampling.” FDA, Sampling to Protect the Food Supply. https://www.fda.gov/food/sampling-protect-food-supply/environmental-sampling. Accessed October 12, 2026.
  4. U.S. Food and Drug Administration. “CORE+EP 2025 Annual Report: Investigations of Foodborne Outbreaks and Adverse Events in FDA-Regulated Foods.” FDA, 2026. https://www.fda.gov/food/outbreaks-foodborne-illness/coreep-2025-annual-report. Accessed October 12, 2026.
  5. U.S. Food and Drug Administration. “Food Safety Culture—Core Element 4 of the New Era of Smarter Food Safety Blueprint.” FDA, New Era of Smarter Food Safety. https://www.fda.gov/food/new-era-smarter-food-safety/food-safety-culture-core-element-4-new-era-smarter-food-safety-blueprint. Accessed October 12, 2026.
  6. Vyansa Intelligence. “Saudi Arabia Food Pathogen Testing Market Insights 2032.” Industry Report, report code VI1468. https://www.vyansaintelligence.com/industry-report/saudi-arabia-food-pathogen-testing-market-size. Accessed October 12, 2026.
Accreditation

FDA Recognizes JANAAC as an Accreditation Body Under FSMA

By Food Safety Tech Staff
No Comments
Accreditation

The U.S. Food and Drug Administration (FDA) has recognized Jamaica National Agency for Accreditation (JANAAC), as an accreditation body under the Accredited Third-Party Certification Program for a period of five years.

Accreditation bodies recognized by FDA have the authority to accredit third-party certification bodies. These certification bodies, once accredited, can conduct food safety audits and issue certifications of foreign food facilities (including farms) and the foods—both human and animal—that they produce. Those certifications are required to be used by importers to establish eligibility for participation in the Voluntary Qualified Importer Program. In addition, those certifications may be used in certain circumstances where the FDA can require that imported products be certified before entering the United States.

JANAAC is being recognized as having the authority to accredit certification bodies with the ability to conduct food safety audits under the following scopes of accreditation:

  • Acidified Foods (AF)
  • Dietary Supplements
  • Juice Hazard Analysis and Critical Control Points (Juice HACCP)
  • Low-Acid Canned Foods (LACF)
  • Medicated Feed Current Good Manufacturing Practices (Medicated Feed CGMPs)
  • Preventive Controls for Animal Food (PCAF)
  • Preventive Controls for Human Food (PCHF)
  • Produce Safety
  • Seafood Hazard Analysis and Critical Control Points (Seafood HACCP)
  • Shell Eggs

For more information on the eligibility criteria for recognition, see Key Facts about the Accredited Third-Party Certification Program.

Megan Coy-Moran, AIB

Be Confident in Your PCQI’s Training

By Megan Coy Moran
No Comments
Megan Coy-Moran, AIB

With allergens being the leading cause of recalls in the U.S., accounting for approximately 47 percent of recalls as of the most recent FDA reportable food registry annual report, FDA has placed “an emphasis on preventing allergen contamination, protecting consumers, and reducing the need for food recalls.” So, when FDA makes allergen control a priority, how can you be confident that it is a priority for your team and in your facility? By providing your designated Preventive Controls Qualified Individual (PCQI) with the right PCQI training.

Introduced in the Preventative Controls for Human Food Regulation final rule that exists within the FDA’s Food Safety Modernization Act (FSMA), a PCQI is required to be on staff in all food and beverage facilities registered under section 415 of the Federal Food, Drug, and Cosmetic Act (FD&C) Act. In this role, the PCQI oversees development of the Food Safety Plan, hazard analysis, preventive controls, verification activities, and validation of process preventive controls. Further, FSMA mandates that all food manufacturing facilities conduct Hazard analysis and risk-based preventive controls (HARPC), while also implementing science-based preventive control measures to reduce the potential risk of food product adulteration. Each of these are managed by the PCQI and critical to achieving food safety.

With the goal of preventing foodborne illness and maintaining compliance with the FDA, the PCQI also needs to possess an in-depth knowledge of the facility’s Environmental Monitoring Program, food allergen controls, sanitation controls, supply chain controls, and recall plan. The importance of the PCQI’s many responsibilities means they need to have the necessary training and skills for the creation, application, and verification of these and other measures as applicable to their facility.

The PCQI’s oversight and familiarity with the Food Safety Plan also suggests they are likely the primary contact when FDA arrives at your facility for an inspection. Their ability to answer the inspector’s questions and successfully manage this process helps ensure that those visits are as concise and positive as possible. Having this single point of contact is also beneficial for the inspector, as they know they can count on the PCQI as a resource to provide them with necessary information without having to chase down multiple sources. Too, having a PCQI on site makes it easier to then implement regulatory requirements and any necessary preventive controls within the designated time, as they are already familiar with the facility and team.

The best PCQI training will prompt participants to think through real-world scenarios, preparing them to identify best practices to achieve food safety. By then putting this theory into practice in their facilities, they will help ensure compliance. Further, it is important that any course they take features consistently updated information, so you can be assured that what they are being trained on is current and accurate. For instance, when the U.S. Congress passed and President Biden signed the FASTER Act into law in April 2021, including sesame as an allergen of concern, this was an important update. As new information becomes available, their training should remain timely and accurate, ensuring that the experience is relevant and responsive to changing regulations.

Because production right now is priority and many teams are short-staffed, it can be difficult for some to find the time to travel to participate in an in-person training course. This makes online training appealing, as it can be completed when time becomes available, while also saving on travel costs.

With the right training, your PCQI will be an invaluable member of your team. By aligning priorities with regulators and prioritizing food safety throughout their responsibilities, they will improve your facility’s ability to produce safe food.

With our PCQI Online training, your PCQI will be an invaluable member of your team. By aligning priorities with regulators and prioritizing food safety throughout their responsibilities, they will improve your facility’s ability to produce safe food.

Kathryn Birmingham, ImEpik

Ask the Expert: ImEPIK Discusses Supply Chain Controls and PCQI Responsibilities Under FSMA

Kathryn Birmingham, ImEpik

Dr. Kathryn Birmingham, one of ImEPIK’s PCQI training experts, provides guidance to Juan, a future PCQI in a plant that receives ingredients for ready-to-eat energy bars.

Juan: I’m new on the food safety team at a small company and the next person to be trained as a PCQI. Our team wants to make sure we are meeting the requirements in our food safety plan under the Preventive Controls for Human Food Rule in FSMA. There are a lot of players along our ingredients supply chain. Who is ultimately responsible for product safety?

Kathryn Birmingham: As you know Juan, if you manufacture, process, hold or pack an ingredient or food product, food safety is your responsibility. For all of the players along the supply chain FSMA focuses on risk assessment and identifying hazards and preventive controls when required. Your team must have a plan and implement verification activities for the supply chain preventive controls for the food ingredients with hazards you have identified needing a control.

Juan: So, we are sourcing chocolate from a number of suppliers or our bars. They all provide COAs with the shipment that tell us the chocolate is manufactured to be free of pathogens like Salmonella. Usually we get a laboratory report on the sample testing for vegetative pathogens from the supplier for each shipment. We put that in our food safety plan to verify that the hazard was controlled by the supplier. But one of the suppliers has not provided sample testing results we requested. We have finished product to get out the door, but we have to ensure our product doesn’t harm consumers. On top of that, we can’t risk a costly product recall.

Kathryn: Right, Juan. That Certificate of Analysis may not be enough to verify that your chocolate supplier is effectively controlling for the hazard of Salmonella. For your product process flow the chocolate will never have a kill step to mitigate the hazard. If you cannot be sure that the hazard has been significantly minimized or prevented before receipt of the chocolate – per section 117.410 in the PCHF Rule – you have some choices to make. If you are using a foreign supplier there are considerations if the supplier is or is not in compliance with the FDA’s Foreign Supplier Verification Program.

Juan: So it looks like we may have to take on the cost and additional time of sample testing?

Kathryn: Remember, supplier approval is based on performance. If your supplier does not give you the evidence for verification you may need to conduct an onsite audit, perform sampling and testing and review other supplier records. You decide if the supplier meets your Supply Chain Control Program or Foreign Supply Chain Control Program.

Juan: My team members need to learn more about what we need to do to comply with FSMA and the PCHF Rule. Tell me about what we can learn through PCQI training.

Kathryn: Preventive Controls Qualified Individuals are trained in a methodical process for decision-making on hazards and preventive controls. The best training fosters a positive food safety culture and includes practice on team scenarios.

A PCQI must be able to identify hazards associated with a product and process, determine the appropriate preventive controls and develop associated monitoring and corrective actions for hazards that are identified. PCQIs must also establish and implement appropriate verification activities for the application of preventive controls. All of that is included in the food safety plan they oversee.

Juan: What choices do we have for online PCQI training?

Kathryn: First choose your food safety team members. If your company is registering with the FDA you are required to have at least one PCQI at each facility. Most companies train multiple or back up employees for the PCQI role to ensure they are covered during vacations, sick time, various shifts or employee turnover.

Look for courses that include the FDA’s standard curriculum, like ImEPIK’s PCQI Online. The PCHF Rule does not require that PCQIs hold a specific training certificate, but FDA inspectors want to see that the PCQI has been successful in a training with the requisite learning objectives and content. There are many PCQI training options on the market. Some providers claim that their training is the only accepted training – that’s simply not true.

Look for courses that have a multiple of scenarios with different food products and challenge situations for practice and wider breadth of learning.

ImEPIK’s PCQI Course is interactive and 100% online. The ten-module training is entirely self-paced thus does not require travel or scheduling on-line webinars or sessions. You simply log in, work through the course as you have time, and earn your completion certificate to document in your food safety plan. If you take a break, the work you have done will be saved, and you pick up where you left off when you return to the course. This allows for reflection and practice in the workplace as you move through the modules.

It’s an ever changing environment for the food safety professional and quality training makes a big difference in keeping up with changes and staying regulatory compliant. Take PCQI Online and position yourself and your facility for food safety success.

About Kathryn Birmingham, Ph.D

Kathryn Birmingham, ImEpikKathryn Birmingham, Ph.D., is Chief Operating Officer of ImEPIK. Birmingham leads the company’s course development teams and ensures that the online training solutions are of high quality. She is certified as a Lead Instructor to teach the FSPCA’s Preventive Controls Qualified Individual course.

Dr. Birmingham taught graduate and doctoral students at the University of Florida and served as Dean of Arts and Sciences at Florida State College. At the latter she lead the Biotechnology Degree program and Institute for Food Safety analytical lab. She was Principal Investigator (PI) for its National Science Foundation studies.

Content Sponsored by ImEPIK.

Chris Keith, FlexXray
FST Soapbox

How Foreign Material Inspection Can Impact Your Liability From Packaging

By Chris Keith
No Comments
Chris Keith, FlexXray

Packaging is an essential component of our modern, global food supply. While it helps us preserve and protect food and creates instant brand recognition for consumers, packaging also inserts an additional level of necessary risk mitigation into the manufacturing process. Liability stemming from packaging is a serious concern for food manufacturers of all sizes, with millions of dollars and brand-damaging lawsuits on the line. Processed foods need packaging to arrive in the hands of consumers, and processed foods are necessary to feed the world’s population. According to a survey conducted by the United States National Library of Medicine, “60% of calories consumed were from ultra-processed foods.”1 This shows the prevalence of processed foods and the significant impact packaging, a ubiquitous component of processed foods, plays in the food industry.1 However, if not handled properly, food packaging can be a significant liability.

Liability from packaging commonly presents in two ways: First, as foreign material contamination. Broken, damaged or defective packaging material can end up in food products, which increases the risk of a consumer attempting to consume contaminated goods. Second, packaging can be a hurdle to effective remediation of foreign material contamination, as goods can often not be efficiently or effectively inspected back through in-plant critical control points. The resulting disposal of product can contribute to food and environmental waste, as well as lost profits.

The harsh truth is that if manufacturers lack processes to identify, prevent or mitigate foreign material contamination when it occurs in packaged food, packaging can be a significant liability at every stage from the manufacturing facility to the store shelf. Following strict food safety plans can save countless hours, resources and dollars in the long run.2

Foreign Material Contamination: Where It Comes From

Foreign material contamination comes from multiple sources in the production cycle. It can come from raw materials, like animal bones ending up in boneless meat products. It can happen during the production process when a screw or seal detaches from a machine and gets mixed into a pie. It can be biological, like an insect ending up in a bag of chips. Or it can come from packaging: A shard of glass winding up in a jar of salsa or a plastic wrapper finding itself in a muffin. All of these foreign material contaminants are risks and dangers for which manufacturers can be held liable.

Packaging-related contamination is a high priority for manufacturers. Foreign material contamination due to packaging occurs when contaminants like metal, plastic, styrofoam and other objects end up where they do not belong, disrupting the integrity and quality of the product. Packaging materials can break down into tiny pieces that inline inspection machines may not be able to identify. Inline machines are calibrated for a certain size and certain types of foreign material contamination, which may not include packaging materials. Additionally, inline machines are often used at critical points during the manufacturing process but are not commonly used to inspect completed packaged products.

Break It Down: Liabilities Within Food Packaging

The party most affected by missed foreign material contamination is the consumer. Current consumer trends point to greater ingredient awareness, education and research into the companies from which consumers purchase products. The consumer mindset of environmentally friendly products and socially responsible purchases are impacting the food industry directly. Consumers seek transparency from brands about the products they’re ingesting. When a consumer discovers foreign material contamination inside a product, it creates frustration and eliminates trust. In addition to negatively impacted brand reputation, a foreign object from packaging can be incredibly costly. Recalls, especially those that require a local or national public warning, are detrimental to a brand’s reputation.3 Consumer trust in a brand is priceless and can take years to repair when broken.

In the age of social media, consumer reports of foreign material contamination can spread like wildfire across multiple platforms, reaching countless consumers across the world. One tweet about a contaminated product can go viral, costing corporations their reputations or worse–– lawsuits. An accidental miss somewhere along the production line can result in public outrage and cost the manufacturer millions of dollars in wasted product and crisis management. Suppose a consumer accidentally consumes a foreign contaminant from product packaging which results in injury. In that case, the manufacturer could be held liable for the medical bills and even long-term care if the injury is debilitating. These court cases can be highly costly monetarily and in terms of public perception.

In addition to legal liability from consumers, the loss of product for foreign material contamination is typically very costly when labor, storage, time, materials and lost revenue are taken into account. A producer who makes the moral and ethical decision to dispose of product that may be contaminated loses money doing so. They also risk harming their reputation with consumers by contributing to the problem of food waste.

In the 21st century, shoppers are increasingly looking “beyond the label,” and are concerned with the impact their purchase behaviors have on the environment.4 Consumers in younger demographics are significantly more likely to have a purchase decision influenced by a company’s impact on and concern for the environment. Packaging is a major concern for food manufacturers as they seek to lessen their environmental impact to meet market demands. This impacts foreign material contamination in two important ways. First, as packaging materials move towards the use of biodegradable materials, the capability of technology to detect the difference between packaging and food material must increase. Second, environmentally-friendly packaging is still relatively new compared to traditional materials, and the risks of foreign material contamination associated with these materials are still relatively unknown.

Manufacturers are in a difficult position when dealing with the liabilities stemming from packaging as a foreign material contaminant. Compounding this issue is the role packaging plays in preventing manufacturers from using in-house processes or inline equipment to inspect product back through Critical Control Points. Inline mechanisms for identifying foreign material contamination are not designed to inspect completed, packaged product. If producers dispose of and rework product, they risk harm to sustainability-focused brands, production quotas and bottom lines. If they attempt to identify the contamination themselves, they lose valuable production time and potentially lose perishable product to spoilage. With nearly every solution, another liability arises.

Packaging Contaminants: Prevention, Response and Liability

The FDA-required Hazard Analysis and Critical Control Points (HACCP) plan has seven principles to ensure manufacturers meet food safety goals from production to consumption. Physical, chemical and visual tests are involved to ensure foreign contaminants do not exist in products produced in the manufacturing facilities.5 The more detailed processes are in place, the more protected companies are from recalls and reducing the chance of a lawsuit where the manufacturer is liable. Implementing different programs and processes to prevent and diminish food waste ultimately positively impacts the manufacturer’s bottom line. The Business Case conducted a study called “Reducing Food Loss, and Waste” that found “99% of companies earned a positive investment when they implemented programs to reduce food waste”.6

Many companies engage third-party food inspection partners as an extra measure to ensure that their product is free from foreign material contamination. By electing to utilize third-party inspection services, manufacturers hit a trifecta: They can typically salvage the majority of on-hold product, reduce food waste, and with the right partner, get the data they need to have traceability of foreign material contamination issues at their plant.

Manufacturers should pursue third-party inspection partners that meet a high standard of excellence. The best third-party inspection partners use cutting-edge technology to inspect products in higher detail than inline machines. Their machines should be capable of identifying foreign material contaminants of all types and have a high capacity to turn around large volumes of product efficiently. Their machines should be capable of overcoming the obstacle of packaging as an impediment to inspection using machines with a larger aperture than typical inline tools. Lastly, third-party inspection adds significant value if it has the ability to find and retrieve foreign material contamination so manufacturers can effectively use the resulting data to identify and remediate problems within the plant. An inspection service that does not meet these criteria is not an inspection service, but merely a method for outsourcing the same practices that a manufacturer would conduct in-house.

Liability Questions Answered

So, when are companies liable for packaging issues? Unfortunately, the answer isn’t always black and white. FSMA is in place to help prevent foodborne illness, requiring Food Safety Plans. In addition, the FDA recognizes “that ensuring the safety of the food supply is a shared responsibility among many different points in the global supply chain for both human and animal food,” so manufacturers may not be the only ones liable in many cases.7 The problem arises when manufacturers miss foreign contaminants or if foreign biological contaminants affect the integrity of the packaging.

Even if companies take the necessary steps, incorporate a HACCP plan and are vigilant, contamination can, unfortunately, happen at any time to any manufacturer. Using a third-party partner as an outside resource for foreign material inspection is important. Choosing a third-party partner with the experience, certifications, technology, processes and reputation to protect your brand is critical. Manufacturers can validate their internal processes and data using reports from their third-party inspection partner more quickly than they could internally.

Food packaging and the potential liability involved can be daunting. Still, with proper processes and procedures in place, manufacturers can have confidence that their products are hitting the shelves with a low probability of recall or lawsuit due to a packaging issue. While there is always a chance of foreign material contamination, quality packaging materials, quality assurance processes and quality third-party inspection partners can significantly reduce a company’s potential liability.

References

  1. Baraldi, L. G. (March 9, 2018). “Consumption of ultra-processed foods and associated sociodemographic factors in the USA between 2007 and 2012: evidence from a nationally representative cross-sectional study.” BMJ Open.
  2. FDA. “FSMA Final Rule For Preventive Controls For Human Food”.
  3. Lusk, J. (October 15, 2019). “Consumer Beliefs About Healthy Foods And Diets.”
  4. Cheung, K. H. J. L. (2020). “Meet the 2020 Consumers Driving Change“. IBM.
  5. FDA(August 14, 1997). “HACCP Principles & Application Guidelines.”
  6. Hansen, C. “The Business Case For Reducing Food Loss and Waste.” Champions 12.3.
  7. FDA. “Food Safety Modernization Act (FSMA).”
FDA

FDA Issues Letter to Industry Addressing Efforts to Reduce Chemical Hazards in Foods for Babies and Young Children

By Food Safety Tech Staff
No Comments
FDA

A report released last month by the Subcommittee on Economic and Consumer Policy revealed dangerous levels of toxic heavy metals in baby food. It stirred up quite a bit of controversy and concern, and raised questions over whether baby food manufacturers were hiding dangerous levels of toxic heavy metals in food, and whether FDA was doing enough to ensure the safety of food.

In an effort to assure the public that FDA is taking the issue seriously, the agency published a constituent update about its actions to further prevent or reduce toxic elements in foods for babies and young children. It also issued a letter to manufacturers and processors of baby and toddler foods as a reminder of the “responsibility under the rulemaking to consider chemical hazards that may be present in foods when conducting your hazard analysis,” which is part of the preventive control provisions of the Current Good Manufacturing Practice, Hazard Analysis, and Risk-based Preventive Controls for Human Food FSMA rule.

“FDA takes exposure to toxic elements in the food supply extremely seriously, especially when it comes to protecting the health and safety of the youngest and most vulnerable in the population. Toxic elements, such as arsenic and lead, are present in the environment and may enter the food supply through soil, water, or air,” stated CFSAN Director Susan Mayne in the letter. “Our goal is to reduce exposure to toxic elements in foods to the greatest extent feasible and to further advance progress in this area through more research and enhanced collaboration among stakeholders.”

The agency also stated that it is finalizing a plan to reduce levels of toxic elements in baby foods, including:

  • “Reviewing current action levels, as well as developing additional action levels, to help make food safer, including finalizing the arsenic in apple juice draft guidance and publishing a draft guidance with action levels for lead in juices.

  • Focused compliance and enforcement activities, including inspections.

  • Providing guidance to industry on how to meet their obligations under current regulations.”

The agency will also continue its surveillance sampling assignment that focuses on these products.

Frank Yiannas, FDA, food safety

Ten Years Later, a Reflection on FSMA’s Accomplishments

Frank Yiannas, FDA, food safety

It may be hard to believe that 10 years have passed since FSMA became law. The risk-based preventive approach to growing, manufacturing and processing, packing, storing and transporting food has transformed the industry and the nation’s food system. Today, on the anniversary of FSMA, FDA Deputy Commissioner for Food Policy and Response Frank Yiannas takes a look at where it all began and walks us through progress, accomplishments and what the future holds.

  • Seven foundational rules established, and the proposed Food Traceability Rule (September 2020) positioned to harmonized traceability
  • Global partnerships (Canada, Mexico, Europe, and China) to strengthen safety of imported food
  • Investment in cooperative agreement programs to support compliance with FSMA rules at the state level
  • Looking forward: New Era of Smarter Food Safety, with blueprint released in July 2020 creates a 10-year roadmap for a more “digital, traceable and safer food system”
    • Incentivizing industry to adopt new technologies that facilitate full traceability
    • Emphasis on food safety culture on farms and in food facilities
    • Improving root cause analysis when preventive control measures fail

“Have we accomplished everything we wanted to help ensure that the food you serve your family is safe? The honest answer is that we’re still working on that. We are working diligently to ensure that remaining FSMA rules and related guidance documents are finalized and implemented,” said Yiannas in the FDA Voices blog. “But even when we have reached all of those milestones, we will always be working with industry on continuous improvement based on the latest science and the application of new technologies. Every day we will do our utmost to make our nation’s food as safe as it can be.”

Manuel Orozco, AIB International
FST Soapbox

Detecting Foreign Material Will Protect Your Customers and Brand

By Manuel Orozco
No Comments
Manuel Orozco, AIB International

During the production process, physical hazards can contaminate food products, making them unfit for human consumption. According to the USDA’s Food Safety and Inspection Service (FSIS), the leading cause of food recalls is foreign material contamination. This includes 20 of the top 50, and three of the top five, largest food recalls issued in 2019.

As methods for detecting foreign materials in food have improved over time, you might think that associated recalls should be declining. To the contrary, USDA FSIS and FDA recalls due to foreign material seem to be increasing. During the entire calendar year of 2018, 28 of the 382 food recalls (7.3%) in the USDA’s recall case archive were for foreign material contamination. Through 2019, this figure increased to approximately 50 of the 337 food recalls (14.8%). Each of these recalls may have had a significant negative impact on those brands and their customers, which makes foreign material detection a crucial component of any food safety system.

The FDA notes, “hard or sharp foreign materials found in food may cause traumatic injury, including laceration and perforation of tissues of the mouth, tongue, throat, stomach and intestine, as well as damage to the teeth and gums”. Metal, plastic and glass are by far the most common types of foreign materials. There are many ways foreign materials can be introduced into a product, including raw materials, employee error, maintenance and cleaning procedures, and equipment malfunction or breakage during the manufacturing and packaging processes.

The increasing use of automation and machinery to perform tasks that were once done by hand are likely driving increases in foreign matter contamination. In addition, improved manufacturer capabilities to detect particles in food could be triggering these recalls, as most of the recalls have been voluntary by the manufacturer.

To prevent foreign material recalls, it is key to first prevent foreign materials in food production facilities. A proper food safety/ HACCP plan should be introduced to prevent these contaminants from ending up in the finished food product through prevention, detection and investigation.
Food manufacturers also have a variety of options when it comes to the detection of foreign objects from entering food on production lines. In addition to metal detectors, x-ray systems, optical sorting and camera-based systems, novel methods such as infrared multi-wavelength imaging and nuclear magnetic resonance are in development to resolve the problem of detection of similar foreign materials in a complex background. Such systems are commonly identified as CCPs (Critical Control Points)/preventive controls within our food safety plans.

But what factors should you focus on when deciding between different inspection systems? Product type, flow characteristics, particle size, density and blended components are important factors in foreign material detection. Typically, food manufacturers use metal and/or x-ray inspection for foreign material detection in food production as their CCP/preventive control. While both technologies are commonly used, there are reasons why x-ray inspection is becoming more popular. Foreign objects can vary in size and material, so a detection method like an x-ray that is based on density often provides the best performance.

Regardless of which detection system you choose, keep in mind that FSMA gives FDA the power to scientifically evaluate food safety programs and preventive controls implemented in a food production facility, so validation and verification are crucial elements of any detection system.

It is also important to remember that a key element of any validation system is the equipment validation process. This process ensures that your equipment operates properly and is appropriate for its intended use. This process consists of three steps: Installation qualification, operational qualification and performance qualification.

Installation qualification is the first step of the equipment validation process, designed to ensure that the instrument is properly installed, in a suitable environment free from interference. This process takes into consideration the necessary electrical requirements such as voltage and frequency ratings, as well as other factors related with the environment, such as temperature and humidity. These requirements are generally established by the manufacturer and can be found within the installation manual.

The second step is operational qualification. This ensures that the equipment will operate according to its technical specification. In order to achieve this, the general functions of the equipment must be tested within the specified range limits. Therefore, this step focuses on the overall functionality of the instrument.

The third and last step is the performance qualification, which is focused on providing documented evidence through specific tests that the instrument will performs according to the routine specifications. These requirements could be established by internal and industry standards.

Following these three steps will allow you to provide documented evidence that the equipment will perform adequately within the work environment and for the intended process. After completion of the equipment validation process, monitoring and verification procedures must be established to guarantee the correct operation of the instrument, as well procedures to address deviations and recordkeeping. This will help you effectively control the hazards identified within our operation.

There can be massive consequences if products contaminated with foreign material are purchased and consumed by the public. That’s why the development and implementation of a strong food safety/ HACCP plan, coupled with the selection and validation of your detection equipment, are so important. These steps are each key elements in protecting your customers and your brand.

Alex Kinne, Thermo Fisher Scientific
In the Food Lab

Ensuring Food Safety in Meat Processing Through Foreign Object Detection

By Alex Kinne
No Comments
Alex Kinne, Thermo Fisher Scientific

The USDA estimates that foodborne illnesses cost more than $15.6 billion each year. However, biological contamination isn’t the only risk to the safety and quality of food. Food safety can also be compromised by foreign objects at virtually any stage in the production process, from contaminants in raw materials to metal shavings from the wear of equipment on the line, and even from human error. While the risk of foreign object contamination may seem easy to avoid, in 2019 alone the USDA reported 34 food recalls, impacting 17 million pounds of food due to ‘extraneous material’ which can include metal, plastic and even glass.

When FSMA went into effect, the focus shifted to preventing food safety problems, necessitating that food processors implement preventive controls to shift the focus from recovery and quarantine to proactive risk mitigation. Food producers developed Hazard Analysis and Critical Control Point (HACCP) plans focused on identifying potential areas of risk and placement of appropriate inspection equipment at these key locations within the processing line.

Metal detection is the most common detection technology used to find ferrous, non-ferrous, and stainless steel foreign objects in food. In order to increase levels of food safety and better protect brand reputation, food processors need detection technologies that can find increasingly smaller metal foreign objects. Leading retailers are echoing that need and more often stipulate specific detection performance in their codes of practice, which processors must meet in order to sell them product.

As food processors face increased consumer demand and continued price-per-unit pressures, they must meet the challenges of greater throughput demands while concurrently driving out waste to ensure maximum operational efficiencies.

Challenges Inherent in Meat Metal Detection

While some food products are easier to inspect, such as dry, inert products like pasta or grains, metal foreign object detection in meat is particularly challenging. This is due to the high moisture and salt content common in ready-to-eat, frozen and processed, often spicy, meat products that have high “product effect.” Bloody whole muscle cuts can also create high product effect.

The conductive properties of meat can mimic a foreign object and cause metal detectors to incorrectly signal the presence of a physical contaminant even when it is nonexistent. Food metal detectors must be intelligent enough to ignore these signals and recognize them as product effect to avoid false rejection. Otherwise, they can signal metal when it is not present, thus rejecting good product and thereby increasing costs through scrap or re-work.

Equipping for Success

When evaluating metal detection technologies, food processors should request a product test, which allows the processor to see how various options perform for their application. The gold standard is for the food processor to send in samples of their product and provide information about the processing environment so that the companies under consideration can as closely as possible simulate the manufacturing environment. These tests are typically provided at no charge, but care should be taken upfront to fully understand the comprehensiveness of the testing methodologies and reporting.

Among the options to explore are new technologies such as multiscan metal detection, which enables meat processors to achieve a new level of food safety and quality. This technology utilizes five user-adjustable frequencies at once, essentially doing the work of five metal detectors back-to-back in the production line and yielding the highest probability of detecting metal foreign objects in food. When running, multiscan technology allows inspectors to view all the selected frequencies in real time and pull up a report of the last 20 rejects to see what caused them, allowing them to quickly make appropriate adjustments to the production line.

Such innovations are designed for ease of use and to meet even the most rigorous retailer codes of practice. Brands, their retail and wholesale customers, and consumers all benefit from carefully considered, application-specific, food safety inspection.

Ensuring Safety

The food processing industry is necessarily highly regulated. Implementing the right food safety program needs to be a top priority to ensure consumer safety and brand protection. Innovative new approaches address these safety concerns for regulatory requirements and at the same time are designed to support increased productivity and operational efficiency.

Ben Schreiber, ActiveSense
Bug Bytes

How ERM Can Simplify Pest Management

By Benjamin Schreiber
2 Comments
Ben Schreiber, ActiveSense

Whether you work in food manufacturing, distribution or retail, pests are both a fact of life as well as a regulatory disruption. At the same time, pest management solutions aren’t always clear-cut: While there are a variety of effective strategies employed by pest management professionals (PMPs) servicing the food industry, industry challenges—shifting regulatory standards, a lack of proper documentation and more—can complicate the process. For these reasons, short-term rodent problems can become long-term logistical nightmares, leaving food manufacturers in an undesirable situation when a third-party food plant auditor arrives.

Fortunately, emerging technologies in pest management practices are helping facility managers streamline their food and beverage quality assurance processes, reducing the risk of product loss, regulatory action, improper brand management and more. Specifically, electronic remote monitoring (ERM) allows PMPs to detect and monitor rodents in real time, providing you with important information to help reduce risk and increase audit compliance. As such, the value of food safety pest management strategies that incorporate ERM systems is only growing. Seeking out PMPs who use ERM allows you to invest in technologies that protect your margins, ensure the quality of your product and, ultimately, safeguard your most important asset—your reputation.

Modernizing Pest Management With ERM

At first glance, it might seem like pest management practices haven’t drastically changed since they were first implemented in the food manufacturing industry. Many rodent trapping systems remain similar to their original design: Devices designed to trap or kill that must be individually inspected and serviced by professional technicians. Technicians must then relay any risks to facility managers, who have to determine if additional resources are needed to avoid product loss or audit-based infractions.

Upon closer examination, it’s clear that while pests themselves have not significantly changed, both the pest management industry and the modern food supply chain have become increasingly complex. Food facility managers must contend with increasingly stringent food safety standards, and PMPs must rise to meet these needs with evolving pest management strategies.

In many ways, ERM technologies are the structural pest control industry’s response to these challenges, providing technicians with real-time notifications about rodent behavior and allowing them to make risk-based assessments that identify and treat problems before infestations occur. Unlike pest control strategies that rely on periodic service visits from technicians, PMPs who utilize ERM technology can monitor pest activity around the clock, 24/7/365, in virtually any environment. Instead of monitoring individual traps, PMPs can use ERM technology to know exactly when and where pest activity occurs, including in hard-to-monitor areas such as drop ceilings, crawlspaces, shelving undersides and other traditionally overlooked spaces. Technicians then receive valuable analytics from each trap they install, as well as documentation and reporting, that help managers achieve audit and regulatory compliance.

FSMA and ERM

In 2015, the FDA issued the final component of preventative control for human food under FSMA, officially enacting legislation that requires food safety plants to focus on risk-based pest prevention instead of reactive pest control strategies. As a result, quality assurance professionals and facility managers are often tasked with reallocating personnel toward proactive pest control activities in addition to their day-to-day responsibilities.

In many ways, ERM systems go hand-in-hand with FSMA and GFSI regulations. While preparing for a situation that hasn’t yet occurred can be a costly and time-consuming process, ERM has helped PMPs develop custom pest management strategies that assess and control situations in accordance with FSMA and other auditing firm guidelines. In many ways, ERM can provide all parties—PMPs, in-house auditors and third-party regulators—with a track record of pest history that all parties can cross-reference when assessing a facility.

From Risk-Averse to Risk-Based

When it comes to food safety rules and regulations, the only constant is change. In the structural pest control industry, auditors have historically implemented strict guidelines about trap placement that are frequently changing: For instance, traps should be placed every 10, 15, or 20 feet, regardless of facility susceptibility to various pest conditions. Failure to comply with regulations can result in point deductions on audits, even if the conditions that might lead to an infestation are not present. As such, food processing plants often choose to abide by the most stringent audit guidelines imposed upon them by other parties, such as retailers. By utilizing ERM technologies, food safety and quality assurance professionals can use additional pest monitoring analytics to focus on specific compliance issues, rather than spending additional time and money on other strategies.

Additionally, ERM allows PMPs to focus their efforts not only on weekly service visits and station checks, but also on important tasks, including assessing facility vulnerabilities, tracking rodent access points, and providing consultation and additional management strategies to their client—you.

Approaching the Audit with ERM

Food plant managers and retailers alike know that auditor approval is everything. Because ERM is a fast-developing technology, many quality assurance managers and facility owners are curious to know if ERM is audit approved. In truth, there are many kinds of audits, each with different goals, assessment techniques and regulatory standards. When it comes to audits, the gold standard is not necessarily the assessment of the facility and production line itself, but rather how well the assessment matches records kept by the food production plant.

To this end, ERM might be the answer to a streamlined audit process. No matter what kind of audit a plant is currently undergoing, ERM allows PMPs to provide records auditors need to verify that all systems are working properly. ERM can mean the difference between a streamlined process and a laborious audit, acting as a documentation system that helps officials conduct a PMP-verified “second-check.” This kind of verification is invaluable in an industry where there are already more than enough regulatory categories to consider without having to further worry about potential pest infestations.

ERM-Oriented Solutions

Thanks to the many advantages they offer, ERM and other remote pest monitoring technologies are growing in popularity. Many facility managers appreciate that ERM allows them to assess pest activity, prevent infestations before they occur, gather data that helps them remain industry-compliant, and acquire and share information with additional parties. If you’re a facility manager, quality assurance professional or other food safety decision-maker interested in the opportunities ERM technologies provide, consider starting the conversation about your pest prevention system with your PMP and how ERM might help improve it.

Trust, But Verify

There is an overwhelming consensus in the pest control industry that technology should be developed to provide end-users with more information. ERM systems are a natural extension of this belief, providing each component of the food production and distribution supply chain—manufacturers, distributors, retailers, quality assurance officials, technicians and others—with more data about how pest control decisions are made. Without data, it can be difficult to ensure technician service visits end in greater transparency about the issues facility owners will face as they prepare for an audit.

Fortunately, ERM can help provide the level of trust and assurance plant managers need to feel confident in their day-to-day operations. ERM is an important step forward for manufacturer-regulator relations, which require a strong combination of data, trust and transparency to ensure that communication systems don’t break down. After all, there are many industries in which miscommunication can lead to catastrophic consequences, and food production is no exception.

While each manufacturing facility, processing plant, distribution center, storage warehouse and retail outlet is different, none are insusceptible to pest infestations, and none can avoid audits required to keep them compliant. Because rigorous oversight is crucial for food producers and consumers alike, working with your PMP to develop pest monitoring strategies that utilize ERM systems and other cutting-edge technologies should be part of your larger pest control consideration process.

In the end, the pest infestation that causes the least damage to your product, profit potential and industry reputation is the infestation that never occurs.