Top 20 Tips for Tubing and Hose Selection

By John Stover
4 Comments
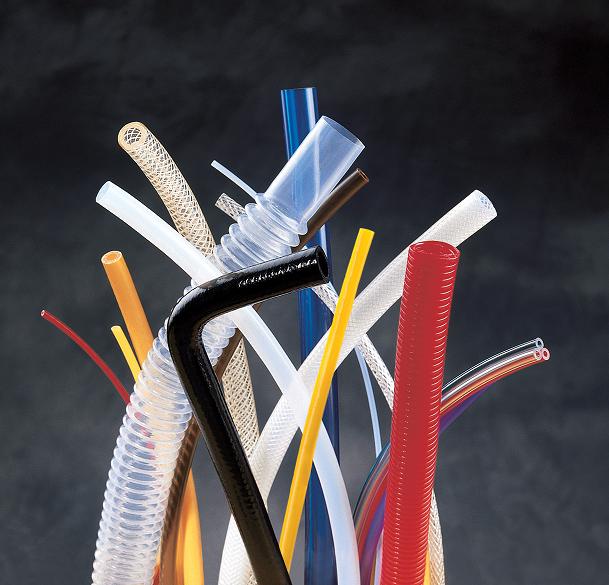
It can be challenging to make sure that you have covered all the bases during the tubing and hose selection process. Have you considered all the elements involved with the application? Temperatures, chemicals, pressures, flexibility needs? Have you ever ordered hundreds, even thousands, of feet of plastic tubing or reinforced hose and then found it wasn’t the best product for your application? 
 
This article on Top 20 Tubing & Hose Buying Tips can help avoid the downtime, costs, and frustration involved with ordering the wrong tubing or hose. The tips highlight details that can be overlooked, present questions to ask your supplier, and suggest research you can do to help avoid buying errors.
In this first part, we present Tips 1 through 10; check back next week for tips 11 through 20. 
 
1. Check for ingredient approvals
You may need to know if the tubing or hose under consideration is manufactured with FDA (Food and Drug Administration), NSF (National Sanitation Foundation), USP Class VI (United States Pharmacopoeia), 3-A (a dairy industry organization), or other association-approved ingredients.
 
If this is the case, check the supplier’s tubing specifications for this information. If you’re unsure whether the application calls for association-approved ingredients, find out from an informed source, such as the end user or product design engineer. Educate yourself about required ingredient approvals to avoid the hassle of buying something you may need to return.
 
2. Be aware of pressure or vacuum requirements
Applications can range from simple drainage lines, well handled by gravity and involving virtually no pressure, to those requiring a robust product able to manage full vacuum (29.9 in/Hg). You’ll need to consider whether your application is one of these extremes or, more likely, one that falls in between. Some unreinforced tubing can deal adequately with low pressure situations; others cannot. It often depends on the tubing material and how hard or soft it is (i.e., polypropylene or latex).
 
Reinforced hose is frequently called for in pressure and vacuum applications. In fact depending on the type of reinforcement (braid, fabric, stainless steel wire, convolutions), certain types of reinforced hose are well suited for pressure applications, while others are better for vacuum. If you’re unsure of your application’s pressure or vacuum needs, you’ll need to ask questions, conduct tests, or find out from an informed source. Research the needs and usage to avoid situations where the tubing or hose ruptures – or even explodes – because it was not the right product for the application. Human injuries can occur depending on the severity of the rupture.
 
3. Know the temperatures involved
Several things need to be investigated when it comes to tubing, hose, and temperatures. Can the tubing or hose being withstand the temperature of the product traveling through it?  Is that product a liquid, gas, dry material, or electrical wiring? Also think about the temperature of the environment it is in. Will the tubing be inside a controlled environment that’s kept at a constant 72°F (22°C)? Will it lay next to other equipment that throws off heat? Will the hose or tubing be outside and subject to both heat and cold, plus variable sunlight? Will it need to operate and remain flexible below freezing? 
 
Remember, the higher the temperature, the less pressure the tubing or hose can handle. Your application may be well served with, for instance, 1/4” silicone tubing conveying water at 200°F and a working pressure of only 20 psi at 70°F. But if the temperature increases to 300°F, your pressure handling capabilities will decrease. Reinforced silicone hose should then be considered.
 
June-2012-NewAge-Industries-34. Consider flexibility and resistance to kinking
Flexibility is a property that varies greatly depending on the type of plastic or rubber material and its construction. Factors that affect flexibility include durometer (softness or hardness), force-to-bend, size, wall thickness, reinforcement style, and temperature. Some plastic tubing and hose, like that made from softer-durometer PVC or polyurethane, is very flexible. Most rubber tubing such as silicone and latex is also flexible. Examples of harder durometer flexible plastic tubing include those made from nylon, fluoropolymers like PTFE, polyethylene, and polypropylene. These are fairly stiff in their common straight tubing styles but are bendable. Customization such as coiling, convoluting, and corrugating can make them more flexible.
 
Some applications call for repeated flexing of the tubing or hose. Situations involving robotics or circumstances where the tubing is repeatedly moved require special consideration. The tubing or hose must be durable enough to withstand such movements. Instances where the tubing comes into contact with other equipment should be examined as well. Many materials offer abrasion resistance and are able to withstand repeated flexing and rubbing.
 
Closely related to flexibility concerns is kink resistance. If your application calls for the tubing or hose to bend around machinery, its resistance to kinking and collapsing upon itself must be considered. Sometimes a very flexible material – silicone, for instance – can address the issue. But if pressure and/or durability requirements will not allow the use of such a soft material, the hose’s construction can come into play. Braid or wire reinforcement can help to reduce the occurrence of kinking, as can products that are multi-layered. Stiff materials can also resist kinking provided that enough length is incorporated into the design.
 
5. Consider weight
The weight of a tube or hose can have a big impact on a final product. You need a product that will help keep overall equipment weight at a minimum but one that can handle the job. Tubing material, size, wall thickness, and reinforcement (if any) affect its heaviness. For example, a typical 100 ft. coil of unreinforced polyurethane tubing, 1″ I.D. x 1-1/4″ O.D., weighs about 21 lbs. A similar size and length of reinforced PVC tubing weighs 35 percent more. 
 
Multi-layered hoses – especially those incorporating metal reinforcement – can be quite heavy. Add metal fittings and clamps to form an assembly, and that increases the weight further. 
 
The overall weight of the tubing, reinforced hose, and/or assembly components used in your application must be examined. You’ll want to make sure you don’t create a situation where a hose assembly’s weight pulls on other components such as fitting connections. If your application involves a bulkhead, you don’t want the assembly putting a strain on the entire system or structure.
 
6. Know if the tubing or hose would impart a taste or odor to the product 
If your application involves foods, beverages or dairy products, any taste or odor transferred to those products could be critical. Some tubing and hose materials contain plasticizers (chemical agents) to facilitate processing and aid in the flexibility of the finished tubing or hose. Under certain circumstances these additives can leach out from the tubing or hose. They can appear in the streams conveyed by the tubing or hose or possibly affect the stream with a taste or odor. That may be fine if the line is used for drainage or a waste product, but if the fluid is part of a finished product that someone will consume, taste and odor transfer is a significant concern.
 
Certain tubing and hose materials (silicone and polyurethane, for instance) are naturally flexible. There are no plasticizers used in their manufacture, so the potential of taste and odor issues that can come from the use of plasticizers is eliminated. In any case, if taste or odor is a concern in your application, you should sample a candidate hose or tubing to test if the material might affect your stream.
 
June-2012-NewAge-Industries-57. Decide if you need to see the products being conveyed within the tubing or hose
Do you need to see the flow of product through the tubing or hose to check for consistency, progression, or to note measurements? Perhaps the nature of the application makes it undesirable to see what’s inside, so an opaque color is called for.
 
Do not assume that because one style of a particular hose material is crystal clear that all hose of that material is the same. The hose’s construction, whether it’s reinforced with wire, braid, or spirals, can greatly affect its clarity. Several tubing products are available in clear styles – PVC, polyurethane, and some fluoropolymers are examples. But when they’re in the form of reinforced hose, their clarity can be compromised. 
 
Many tubing materials can be tinted or colored to varying degrees of clarity. Clear or color-tinted transparent tubing allows light to pass through so that objects within or behind can be easily seen. Some tubing materials (silicone, polypropylene, latex) offer translucency and allow light to pass through but not detailed images. 
 
8. Learn whether the tubing or hose can be sterilized and reused
Plastic tubing is often considered a disposable item, but it doesn’t always have to be. Learning whether the tubing or hose for your application can be cleaned and used again can save you money.
 
Discover whether the tubing or hose can handle one or more standard cleaning methods. Other important information to know is how many cycles, or how many times, it may be cleaned using the same procedure. Testing for your specific application is best. Research the best cleaning method for the type of tubing material you have in mind. Can it be autoclaved? Low-pressure steam sterilized? Gamma irradiated? Cleaned with a specific chemical? Does the application call for a simple flush cleaning with water?
 
Some plastic tubing materials such as polyurethane and PVC are quite durable and chemical resistant. Other materials may handle high temperatures well but not certain cleaning fluids or gases. Depending on the tubing material and cleaning method used, tubing may become brittle or gummy, break down chemically, loose its shape, or absorb the cleaning agent.
 
Consider, too, that depending on the labor, equipment, and resources involved with cleaning or sterilizing the tubing or hose, it may be more efficient to replace it.
 
9. Evaluate surface characteristics
Many people naturally think of plastic as having a smooth surface. The plastic products we use regularly (computers, toothbrushes, phones, pens, cars, items from your kitchen) often have smooth, even glossy, surfaces. In some cases the surface is textured for aesthetic or gripping purposes.
 
What type of surface does the tubing or hose in your application need? Whether your tubing will carry fluid, air, or a granular or powdery substance, you’ll likely want a smooth interior for the most efficient transfer. An irregular surface can cause resistance and slow the rate of flow.
 
Some thermoplastic tubing materials – PVC, for example – offer a very smooth surface (a low coefficient of friction). Others like fluoropolymer and polyethylene are even smoother and feel almost slippery. Polyurethane and certain thermoset rubbers such as silicone can feel tacky, and that might be a desired characteristic in particular applications.
 
What about the exterior? Should it, too, be smooth, or does it need a surface texture like ribbing to make it easier to grip and hold on to? Some tubing styles, specifically stainless steel overbraided types, can be supplied with a protective outer layer of silicone to make the product easier to handle at high temperatures and to eliminate entrapment issues. Other styles are coextrusions where one material is used for the inside and another for the outside. For instance, Hytrel®-lined PVC can be useful in a harsh environment application involving the transfer of oil. The durability of PVC works well for the exterior, while the oil resistance properties of Hytrel are a good fit for the interior.
 
Surface properties can also affect electrical conductivity and static dissipation.
 
10. Know your packaging requirements
Are 100-foot coils of tubing or hose acceptable? Do you need 10,000 straight pieces, each five feet long? Must they be bagged, double bagged for extra cleanliness, boxed, or are stacked coils on a wooden pallet satisfactory? Can lengths of rigid products be cut and boxed to meet requirements for shipping by UPS or a similar carrier, instead of forcing a truck shipment?
 
Knowing how the tubing or reinforced hose will be used can help determine your packaging needs. If it’s going to be inventoried, you may want a protective covering like a bag or box. If the tubing will be used immediately, that may be unnecessary. Ask about bulk packaging (multiple coils or lengths in one box), and see if it will save you money.
 
Perhaps the tubing is part of a kit that you assemble. You’d like six-foot lengths of 1/8″ I.D. clear, unreinforced PVC coiled into 4″ diameter circles, and then placed in individual bags and sealed. Order it that way, so you don’t need to do anything with it other than place each bag with your kit.
 
Do you want the tubing bagged and labeled with your part number, your customer’s, or other useful information such as temperature limitations? Will the tubing be used in a medical, pharmaceutical, or other clean application? Check into having it gamma irradiated before it ships to you, so it’s ready for use upon delivery.
 
Consider the tubing’s application and how the proper packaging can assist the end user. Keep in mind that special packaging is a custom process that will likely involve minimum order quantities, additional lead time, and added costs. 

For more information, check back next week for Tips 11-20. 
Retail Food Safety Forum

All About Food Policy: Interview with Baylen Linnekin

By Chelsey Davis
No Comments

GMOs, FSMA and menu labeling are all hot topics right now in the world of food policy and regulation. To further discuss the latest updates,TraceGains’ Chelsey Davis sat down with Baylen J. Linnekin, Executive Director for Keep Food Legal, Adjunct Professor at George Mason School of Law, and Columnist at Reason, to explore his take on a few of these key issues.

GMOs, FSMA and menu labeling are all hot topics right now in the world of food policy and regulation. To further discuss the latest updates,TraceGains‘ Chelsey Davis sat down with Baylen J. Linnekin, Executive Director for Keep Food Legal, Adjunct Professor at George Mason School of Law, and Columnist at Reason, to explore his take on a few of these key issues.

Linnekin is a licensed attorney and is the founder and executive director of Keep Food Legal Foundation, a Washington, DC-based 501(c)(3) nonprofit that promotes food freedom of choice—the right of every American to grow, raise, produce, buy, sell, share, cook, eat, and drink the foods of their own choosing. He serves as an adjunct professor at George Mason University Law School and an adjunct faculty member at American University, where his teaching focuses largely on contemporary food-policy issues. Along with faculty from Harvard Law School and UCLA Law School, Linnekin is one of six founding board members of the new Academy of Food Law & Policy. He is currently writing his first book, which focuses on the ways that government policies often thwart sustainable food practices, for Island Press. He is also serving as an expert witness in an ongoing First Amendment food-labeling lawsuit.

What are your thoughts on the final rules for menu and vending labeling that are set to be enforced by December 2015 (2016 for vending)? Do you think it will help fight obesity?

Linnekin: From both a theoretical and practical standpoint, mandatory menu- and vending-labeling is a lousy idea. Looking forward—from a theoretical perspective—even the chief architect of the country’s first menu-labeling law, former New York City health department head Thomas Farley, admits menu labeling “won’t stop the obesity epidemic[.]” Practically, we know Farley is right, as study after study has found that mandatory menu labeling doesn’t lead consumers to choose lower-calorie options, and may even cause them to choose options with more calories.

What is your take on “natural” labeling and advertising claims? Do you think things like this should be regulated, or better yet, more specific in regulation?

Linnekin: This is properly a matter for the courts. If someone believes they’ve been harmed by an “all natural” label—e.g., they were tricked into buying something by what they believe is a misleading label—then they should sue. The FDA should stay out of it. Instead, the FDA should permit any food label so long as it contains the required information—including an accurate list of ingredients—and doesn’t contain statements that are demonstrably false (fraudulent).

You talk about GMO labeling in a few of your recently published articles. If Congress were to pass a mandatory GMO-labeling law, what do you think would be the immediate ramifications to food manufacturers?

Linnekin: Mandatory GMO-labeling laws are bad for food manufacturers and consumers. Costs would rise for both thanks to new regulatory requirements and, for the former, threats of lawsuits. Thankfully, there doesn’t seem to be any stomach in Congress for passing a mandatory GMO-labeling law.

Can you elaborate on what you mean when you say things like, our “food freedom is under attack”?

Linnekin: I define food freedom as an individual’s right to grow, raise, produce, buy, sell, share, cook, eat, and drink the foods of his or her own choosing. Federal, state, and local government officials—both elected and working in regulatory agencies—are threatening this individual right. Many cities restrict a person’s right to plant a garden in their own yard, or to share food with the homeless and less fortunate. States have banned foods and food ingredients—from foie gras to Four Loko to raw milk. The federal government subsidizes farmers who grow some crops (i.e., corn and soy) and bans farmers from growing others (e.g., hemp). And it’s cracking down on foods that contain salt, caffeine, trans fats, and other ingredients. The list goes on. If the government were to restrict our speech—what comes out of our mouths—in the same way it does what we put into our mouths, we wouldn’t hesitate to say that free speech is under attack. That’s why I say food freedom is under attack.

With so many food recalls that occurred during 2014 and in previous years, how would you suggest food manufacturers prevent these issues while also not requiring additional regulation?

Linnekin: The U.S. food supply is remarkably safe. That’s thanks in very large part to the nation’s farmers and food manufacturers. The threat of harming consumers and consumer confidence—not to mention the lawsuits and calls for increased regulations that arise when such harm occurs—should be incentive enough for food companies to seek to prevent these issues from arising. But not all food regulations—even newer ones—are bad. I support the FDA’s mandatory recall authority under FSMA for many reasons, including because I think it makes lots of sense given the FDA’s original mission to protect food safety.

Which GFSI Standard is Right for Me, and How Do I Prepare For The Audit?

So your company has decided to pursue certification against a GFSI benchmarked standard. How do you go about choosing the right standard for you, and how can you prepare for your first audit? This article offers some advice.

One of the most important questions to ask before researching and deciding upon a standard for GFSI certification is, “Do any of my company’s current or prospective customers require GFSI certification to a particular standard?

Some customers do require their suppliers to achieve certification to a particular GFSI benchmarked standard and it is worth investigating customer requirements upfront before investing time and resources in the development of a standard specific food safety management system, which is not recognized by a particular customer.

While GFSI benchmarked standards are similar to each other in the core criteria of a supplier’s food safety management system, there are subtle differences with respect to the level of prescriptiveness and certification cycles required by each standard. While GFSI’s motto is “One Certified, Accepted Everywhere,” the reality is that retailers and manufacturers have unique requirements for their suppliers to support organizational initiatives and it is in the best interest of suppliers to understand such requirements for increased market access of their company’s food products.

Identify your company’s preparation profile

Once customer requirements for GFSI certification are evaluated, the next step is to assess management objectives for GFSI certification as commitment and resource requirements maybe different depending on which standard is adopted for certification.

At their most basic level, all GFSI benchmarked standards require the development and implementation of a food safety management system (FSMS) for certification. However, some schemes extend the scope of certification beyond food safety requirements and offer certification of both a food safety and quality management system (FSQMS) such as BRC Global Standard for Food Safety or SQF Code Level 3.

Distinguishing between implementation of these two types of management systems is critical for determining management commitment, resource requirements, implementation of timelines, and maintenance (certification) of the system.

Attributes to consider and evaluate against the different GFSI benchmarked standards when deciding which GFSI standard to implement may include consideration of the following:

  • Type of operation
  • Number of locations
  • Physical size of the facility
  • Number of employees
  • High or low-risk product
  • Number of HACCPs
  • Product category(ies) to be included in scope of certification
  • Ability of management and staff to submit to required unannounced audit during certification cycles.

Developing, implementing, and maintaining a food safety management system is a financial commitment on the part of the company seeking certification with immediate and long term benefits as previously discussed. As such, budgeting for the initial development and implementation as well as continued maintenance of the system is necessary. Consideration should be given to the need for initial training of key management and staff to the selected standard, consultancy, allocation of management and staff time, and initial audit costs. Maintenance of the system should consider continued training needs as new editions of the standards are issued, annual review, revision, and verification of the system, and annual recertification costs.

How to prepare for the audit

In preparation of the audit, it’s helpful to prepare an Internal Preparing Checklist, covering the following aspects:

  • GFSI Standard: Have you determined which GFSI standard best fits your company culture and acquired the current version of the standard?
  • Commitment: Is senior management fully committed to implementation and maintenance of the selected standard’s requirements?
  • Food Safety Management Team: Do you have a qualified HACCP team leader, inter-departmental HACCP team, and designated individual(s) to lead the development and implementation of the food safety management system?
  • Training: Are the company’s designated HACCP and food safety management leads trained in the requirements of the current version of the standard?
  • Readiness: Does the company have a well developed, implemented, and documented HACCP system with core prerequisite programs included allergen management, internal audit, GMPs, process and product segregation, SSOPs, specification approval, supplier approval, recall plan, traceability and training?
  • Timeline: Has senior management set a target date for certification?
  • Consultancy: Do company resources lend itself to successful development of a documented food safety management system, which meets all requirements of the standard, or is there a need for a standard specific consultancy?
  • Internal Audit (Gap Assessment): Has the food safety management team conducted an internal audit of its system against the requirements of the standard? Are “Gaps” or a reason of non-conformance to standard requirements identified with a correction action plan?
  • Third Party Assessment: Is there a need for a third-party (certification body) to conduct a pre-assessment audit of the company’s system against standard requirements? Third party pre-assessments provide objective and competent evaluation of the system by a trained auditor in preparation for the planned certification audit.

The above article has been adapted from a white paper published by CERT-ID, which has over 15 years’ experience in providing certification services globally. For more information, visit www.cert-id.com.

Top 6 Best Practices for Your Allergen Control Program

Undeclared allergens are the cause of a great number of recalls in the United States, causing significant consumer health issues, scrap costs, and sourcing conundrums. Under FSMA, good manufacturing practices are undergoing revisions, and the one area that has gotten the most attention is allergen control.

Undeclared allergens were responsible for the greatest number of recalls in the United States in 2013, causing significant consumer health issues, scrap costs, and sourcing conundrums. Under the Food Safety Modernization Act (FSMA), good manufacturing practices (GMPs) are undergoing revisions — and the one area that has gotten the most attention is allergen control. Under the new GMPs, an emphasis has been put on facilities to have an allergen control program.

Further, 15 million Americans and 17 million Europeans have documented food allergies. According to a study released by the Centers for Disease Control and Prevention (CDC), food allergies have increased by 50 percent among children from 1997 to 2011; and hospital admissions for severe reactions have increased seven-fold in Europe over the past decade, according to the European Academy of Allergy and Clinical Immunology.

FSMA’s Proposed Rule for Preventive Controls for Human Food has two major features–provisions requiring hazard analysis and risk-based preventive controls, and revisions to the existing Current Good Manufacturing Practice (CGMP) requirements found in 21 CFR part 110. Included within these revisions is the requirement that each covered facility prepare and implement a written food safety plan, which includes a hazard analysis, preventive controls (e.g., process controls, food allergen controls, sanitation controls, and recall plan), monitoring procedures, corrective actions, verification activities, and recordkeeping.

Allergen Control Programs are multifaceted with elements ranging from ingredient supplier verification, storage, scheduling, formula and rework control, sanitation and changeovers, and label verification.

In essence, there are two main goals of an allergen control program, which appear simple on paper, but are very difficult to execute.

  • Goal #1: If you make a product with an allergen in it, you need to make sure that the allergen is declared on the label.
  • Goal #2: If you make a product that is NOT supposed to have a specific allergen in it, you need to do everything possible to prevent cross-contact.

So how can you make the most of your Allergen Control Program? Use these 6 Best Practices in this e-book, co-produced by TraceGains Inc. and AIB International. Click here to download.

FDA Seeks Key Investments for Implementing FSMA

The agency makes a case for immediate investments now, and sustained funding in future years, explaining that there is a risk of delayed, uneven, and potentially disruptive implementation of FSMA, to the detriment of public health and the food industry.

The FDA Food Safety Modernization Act (FSMA) was signed into law in January 2011. FSMA reflects the need for a modern, global food safety system that prevents problems rather than primarily reacting to them after they have occurred.

The law, which received bipartisan support, followed a series of severe outbreaks of foodborne illness. It responds to the significant burden of foodborne illness in the United States each year, which the Centers for Disease Control and Prevention estimate at 48 million illnesses, 128,000 hospitalizations, and 3,000 deaths. The economic losses to industry, including farmers, are enormous, estimated at over $75 billion per year.

Since FSMA was enacted, FDA has carried out extensive work to implement the law by publishing key FSMA proposed rules that would provide needed food safety protections for the American public, while at the same time making the proposed rules as flexible as possible and workable.

These proposed rules were informed by current industry practices and by conducting extensive outreach and dialogue across the country and overseas with farmers, manufacturers, commercial food handlers, consumers, and government partners.

Currently, FDA is under court-ordered deadlines to issue all seven of these key final rules:

  • The final rules for preventive controls for human and animal foods are due on August 30, 2015;
  • The final rules on produce safety, Foreign Supplier Verification Programs, and accreditation of third party auditors are due on October 31, 2015; and
  • The final rules for sanitary transportation and intentional adulteration are due on March 31, 2016, and May 31, 2016, respectively.

Implementation

Developing reasonable, effective, and flexible rules is just the first step in FSMA implementation. Much more needs to be done to ensure smooth and effective implementation in late 2016 and 2017. And additional funding is needed to support the following areas:

  • Inspection modernization and training;
  • Furthering the National Integrated Food Safety System;
  • Education and technical assistance for industry;
  • Technical staffing and guidance development at FDA;
  • Building the new import safety system; and
  • Risk analytics and evaluation.

FDA is also committed to change within the agency itself to enhance industry compliance with the FSMA rules. First, FDA is overhauling its inspection model to fulfill FSMA’s prevention mandate. To carry out the new model, FDA will increase specialization of the inspection and compliance workforce, build a new compliance culture within FDA that uses a variety of tools and incentives to achieve compliance, and invest in training to ensure expert and consistent inspections and sound decision making.

Second, the agency will assume that most in industry want to comply with food safety standards and thus will educate before and while it regulates through guidance, education, and technical assistance.

Third, the frequency and manner of FDA’s inspections will be guided by a company’s food safety culture and performance.

The allocation of funds needed in FY 2016 to make these changes is outlined below.

FY 2016 plans for requested budget authority

With a total of $1.3 billion in budget authority, an increase of $109.5 million, requested in the President’s Budget, FDA will make improvements in the following areas, continuing improvements that began with FY 2015 funds.

1. Inspection Modernization and Training – $25 million

FSMA fundamentally changes FDA’s approach to food safety oversight, from primarily reacting to problems to preventing them in the first place. New inspection and compliance strategies will be a key component of this shift. FDA is not requesting more inspectors for domestic inspections, but rather will increase efficiency and effectiveness of current inspectors through the use of new inspectional models and approaches. Inspectors are currently trained to inspect food manufacturers using a compliance model focused on finding evidence of violations and bringing enforcement cases. The new food safety paradigm will be focused on whether firms are implementing systems that effectively prevent food contamination, requiring fundamentally different approaches to food safety inspection and compliance. For example, FDA will deploy more specialized inspectors, supported by technical experts, to assess the soundness and performance of a facility’s overall food safety system and will use data to guide risk-based inspection priority, frequency, depth, and approach. FDA will also focus on ensuring consistency among inspections conducted by FDA or the states on behalf of FDA.

This new paradigm involves a major reorientation and retraining of more than 2,000 FDA inspectors, compliance officers, and other staff involved in food safety activities. FDA has also committed to improving risk-based targeting, which will require better data about facilities, new IT systems to identify and track risk, and methods for assessing and tracking inspection efficiency and inspector competency.

2. National Integrated Food Safety System – $32 million

Congress recognized that the success of FSMA implementation depends on fundamentally new approaches to collaboration among the more than 3,000 state, local, and tribal government agencies involved in food safety. Building a National Integrated Food Safety System is a complex and long-term process. To be successful in aligning state programs with FDA’s new facility inspection and compliance approach, approximately 1,000 state inspectors will need training, and the states will need real-time information sharing capacity with FDA and other states, state laboratory accreditation, and inspector certification programs. Those processes, which will be carried out mostly via FDA grants and cooperative agreements to states, have been ongoing but must be ramped up significantly in 2016 to help ensure that states conduct sound, consistent inspections when industry must comply with the new preventive controls rules starting in late 2016. In addition, to successfully implement the produce safety rule, FDA must build state partnerships and capacity in 2016 to provide education and technical assistance to growers in anticipation of the rule starting to be implemented in 2017.

3. Education and Technical Assistance for Industry – $11.5 million

With FDA’s new approach to ensuring food safety, education and technical assistance are needed to help farmers, processors, and importers—especially small businesses—implement the new prevention-oriented standards. Approximately 300,000 entities could be subject to the final FSMA rules. FDA believes that it should expend substantial financial resources to provide such assistance and will make training materials widely available to protect public health. FDA would use a large portion of these resources to provide financial support to state agencies and public-private-academic collaborative entities, such as the Produce Safety Alliance and the Preventive Controls Alliance.

4. Technical Staffing and Guidance Development at FDA – $4 million

Maintaining an adequate number of highly qualified technical staff at FDA is always a priority and challenge, but FSMA makes it essential to achieve this goal. In addition to regulatory standards for FSMA, FDA is issuing guidance documents that express the agency’s current thinking and are essential to helping industry to comply with the FSMA requirements. Funds are needed now to recruit additional experts at FDA who can ensure that guidance development, which is now underway, is based on the best science and knowledge of industry practices. More experts are also needed to conduct outreach to industry, academia, and state extension services to ensure that their concerns are heard, that their advice is solicited and utilized, and that the guidance documents reflect the most cost-effective solutions achievable. They will also play an essential role in supporting FDA’s inspection and compliance force in properly overseeing implementation of the new standards and achieving high rates of compliance.

5. New Import Safety Systems – $25.5 million

Improving oversight of imported food is crucial to protect public health and ensure consumer confidence in food safety, regardless of whether food is produced domestically or imported. The food consumed by Americans today comes from over 200,000 different food facilities, more than half of which are located outside the United States. For example, about 50% of fresh fruits, 20% of fresh vegetables, and 80% of seafood consumed by Americans is imported. The volume of imported food has increased enormously over the past 20 years, going from fewer than 200,000 line-entries in the early 1990s to an estimated 12 million in 2013. The Foreign Supplier Verification Program (FSVP) mandated by FSMA, will require importers to implement supplier verification plans to help ensure food produced overseas meets U.S. food safety standards. This shift presents an enormous challenge for both FDA and food importers, given that there were approximately 88,000 consignees receiving food shipments last year. To be successful, FSVP implementation will require a substantial regulatory development process, training of more than 400 current FDA investigative and compliance personnel, and the addition of new staff (including 50 in 2016) with the audit skills needed to assess importer safety plans. It will also require extensive training and technical assistance for importers.

6. Risk Analytics and Evaluation – $4.5 million

Focusing decisions and resources on areas of greatest risk to health is a key element of FSMA, so FDA is developing new tools that will provide the information needed to do so. This includes new tools for ranking risks, prioritizing program activities based on opportunities to reduce risk, and linking risk-based priorities more clearly with budget formulation and execution. For example, these tools will better inform FDA about which foods, including animal foods, are most vulnerable to which bacterial contaminants, and where it should invest its research efforts to most effectively identify how to reduce contamination of food. This will improve FDA’s productivity in all areas, including research and standard setting, inspections, and guidance to industry.

Note: The $109.5 million increase in the food safety budget for FDA includes $7 million for necessary infrastructure costs.

Conclusion

Developing reasonable, effective, and flexible rules to create a modern, prevention-based food safety system is a formidable job, but it is just the first step in FSMA implementation. Much more needs to be done to lay the groundwork for smooth and effective implementation of FSMA in late 2016 and 2017. Without an immediate investment now, and sustained funding in future years, there is a risk of delayed, uneven, and potentially disruptive implementation of FSMA, to the detriment of public health and the food industry. 

Source: This article has been adapted from a paper authored by FDA, which can be accessed here

Interview: FSQA Enabling Technologies as a Food Safety and Quality Assurance Game Changer

By Barbara Levin
No Comments

In an interview withFood Safety Tech, Barbara Levin, Senior Vice President and Co-Founder of SafetyChain Software, talks about FSQA Enabling Technologies – the Food Safety and Quality Assurance (FSQA) Game Changer, a series of leadership forums, tech talks and executive briefs that SafetyChain has launched this month.

Barbara-Levin2The focus of the series is how technology can help FSQA teams execute to meet today’s biggest food safety and quality challenges in program management, compliance, continuous improvement, risk mitigation and much more.

Food Safety Tech (FST): SafetyChain is launching a new series, called FSQA Enabling Technologies – the Food Safety and Quality Assurance Game Changer. What is the series about and what will it include?

Barbara Levin: For the past three years, working with thought leaders throughout the food and beverage industry, SafetyChain has helped educate and share insights on critical topics – such as FSMA and GFSI. In 2015, we’re excited to bring the conversation to the next level – to discuss the tools that are available to execute on challenges such as FSMA compliance, managing GFSI programs, risk management/brand protection, audit readiness, cost of quality, supplier compliance, operational KPI performance and much more.

FST: Why is technology an important topic in food safety today as we enter 2015?

Levin: I strongly believe that adoption of FSQA enabling technologies is vital, necessary and inevitable – and the only way food companies are going to be able to scale to meet all of the challenges ahead of them. And industry is realizing this and wants to learn more as technology adoption is becoming more mainstream. Think about the technologies we all use at work and home today – things like employee portals to view our paychecks, email, online banking, all of the apps on our computer tablets – none of us can imagine doing without them now. Well think about suppliers entering Certificate of Analysis info on portals. FSQA folks doing pre-harvest inspections on mobile app forms, getting safety and quality information in realtime to determine if there are non-conformances and CAPAs required. And there are hundreds of other examples. We think these will become a way of life too in food safety and quality. So we’re really excited to provide a forum for this FSQA technology conversation.

FST: What changes have we seen in Food Safety and Quality Assurance enabling technologies that are allowing them to achieve more widespread, mainstream adoption?

Levin: There’s a wrong perception that the food industry lags behind some other industries when it comes to technology adoption. In reality, food companies have automated a lot of their functions – look at finance, human resources, payroll systems, supply chain, purchasing, inventory and such. These functions were automated because it saved time, saved money and created operational efficiencies.

Where there was a lag was in adoption of FSQA technologies. I think that this was because first generation safety and quality technologies were behind the firewall – and as we know food safety and quality folks are not sitting at their desks looking at a computer all day. Instead, they are out in the field doing a pre-harvest inspections, or on the plant floor, or at the supplier site doing an audit, or with the customer… basically they are everywhere except at a desk. But today, there are many cloud-based, mobile food safety and quality technologies that can be accessed anywhere, at anytime – and this has really been a game changer when it comes to adoption. Now, food companies are deploying technologies and gaining the same advantages – saving time, saving money and creating efficiencies that improve FSQA.

FST: What are some of the triggers leading teams to explore technology for the first time?

Levin: The word “more” is key to this answer. FSQA is seeing more regulation (think FSMA), more third party schemes like GFSI to manage, more audits, more pressure to improve operational KPIs and reduce the cost of quality. The only thing there’s not more of usually is people – and so technology is the most efficient way to scale to do “more with less.” Additionally technology is the key to getting FSQA information in the fastest manner possible – for timely CAPAs – and be preventive vs. reactive in ensuring that non-compliant products do not go into commerce.

FST: Where do you see FSQA enabling technologies as having the biggest impact on safety and quality operations?

Levin: For me, FSQA enabling technology can have great impact in these areas:

  • Reducing risk for withdrawals, rejections and recalls;
  • Having real time and continuous information to generate CAPAs and ensure safe, quality food;
  • Managing supplier risk and supply chain controls;
  • Scalability to do more without having to add more people;
  • Being audit ready – for regulatory, GFSI, customer and internal audits all the time – even for unannounced audits;
  • Reducing the cost of quality; and
  • Having actionable data for meaningful continuous improvement.

All of these really come under one umbrella, which is protecting the brand and financial value of your company.

FST: What’s coming up in terms of topics and speakers during the series kickoff?

Levin: The series has three components – Leadership Forums on “big picture” topics, Tech Talks on specific FSQA issues and how technology helps resolve challenges associated with those issues, and executive brief whitepapers on the business side of technology benefits.

The first leadership forum, scheduled for March 13, will feature Bob Butcher, Ipswich Shellfish Company’s FSQA Group Operations Manager, and Jeff Chilton, President of Chilton Consulting Group, and will focus on The Business Case for Food Safety and Quality Technology. Future topics include the Role of Technology in Risk Mitigation and Brand Protection, and Technology as an Enabler to Reduce the Cost of Quality.

The FSQA Tech Talks kick off at the end of March with the following topics:

  • March 31 – Tackling FSMA Compliance: How Automation Enables HACCP-to-HARPC migration, FSMA Reporting, Supply Chain Controls and More
  • April 21 – Harmonizing FSQA – It’s All About the Cloud: How the Cloud and Mobile Technologies Enable Anywhere, Anytime FSQA Data Capture and CAPA Generation
  • May 19 – Facilitating Continuous Improvement: Enabling Actionable Data for Trending, Benchmarking and Reporting Across Your Entire Operation

The first executive brief is available now and is titled, “The Critical Role of FSQA Enabling Technologies for Today’s Food Safety and Quality Operations: Technology as an Enabler to Fundamentally Change How Food Safety & Quality Operations Manage Risk and Meet Key Performance Indicators.”

Additional details on the entire series – along with registration and download information – is available at www.safetychain.com/2015TechSeries.

FST: Who should attend this series, and how can they get more information?

Levin: Folks from Food Safety, Food Quality, Operations, Legal, Financial, Executive and Information Technology Management from all sectors of the food and beverage industry are encouraged to register and participate in the series. Everything is complimentary and new topics and dates will be announced frequently. We also invite FoodSafetyTech readers to let us know what topics they’d like to see – they can email us at info@safetychain.com.

Developing an Effective Environmental Monitoring, Sampling and Testing Program

By Food Safety Tech Staff
1 Comment

As the food industry is moving toward a more preventive food safety strategy, environmental monitoring is playing an increasingly critical role in testing. Hazard analysis is shifting the focus from finished product testing to proactively testing the environment and the processing as critical control points to continuously monitor and reduce risk. Today many facilities are adding or strengthening their environmental monitoring programs to enhance their food safety risk reduction efforts.

In a recent webinar, Ann Draughon, Emeritus Professor of Food Microbiology and Toxicology, University of Tennessee spoke about Developing an Effective Environmental Monitoring, Sampling and Testing (EMS) Program. We present some excerpts from her presentation.

What do you need to get started with an EMS program?

“You need to first identify the right team; think about what kind of food you are processing (raw products or ready-to-eat products) and if it has had any food safety outbreak associated with it; determine critical or hygiene zones in your facility; determine sample locations; finalize which indicator tests will be done, and in which zones; determine which pathogens you will test for; choose the right test methods; set a baseline, and link that with your sampling plan, and establish testing frequency once you have finalized the number of samples and zones,” explains Draughon.

To establish critical hygiene zones, she advises to:

  • Survey entire facility and have a map of that facility;
  • Study that map and identify traffic patterns to divide the facility into critical hygiene zones, GMP zones, and non-processing zones;
  • Put in place barriers between these zones and dedicate equipment to the critical hygiene zone, and restrict access between zones; and
  • Establish strict cleaning, sanitation and monitoring plans for these diff zones.

Sampling of zones should be based on risk of contamination and/ or transmission of pathogens to food from environment, says Draughon. The sampling should also take into account potential sources of product contamination by whatever means during food processing (see image 1 for examples of 4 zone and 3-zone hygiene systems).

Selecting the right assays for your EMS program

There are many options, and it can be confusing to select the right assay for your needs. Draughon advises that companies need to look their monitoring needs and consider both indicator bacteria and pathogenic bacteria to select the right assay.

For monitoring with indicator bacteria, most companies look at ATP for environmental sanitation, often before start-up to make sure facility is clean before processing begins. Protein assays are also used to pick up any allergen on equipment.

APC or total viable count is a simple assay offering many choices, which tests for the number of live bacteria on your equipment or in your environment that can grow under air or oxygen at room temperature.

Yeast/ mold count assays are good for two purposes: 1. Mold frequently is the cause of spoilage in food, so it’s useful to understand if there are any present to determine shelf life, and 2. It also helps us understand the number of particulates in the air.

We can also select specific microbial groups as indicators, such as total Enterobacteriacae, fecal coliform or E.coli or Listeria species.

Sample collection and prep

When we collect a sample, we have to clearly document the sample including information such as when it was taken, from where, by whom, what happened to that sample etc. Use clean SOPs to reduce error. Use the assays previously selected and do it as quickly as feasible. If you are working with an outside company, decide how they are going to handle the sample. Finally, always keep in mind plant safety and leave nothing behind after sampling, and avoid cross-contamination.

For characterizing pathogens, you may want to genetically fingerprint any pathogenic isolates from your facilities. This will allow you to see if you have a constant harborage of a particular pathogen or if it changes. Draughon recommends using a contract lab for characterizing pathogens, as they would be better suited, and have better resources to do this. Destroy the isolates after characterization – you don’t want any chance of the pathogen spreading into the product or the environment.

Written SOPs for EMS programs

It’s critical to have clear written SOPs for EMS programs which include the following:

  • Frequency of sampling;
  • When, where , how and duration of sampling;
  • Procedure for recording data and coding;
  • Sample number, size or volume;
  • Specific sampling and analysis validated protocols;
  • Monitoring of incubators and use of equipment;
  • Handling and shipping of samples; and
  • Alert and action levels and appropriate response to deviations from alert or action levels.

It’s also important that we train and validate the personnel performing EMS. Each individual doing this needs to demonstrate proficiency of doing this. They need to understand proper recording of EMS program data, alert and action levels, and zero tolerance levels. The personnel should be comfortable and qualified for sampling protocol, and using all the equipment.

In summary, sampling plans should be adaptable, which highest risk sites being tested initially. Establish a baseline and modify sampling plan as needed. Establish your sampling and testing criteria and sample as needed with each zone to fully assess the environmental program.

Thomas R. Weschler, Founder and President, Strategic Consulting, Inc (SCI)

Faster, Better, Cheaper… What’s Most Important in a Pathogen Test?

By Thomas R. Weschler
No Comments
Thomas R. Weschler, Founder and President, Strategic Consulting, Inc (SCI)

 TomWeschlerJan2015

For close to 20 years, Strategic Consulting Inc. (SCI) has been following the industrial microbiology market, and food safety testing applications in particular. As part of the data gathering for our most recent report, Industrial Microbiology Market Review, SCI interviewed 15 senior managers at major food companies and food contract labs (FCLs) to understand their priorities when choosing a pathogen diagnostic method. The interviews were roughly split between food companies and food contract labs.

SCI identified ten important attributes for evaluating a diagnostic method or instrument, and asked the interviewees to stack rank the top five items most important to them.

The three top-ranked choices were the same at both food companies and FCLs, with sensitivity/specificity the most important attribute. Second in importance was the ability of the method to be utilized in a broad range of food matrices. Ranking third was the cost-per-test for diagnostic reagents.

For food companies, time-to-results (TTR) was tied for third in the stack ranking, followed by ease-of-use (EOU)/automation in fifth place. Clearly food companies want quick results but only after they are assured that the pathogen diagnostic they are using provides accurate results and is able to work with a range of food types.

For food contract labs, the cost of the pathogen diagnostic instrument ranks fourth, and TTR is tied with the cost of labor per test for fifth. For FCLs, most of the key attributes in method selection are based on operational considerations, which makes perfect sense given testing is their business.

Mitigate Food Contamination Risk

Whether mycotoxins or microbiological values, heavy metals or pesticides – independent sampling and testing provide an objective and comprehensive overview of what food products contain and help comply with food safety regulations.

Nuts containing mould, frozen strawberries contaminated with hepatitis pathogens, and pesticide-laden vegetables – more than 3,000 products were objected by EU authorities in 2013. With increasing government, industry and consumer concerns about the hazards of food contaminants, and the risks they pose, food manufacturers, governments and non-governmental agencies, are implementing policies and processes to monitor and reduce contaminants.

Key food contaminants

Food contaminants cover a wide range of potential substances including:

  • Dioxins: Produced as unintentional by-products of industrial processes such as waste incineration, chemical manufacturing and paper bleaching, dioxins can be found in the air, in water and contaminated soil.
  • Allergens: Virtually all of the known food allergens are proteins that can subsist in large quantities and often survive food processing.
  • Genetically modified organisms (GMOs): Banned in a number of countries, controversy still exists with regard to the use of GMOs. Selling food and/or feed that is non-GMO in restricted markets places the burden of proof on the supply chain.
  • Heavy metals: Whilst heavy metals, such as lead (Pb), cadmium (Cd), mercury (Hg) and arsenic (As), can be found in nature, industrial and environmental pollutants have resulted in their increased presence in food and feed.
  • Hormones: Commonly used in animal husbandry to promote growth, hormone residues can be found in the food supply.
  • Melamine: Harmful to animal and human health, melamine is not a permitted food additive.
  • Mycotoxins: Produced by several strains of fungi found on food and feed products, mycotoxins are often invisible, tasteless, and chemically stable both at high temperatures and during long periods of storage.
  • Pesticide residues: Over-use of pesticides can lead to dangerous levels of hazardous chemicals entering the food chain with fresh fruit and vegetables being most susceptible to pesticide residues.
  • Polychlorinated biphenyls (PCBs): Used in many products, some PCBs are toxic and stable enough to resist breaking down even when released into the environment.
  • Radiation contamination: There are three ways that foodstuffs can become contaminated by radiation: surface, ground and water contamination.
  • Veterinary drug residues: Used in the treatment of animals, veterinary drugs can leave residues in animals subsequently sent into the food chain. The impact of contaminants varies. Depending on their toxicity and the level of contamination their effects can range from causing skin allergies, to more serious illnesses (including cancers and neurological impairments) and, in the most extreme cases, death.

To ensure that your food and feed products are fit for consumption, you need to test for specific contaminants throughout the value chain. For example, in concentrated levels, melamine, antibiotics and hormones can be harmful to animals and humans. Only thorough contaminant testing will determine if the above-mentioned impurities, among others, are present. After identification the relevant goods can be eliminated from the production and distribution chain.

Maximum levels and regulations

In order to protect consumers, maximum levels permitted in food products have been set by food safety legislation in many countries. Disappointingly, and despite efforts in some product areas, maximum levels are rarely harmonized across national borders. This inconsistency places responsibility for compliance firmly with the food supply chain. A comprehensive testing program can verify that your products meet maximum levels and the safety standards they represent.

In the European Union (EU), it is the food business operator who carries primary responsibility for food safety and the General Food Law Regulation (EC) 178/20022 is the primary EC legislation on general food safety. More specific directives and regulations compliment this, for example, EU regulations concerning non-GMO/GMO products, include Directive 2001/18/EC and regulations 1829/2003 and 1830/2003.

The U.S. Food and Drugs Administration has overseen the development and signing into law of the Food Safety Modernization Act (FSMA). Within the U.S., state regulators retain the right to apply additional regulations and laws. As result, rules regarding maximum levels, for example, vary from state to state.

In China, the Food Safety Law (FSL) was passed into law by the Chinese government in 2009. It introduced enhanced provision for monitoring and supervision, improved safety standards, recalls for substandard products and dealing with compliance failures.

Brazil’s food safety agency, Anvisa, coordinates, supervises and controls activities to assure health surveillance over food, beverages, water, ingredients, packages, contamination limits, and veterinary residues for import. No specific restrictions have been established yet for export.

Monitoring

Monitoring programs are frequently used to identify any contamination issues. From seeds, through the growing process and harvest, transportation, collection, storing and processing to the market channel, independent monitoring delivers credible and independently collected data on both quality and contaminants.

With so many policies and standards, both nationally and internationally, anyone involved in the food industry needs to be sure of accurate and up-to date information on food contaminant regulations. Whether mycotoxins or microbiological values, heavy metals or pesticides – independent sampling and testing provide an objective and comprehensive overview of what grain and food products contain.

For more information, please visit: www.SGS.com/foodsafety.

How to Run an Audit-Ready Co-Pack Operation

By James Houghton
No Comments

If an auditor were to walk through your site today, would you be proud of its set-up and its ability to uphold quality and regulatory standards for yourself and your client?

I think many of us have once been – or are still – in a state of scurrying around right before an auditor knocks on our front doors. When you’re small and growing quickly, it’s hard not to be reactive for things like regulatory audits. But at some point, you have to proactively build out repeatable processes to drive long-term growth, and start really taking control of your own operation.

Here’s the ideal:

You want your co-pack operation to be in a state of audit-readiness. That is, if an auditor were to walk through your site today, you’d be proud of its set-up and its ability to uphold quality and regulatory standards for yourself and your client.

Earlier in October, I presented a webinar on “How to Run an Audit-Ready Co-Pack Operation,” i.e., how to get your house in order. Here are the five pillars of maintaining a state of audit-readiness for your co-pack operation:

Culture

In the same way that you have built a culture of collaboration and client satisfaction you’ll also need to build one for Quality. The way you prioritize and permeate Quality initiatives throughout the organization, from your senior team to your shop floor staff, will show when the auditor walks through the doors.

Paperwork

It’s vitally important that your paperwork is in order, including your SOPs, transactional items like RFQs, POs, and SOWs, and most importantly, the batch record. The auditor will be looking for two things amongst all of your documentation: content and consistency. The content needs to meet regulatory requirements, and there needs to be consistency between what you say you do and what you actually do.

It’s not rocket science: you need to write out what you do, and then you have to do the activities that reflect what you’ve written down. This is often the one thing that won’t be maintained properly, unless it’s given attention.

Physical Space

Your physical space will be audited to ensure it’s set up with the correct flow, that it is kept clean, and there is documentation to that effect.

To make sure your physical space is up to par for an audit, imagine that you yourself are the product… go back to your receiving doors and physically walk through your facility, as a “day in the life” of your product. You’ll be able to see where you go, how you are handled, and where each step is documented. Along the way, anything that’s not delineated, not treated or identified properly, or does not follow a logical flow, are the areas you need to lock down before an audit.

Material Control

An auditor will want to see that you’re in control of your materials, and that you have track and traceability. Being able to track where you’re storing things in the site, where it’s moving, what your processes are for moving inventory, etc… all that demonstrates that you have the traceability controls to be able to handle mock and real recalls and maintain consumer safety.

Production

Ahh… the production line. It’s where the magic happens. When setting up your production line, you need to make sure you have appropriate line clearance, the lines are segregated, the correct staff are on the line to do the project, and that they have had the proper training for their particular activity in the line. In the co-pack world, where things are highly customized with low repeatability, it can be easy to overlook the extensive amount of training it takes to make sure each production line is in good hands. You need, however, to make sure you do your due diligence to maintain production accuracy, quality assurance, and regulatory standards.

In the webinar, I discuss each of these areas in greater detail. If maintaining a state of audit-readiness is an endeavor you’d like to pursue, watch the webinar for more details or access the slide deck by clicking here