As the enforcement of rules, regulations and inspections get underway at food production facilities, we are faced with maintaining production rates while looking for infinitesimal pathogens and cleaning to non-detectible levels. This clearly sets demand on the plant for new and creative methods to control and mitigate pathogens pre-production, during production and post production.
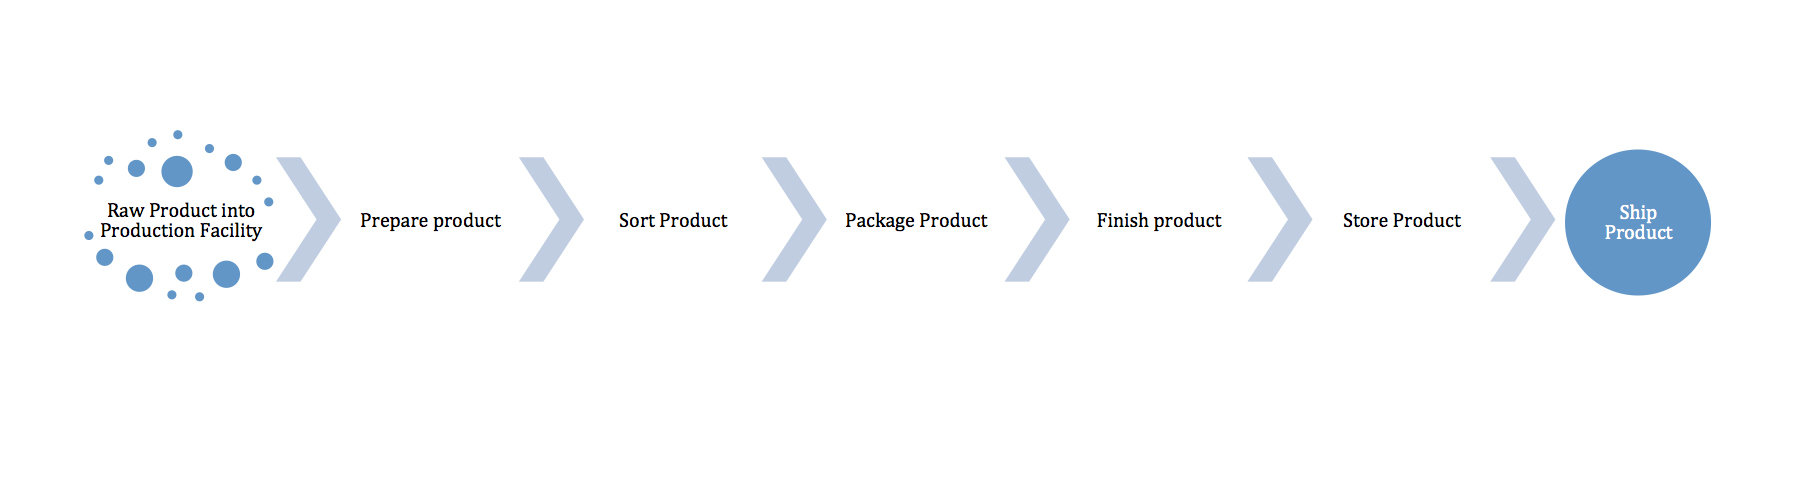
As this occurs, the term clean takes on new meaning: What is clean, and how clean is clean? Swab and plate counts are now critically important. What method is used at the plant, who is testing, what sampling procedure is used, and how do we use the results? As we look at the process from start to finish, we must keep several key questions in mind: What are harboring points in the process, and what are the touch-point considerations to the product? Let’s review the overall processing progression through the factory (see Figure 1).
Figure 1. The progression of processing of a food product through a facility.
Now consider micro pathogen contamination to the product, as we look deeper in the process for contamination or critical control points as used in successful HACCP plans. Consider contamination and how it may travel or contact food product. It is understood through study and research of both pathogens and plant operations that contamination may be introduced to the plant by the front door, back door, pallet, product, or by a person. In many cases, each of these considerations leads to uncontrolled environments that create uncontrolled measurements throughout, which lead to cleaning procedures based on time rather than science. This is certainly not to say that creating a preventive maintenance schedule based on a calendar is a bad thing. Rather, the message is to consider a deeper look at the pathogens and how they live and replicate. From the regulatory and control measures this should be a clear message of what food-to-pathogen considerations should be taken at the plant level as well as measurement methods and acceptable levels (which is not an easy answer, as each product and environment can change this answer). A good example to consider is public schools and children. Health organizations work to help the schooling system understand what immunizations children should have based on the current health risk tolerance levels. In food production, the consideration is similar in an everchanging environment. As we see contamination levels change the methods, techniques and solutions to proper food production must account for the pathogens of concern.
Contamination, Risk tolerance, Opportunity for Growth
Contamination, risk tolerance, and opportunity for growth are the considerations when looking at a plant design or a plant modification. Modification to modernization should be a top-of-mind critical quality control measure. If there are a few things we know, it is how to produce food at high rates of speed, measure and value production rates, and delays or failures can be measured by equipment and personnel performance. In the case of quality control, we must review, comprehend, and protect process risk. From a management or non-technical viewpoint, quality control can be very difficult to understand. When discussing pathogens, our concerns are not visible to the human eye—we are beyond a dirty surface, weare looking at risk tolerance based on pathogen growth in logarithmic measurement. When combining quality control and production, the measurement control and mitigation measures complement the effort. The use of quality control is expected and should coordinate with production to ensure the product is produced at the expected quality level.
Now that the first of the FSMA compliance dates have passed, let’s look back at the past year of training new PCQIs, their questions and concerns from classes as well as the perspective from our FDA friends (yes, really!) who attended our workshops. We have learned so much, it is hard to narrow it down to only five things—but if we look at the issues that arose, the following five proved to be recurring themes throughout 2016.
5. Don’t Scrap Your Current Plan
Many clients have approached us and said they were planning to throw their current food safety and/or HACCP plan in the trash and start from scratch. Please don’t do this! Companies that care about quality and food safety already have effective quality management systems in place. It would be a disservice to the company and the general public for all these time-tested plans to go straight into the bin. It is more realistic to take a look at the current system in light of the new regulation and ask yourself if there are any gaps that can be addressed. This brings us to the next point.
4. Education Is Key
A compliant system cannot be developed without an understanding of the requirements. Although FSMA is derived from the basic principles of HACCP, there are key differences, and not all of them in the direction of less regulation. It is important to understand not only the updated Good Manufacturing Practices and Preventive Controls for both Human and Animal food, but also the Foreign Supplier Verification Program, Sanitary Transportation and the Produce Rule (if they apply). Although the FDA-recognized curriculum for some of these companion regulations have not yet been released, some independent training providers are offering workshops to help fill the gap while the FDA and FSPCA are working on the official curriculum. (Comment on this article for more information via email).
3. “You Must Evaluate If You Need It” Is Not the Same as “You Don’t Need It”
Some training providers have told their attendees that they can scrap many of their current systems because FSMA is less stringent than GFSI-approved schemes. Your certification body for FSSC 22000, SQF or BRC does not care one whit how stringent FSMA is (as long as you are compliant with its requirements, as local regulatory compliance is a key factor in GFSI approval). FSMA will not change expectations related to the GFSI-approved food safety schemes. It is also misleading to think that because FSMA is flexible, FDA regulators will not have expectations of excellence when they arrive at food processing facilities. This law gives regulators the power to take legal actions to address many infractions they have seen over the years but have been powerless to stop; the flexibility may well be a double-edged sword in that regard. Ensure that all decisions are based on data and records exist to validate any claims.
From countless recalls, to FSMA deadlines, to the rising demand for transparency, 2016 has been a monumental year in the food industry. With 2017 knocking, here are the top trends and predictions to watch out for in the food industry next year.
1. Moving Toward a Fully Digital, Connected Supply Chain
The food supply chain in many ways is still lagging behind in technology compared to other supply chains. In 2017, many companies will begin or continue on their journey to fully digitize their supply chain, whether that is simply getting their list of approved suppliers out of an Excel spreadsheet and into a supplier management software technology solution or fully capturing every step of their products along the journey from farm to fork.
The spectrum of digitization across the supply chain is quite broad. But bottom line, supply chain analytics will empower food companies to create useful KPIs, allow them to truly measure the ROI of their supply chain initiatives and give consumers the transparency that they demand. And systems that fully support the daily monitoring, sharing and interpretation of those analytics needed to help companies will experience tremendous growth in 2017.
Collaboration with your supply chain partners is an absolutely critical element, and we can expect to see more companies fully integrate throughout their network of suppliers and customers. Food companies that will succeed in 2017 will need a fully integrated supply chain network, with access to the same information, working towards a shared mission to deliver results and be ahead of their competitors. A connected supplier network will allow food companies to be agile when faced with an issue, responsive to recalls, as well as be flexible and efficient.
2. Recalls, Recalls, Recalls
We saw a high volume of recalls this year, and this trend is not going away anytime soon. As more and more advances in food testing are made, companies will have access to new technologies across their supply chain that will identify issues early. Consequently, more products will need to be pulled out of the supply chain because of that increased testing in order to maintain consumer sentiment.
The companies that are able to roll out these capabilities quickly and efficiently—armed with the data needed—will be well poised to manage their supply chain, potential recalls and the impact to their customers. With the knowledge that we can expect to see several recalls in the new year, food companies should be looking to mitigate risks and better manage their supply chain.
3. Full-force FSMA Is Here Whether You Like It or Not
FSMA focuses on amplifying preventive controls for food production in order to alleviate potential food contamination outbreaks, and the past two or more years have been focused on this preparation. This preparation will come to a pinnacle in 2017, the first full year of FSMA implementation worldwide, with the FDA starting audits for larger companies. This could lead to the FDA requesting required records, conducting audits and in the worst situation for food companies, shutting down operations if they feel it’s necessary.
FSMA will require detailed record keeping when a recall or outbreak occurs, with clearly defined corrective actions in place. Companies will see an increased need for technologies that help supply preventive processes such as food allergen and sanitation controls, as well a prepared recall and supply chain plan. Tracking and traceability will be the two key parameters that will offer manufacturers the ability to examine specific foods and trends to improve their overall process. In order to comply with these new FSMA regulations at every step of the process, food companies will increasingly look to utilize these technologies to account for full traceability of the supply chain.
4. Growth in Foodservice At the Consumer’s Doorstep
Brands like Starbucks and Panera have been testing the food home delivery waters, but more companies seem to be jumping onto the trend of bringing gourmet food directly to the consumer’s doorstep—Blue Apron, Plated, HelloFresh just to name a few.
Anyone who has attended a food safety conference in the last few years has experienced some type of whole genome sequencing (WGS) presentation. WGS is the next big thing for food safety. The technology has been adopted by regulatory agencies, academics, and some food companies. A lot has been said, but there are still some questions regarding the implementation and ramifications of WGS in the food processing environment.
There are a few key acronyms to understand the aspects of genomics in food safety (See Table I below).
PFGE
Pulse Field Gel Electrophoresis
Technique using restriction enzymes and DNA fragment separation via an electronic field for creation of a bacterial isolate DNA fingerprint; PFGE is being replaced by WGS at CDC and other public health laboratories
WGS
Whole Genome Sequencing
The general term used for sequencing—a misnomer—the entirety of the genome is not used, and depends on the analytical methodology implemented
NGS
Next Generation Sequencing
NGS is the next set of technology to do WGS and other genomic applications
SNP
Single Nucleotide Polymorphisms
A variation in a single nucleotide that occurs in specific position of an organism’s genome; Used in WGS as a methodology for determining genetic sameness between organisms
MLST
Multilocus sequence typing
A methodology for determining genetic sameness between organisms; Compares internal fragment DNA sequences from multiple housekeeping genes
16S
16s RNA sequencing
A highly conserved region of the bacterial genome used for species and strain identification
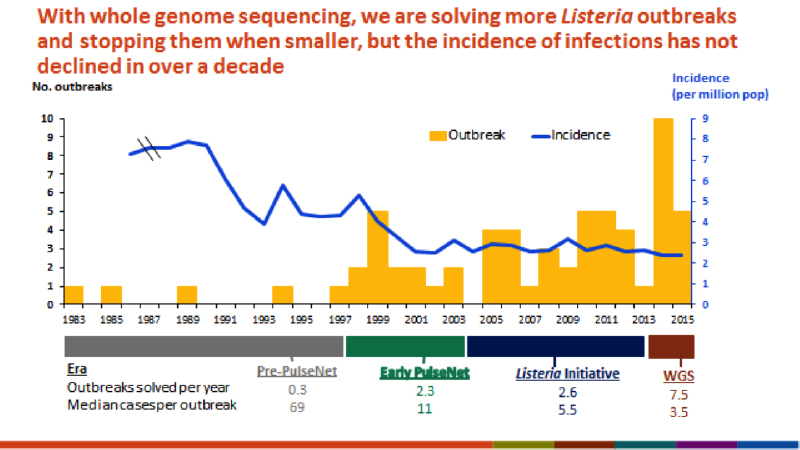
Joseph Heinzelmann will be presenting: Listeria Testing Platforms: Old School Technology vs New Innovative Technology during the 2016 Food Safety Consortium | LEARN MOREIn 1996, the CDC established the PulseNet program for investigating potential foodborne illness outbreaks. PulseNet has relied on using bacterial DNA fingerprints generated via PFGE as comparisons for mapping potential sources and spread of the outbreaks. Due to a number of advantages over PFGE, WGS is quickly becoming the preferred method for organism identification and comparison. Moving to WGS has two critical improvements over PFGE: accuracy and relatedness interpretation. Like PFGE there are nuances when defining the difference between two very closely related organisms. However, instead of defining restriction enzymes and comparing the number of bands, the language changes to either single nucleotide polymorphisms (SNP) or the number of alleles. The other important aspect WGS improves is the ability to determine and interpret the relatedness of organisms more broadly. The frequent Listeria outbreaks and incidence from 1983-2015 provide an insight to what the future might hold with WGS implementation.1 The incidence report shows the increased ability to quickly and more accurately define relatedness between clinical cases creates a link of potential cases much faster.
WGS also provides key practical changes for outbreaks and recalls in the food industry. Sequencing provides a much faster response time and therefore means the outbreaks of foodborne illness decrease, as does the number of cases in each outbreak. As the resolution of the outbreaks increases, the number of outbreaks identified increases. The actual number of outbreaks has likely not increased, but the reported number of outbreaks will increase due increased resolution of the analytical method.
Figure 1: (Permission for use of slide from Patricia M. Griffin, M.D. – Center for Disease Control and Prevention)
WGS continues to establish itself as the go-to technology for the food safety agencies. For example, the USDA food safety inspection service recently published the FY2017–2021 goals. The first bullet point under modernizing inspection systems, policies and the use of scientific approaches is the implementation of in-field screening and whole genome sequencing for outbreak expediency.
Agencies and Adoption
The success of FDA and CDC Listeria project provides a foundation for implementation of WGS for outbreak investigations. The three agencies adopting WGS for outbreak investigations and as replacement for PulseNet are the CDC, FDA and USDA. However, there are still questions on the part of the FDA for when WGS is utilized, including under what circumstances and instances the data will be used.
In recent public forums, the FDA has acknowledged that there are situations when a recall would be a potential solution based on WGS results in the absence of any clinical cases.2 One critical question that still exists in spite of the public presentations and published articles is a clear definitions of when WGS surveillance data will be used for recall purposes, and what type of supporting documentation a facility would need to provide to prove that it had adequate controls in place.
A key element is the definition between agencies for sameness or genetic distance. The FDA and FSIS are using a SNP approach. A sequence is generated from a bacterial isolate, then compared with a known clinical case, or a suspected strain, and the number of different SNPs determines if the strains are identical. The CDC is using the Multilocus sequence typing (MLST) approach.
Simple sequence comparisons are unfortunately not alone sufficient for sameness determination, as various metabolic, taxa specific and environmental parameters must also be considered. Stressful environments and growth rates have significant impact on how quickly SNPs can occur. The three primary pathogens being examined by WGS have very different genetic makeups. Listeria monocytogenes has a relatively conserved genomic taxa, typically associated with cooler environments, and is gram positive. Listeria monocytogenes has a doubling time of 45–60 minutes under enrichment conditions.3 These are contrasted with E. coli O157:H7, a gram negative bacteria, associated with higher growth rates and higher horizontal gene transfer mechanisms. For example, in an examination of E. coli O104, and in research conducted by the University in Madurai, it showed 38 horizontal gene elements.4
These two contrasting examples demonstrate the complexity of the genetic distance question. It demonstrates a need for specific definitions for sameness within a microbiological taxa, and with potential qualifiers based on the environment and potential genetic event triggers. The definitions around SNPs and alleles that define how closely related a Listeriamonocytogenes in a cold facility should be vastly different from an E. coli from a warm environment, under more suitable growth conditions. Another element of interest, but largely unexplored is convergent evolution. In a given environment, with similar conditions, what is the probability of two different organisms converging on a nearly identical genome, and how long would it take?
MLST vs. SNP
As previously stated, the three agencies have chosen different approaches for the analytical methodology: MLST for CDC and SNP of the FDA and USDA. For clarity, both analytical approaches have demonstrated superiority over the incumbent PFGE mythology. MLST does rely on an existing database for allele comparison. A SNP based approach is supported by a database, but is often used in defining genetic distance specifically between two isolates. Both approaches can help build phylogenetic trees.
There are tradeoffs with both approaches. There is a higher requirement for processing and bioinformatics capabilities when using a SNP based approach. However, the resolution between organisms and large groups of organisms is meaningful using SNP comparison. The key take away is MLST uses a gene-to-gene comparison, and the SNP approach is gene agnostic. As mentioned in Table 1, both approaches do not use every A, T, C, and G in the analytical comparisons. Whole genome sequencing in this context is a misnomer, because not every gene is used in either analysis.
Commercial Applications
Utilizing WGS for companies as a preventive measure is still being developed. GenomeTrakr has been established as the data repository for sequenced isolates from the FDA, USDA, CDC and public health labs. The data is housed at the National Center for Biotechnology Information (NCBI). The database contains more than 71,000 isolates and has been used in surveillance and outbreak investigations. There is a current gap between on premise bioinformatics and using GenomeTrakr.
The FDA has stated there are examples where isolates found in a processing facility would help support a recall in the absence of epidemiological evidence, and companies are waiting on clarification before adopting GenomeTrakr as a routine analysis tool. However, services like NeoSeek, a genomic test service by Neogen Corp. are an alternative to public gene databases like GenomeTrakr. In addition to trouble shooting events with WGS, NeoSeek provides services such as spoilage microorganism ID and source tracking, pathogen point source tracking. Using next generation sequencing, a private database, and applications such as 16s metagenomic analysis, phylogenetic tree generation, and identification programs with NeoSeek, companies can answer critical food safety and food quality questions.
Recalls are an inevitable reality of working in the food industry. Indeed, hardly a day goes by without one food company or another announcing a recall. According to the USDA, 150 food products were recalled in 2015. From large national brands like Tyson Foods and McCormick to smaller local manufacturers, no food company is immune from recalls.
Recovering from the sometimes devastatingly expensive recall process can be difficult, so it’s obviously best to avoid problems whenever possible. Understanding the top three reasons for food recalls is the first step toward greatly reducing how frequently they affect your food company.
1. Cross Contamination
Many food manufacturers process multiple products in a single factory. This can lead to cross-contamination issues involving foods to which people are commonly allergic, namely milk, wheat, soy and peanuts. Because cross contamination is sometimes unavoidable, manufacturers are permitted to sell cross-contaminated food, provided the potential contaminants are declared as allergens on the label. According to the USDA’s report, undeclared allergens accounted for 58 of the 150 food recalls in 2015, and milk has been identified as the number one offender.
How to Prevent Cross Contamination. Food is often contaminated because machinery isn’t properly cleaned between uses. Therefore, the most effective way to prevent it is to thoroughly clean equipment after processing food that contains common allergens. Visually inspecting the equipment following cleaning is important, but unseen residue can linger.
To overcome this, in-plant allergen testing of equipment, post cleaning, is recommended. Some tests utilize quick, non-allergen-specific colorimetric tests to identify sugars, proteins and other indicators that an allergen is present. More expensive enzyme-linked immunosorbent assay (ELISA) kits are more sophisticated and may be a better choice if cross contamination plagues your food manufacturing plant.
Other tips to prevent a recall caused by allergen contamination include:
Establishing spill-cleanup protocols
Training personnel on allergen management
Designing equipment with sanitary principles in mind, including self-draining equipment, smooth edges and rounded corners
Carefully inspecting product labels for accuracy
2. Pathogens
Recalls from pathogen-contaminated products are highly damaging because they affect all consumers, not just those with specific allergies. Listeria, E. coli and Salmonella are the most common—resulting in a combined 17 food recalls in 2015, according to the USDA’s report. Several foods have been identified as being most at risk for carrying these pathogens:
Deli meats, soft cheeses and other foods that usually aren’t cooked
Poultry, eggs, undercooked beef, and unpasteurized milk or juice
Raw fruits and vegetables
Raw or undercooked shellfish
Home-canned foods with low-acid content — including asparagus, corn, green beans and beets
How to Prevent Pathogens. As with avoiding cross contamination, the best way to prevent a pathogen outbreak is to implement hygienic manufacturing practices. Four specific techniques apply here:
Separate raw products from cooked/ready-to-eat products. Your efforts should even go as far as separating employees who work in each area. They should use divided washing facilities, locker rooms and cafeterias.
Control the temperature and moisture level to reduce bacteria and mold growth. Anywhere condensation forms or moisture is left to pool, micro-organisms can potentially grow and create a contamination issue. Ventilation and air conditioning can help tremendously with this, as can air dryers used to sap moisture from steamy air.
Implement pest-control techniques. Rats, flies and cockroaches are significant carriers of Listeria, Salmonella, Vibrio cholera and other bacteria. Effective pest-control techniques include disposing of garbage properly, sealing pest entry points, and using air curtains and screens to keep flies out.
Choose durable, easily cleanable equipment for your manufacturing plant and wash all surfaces regularly. Mold and bacteria can start growing within a matter of hours, so keeping surfaces clean is essential. Proper hygiene among plant personnel is critical as well.
3. Physical Contamination
When non-food items are found in food products, a recall is inevitable. Metal, plastic, wood and even insect body parts are examples of physical contaminants. Food is also considered physically contaminated if it’s chemically or biologically tainted. According to a Food Standards Agency report, of the 107 physical contamination incidents in 2012, the most common malefactors were metal (37), pests (23) and plastic/glass (10 each).
How to Prevent Physical Contamination. Foreign objects often enter food products when malfunctioning equipment or human error breaks down the production process. Safeguards such as X-ray scanning, metal detection and filtration/sieving processes help catch foreign objects before they’re shipped, but these aren’t foolproof methods. You should also only work with trustworthy suppliers and take the time to examine raw materials before using them.
The general public expects food manufacturers to produce safe, untainted food. By following these tips, you help uphold your brand and avoid the expensive, reputation-damaging effects of food recalls.
The Final Rule on Preventive Controls for Animal Food (21 CFR 507) was released in September 2015. The first compliance dates for CGMPs arrived in September 2016. All facilities that manufacture, process, pack or hold animal food for consumption in the United States are required to comply (see Figure 1 information on compliance dates.) Non-compliance is considered a prohibited act, but nonetheless this rule has not received the same amount of press as its human food counterpart. We must begin to spread awareness, because this rule has the potential to fundamentally change the pet food and animal feed industries over the next four years. Unlike human foods, animal food is typically intended to be fed as a sole source of nutrients. Thus, the regulation is fairly comprehensive and strict.
Business Size
CGMP Compliance Date
PC Compliance Date
Business other than small and very small
One year
Two years
Small business (fewer than 500 full-time employees)
Two years
Three years
Very small business (averages less than $2.5 million per year, during the three-year period preceding the applicable calendar year in sales of animal food + market value of animal food manufactured, processed, packed or held without sale
Three years
Four years except for records to support its status as a very small business
(January 1, 2017)
Figure 1. Compliance dates for CGMPs and PCs for Animal Food (from fda.gov).
During the 2016 Food Safety Consortium, Debby Newslow and Erika Miller will instruct: FSPCA Preventive Controls for Animal Food (21CFR507) Training | REGISTER FOR THE WORKSHOPSimilar to the Preventive Controls for Human Food regulation (21 CFR 117), there are two parts to the Animal Food rule: Current Good Manufacturing Practices (CGMPs) and Preventive Controls. Figure 2 provides more detail on the Subparts of the Regulation. Also, animal food covered by specific CGMP regulations must still comply with those regulations (specifically low-acid canned food and medicated feed).
Those who have taken a Preventive Controls Qualified Individual (PCQI) course will notice the remarkable similarity to the structure of the Human Food Rule. This is by design, for our animals are often a part of the family for whom we want to provide the highest level of quality and safety possible. That said, there is some overlap between the two regulations. For instance, when human food byproducts are diverted to use in pet food or animal feed, the human food CGMP rules apply to that food intended for use as animal food.
Subpart
Topic
A
General Provisions
B
Current Good Manufacturing Practice
C
Hazard Analysis and Risk-Based Preventive Controls
D
Withdrawal of Qualified Facility Redemption
E
Supply Chain Program
F
Requirements Applying to Records that Must Be Established and Maintained
Figure 2. Subparts of 21 CFR 507, Current Good Manufacturing Practice, Hazard Analysis, and Risk-based Preventive Controls for Food for Animals.
What Does this Regulation Mean for the Pet Food Industry?
Large companies that produce commercially available pet foods available in grocery stores and big box retailers (such as Pedigree, Iams, Nutro, Purina, etc.) are typically already compliant to a voluntary GFSI-approved food safety scheme (FSSC 22000, SQF, etc.). These companies already have most necessary processes in place to be compliant. There may be adjustments related to terminology, documentation, records and hazard analysis expansions to include mention of Preventive Controls. However, most of the work has been completed already and only clarifications, in most instances, should be required.
However, there are many small “mom-and-pop” type establishments making niche pet food with high-quality, organic ingredients that may not have much knowledge about this regulation. These types of manufacturers want to make the best, safest, highest quality product they possibly can, but without knowledge and education, they may not know the questions to ask to point them in the right direction. When an inspector arrives and asks to see the written hazard analysis, even a high-quality niche processor may end up with the deer-in-the-headlights stare if they do not understand the question. This regulation has the potential to significantly impact their business, but in a small business most folks wear many hats, and it is not always possible to just jet away for a few days to attend a specialized training class.
It was indicated during our Lead Trainer course that FDA is developing a clear proactive approach to their inspections related to this rule. Our Lead Trainer courses also emphasized that the inspectors’ focus will be on the reasonably foreseeable hazards and potential hazards to ensure that each is in control. Control can be achieved through a Preventive Control or some other process, such as a GMP based pre-requisite program.
In order to be as effective and efficient as possible, it is critical that an organization understands the requirements of this regulation. For example, the Food Allergen Labeling and Consumer Protection Act (FALCPA) does not apply to food for animals, nor are there allergen provisions included in 21 CFR 507. Certainly there are specialty manufacturers that make special recipes for those pets that may have an allergy or sensitivity (i.e., wheat, rice, etc.); however, this is completely different than the required approach to allergens for the production of human food. The pet food or feed manufacturer is not bound by these restrictions. However, an uninformed processor may take it upon itself to redesign a label to include an allergen declaration assuming that requirements for human food also apply to them. This could result in a great expense for graphic design, reprinting, disposal and wasting of previously printed labels, and of course the time spent on the project.
Measuring effectiveness is one oft-overlooked part of a mature and robust food safety program. Even experienced managers sometimes overlook this crucial step, so it is unlikely that most people would be able to come up with the concept on their own without assistance. If a facility has a rule in place that people must wear gloves, but do not have the experience to train on proper glove use and the reasons gloves are worn, confusion and improper glove use will result. This results in the company wasting money on providing the gloves in the first place. No matter how conscientious a program is, it still requires effective programs for identifying and maintaining records. These provide evidence of compliance with the regulation. There must also be documents in place that define the operational requirements and explain how to demonstrate effectiveness.
Industry representatives also must fully understand how to distinguish between Current Good Manufacturing Practices (CGMPs), other prerequisite programs and preventive controls, and to determine where they fit into their operation and the regulatory framework. The logic used to determine whether a specified hazard is reasonably foreseeable is based on science, experience and education. There are different record-keeping requirements for different types of controls.
It is critical to the process to ensure that reliable resources are used to develop the foundation of the program. This is considered so important that the PCQI Preventive Control for Animal Food material references examples of credible resources in each chapter. Examples of these include trade associations, universities, industry-focused events, relevant informational emails and webinars. We have experienced first-hand that expanding a professional network using these types of resources increases the rate of attrition for knowledge when a sink-or-swim situation is presented.
Keep in mind that an operation must take an active role in defining, implementing and maintaining its food safety program. It is usually recommended that a consultant knowledgeable in your food sector be engaged to assist. However, the word of the day is “assist”. If the consultant writes a turnkey program, then whose program is it? And better yet, where are they going to be when you are in an audit and can’t explain (justify) what is stated in the program?
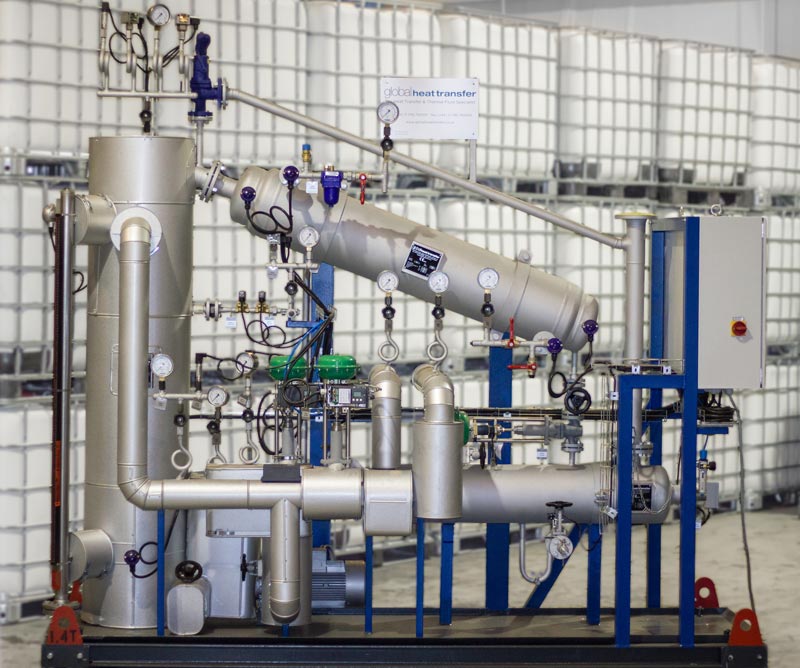
It is critical that the heat transfer fluids (HTFs) used in the manufacturing sector are used appropriately and managed safely. Food-grade HTFs are highly refined petroleum mineral oils that are non-toxic, non-irritating and lack an odor. If a food grade HTF has been certified for use in food processing, it carries a HT-1 certificate (e.g., Globaltherm FG). Food-grade HTFs are commonly referred to as being non-fouling, which means that as they thermally degrade, they produce small carbon particles that are suspended in the HTF. This means the carbon formations are less sticky, thereby reducing the extent of adhesion to the internal surfaces of a HTF system. A recent report analyzed the test reports from HTF systems and showed carbon residue was lower for food-grade HTFs than mineral-based HTFs.1 This demonstrates the non-fouling nature of food-grade HTFs. The report recommended the independent assessment of HTFs to ensure food manufacturers and producers are using food-grade HTFs.
The HTF sector was estimated to be worth $2.8 billion in 2015 and is projected to grow by 6.8% over the next 5 years.2 Heat transfer refers to the transfer of thermal energy, and fluids are used to transfer heat energy from a heat source to processing equipment where heat is needed. This is a basic requirement in a wide variety of industrial processes, including the processing of foodstuffs such as crackers or any foods that come in a packet.
Food-grade HTFs are non-toxic, odorless and appear transparent like water, but they clearly should not be confused with water.1 Indeed, a food-grade HTF is a highly refined petroleum mineral oil and consists of a complex combination of hydrocarbons obtained from the intensive treatment of a petroleum fraction with sulphuric acid and oleum, by hydrogenation or by a combination of hydrogenation and acid treatment.
Food-grade HTFs are the most likely HTF to be used in the processing of foods provided they are judged to be safe for incidental contact with food. This certification is governed by two well-known bodies—the NSF and InS. In the case of the NSF, the components comprising a fluid are assessed for safety by a toxicologist and, if deemed safe, are awarded a HT-1 certification and can be used for incidental contact. In some cases the use of so-called food-grade HTFs is stipulated by insurers and food retailers, and certain manufacturers will be routinely audited to ensure that an appropriate HTF is being used in the processing of food. Another advantage of a HT-1 certification is that it is associated with fewer handling complaints than other fluids.
In the case of the United Kingdom, Global Heat Transfer, part of the Global Group of Companies, estimates that around 20% of all HTF systems are involved in the processing of food. The use of a food-grade HTF is recommended, but its use is not regulated. However, HTF leaks do occasionally occur. In 1998 more than 490,000 pounds of smoked boneless hams were recalled by Smithfield Foods after several customers reported a “bad taste” and “burning in their throat”, which lasted up to three hours.3 The cause was incidental contact with a non-food grade gear lubricant.
In the context of food processing, good manufacturing practice (GMP) prerequisites combined with the application of risk-based Hazard Analysis Critical Control Points (HACCP) according to Codex Alimentarius principles alongside first-, second- and third-party quality audits in the supply chain are used to ensure food is managed safely both during processing and when being distributed to the consumer. In addition, industrial insurers work closely with manufacturers to ensure commercial operations are adequately insured and as part of this process, may stipulate the use of a food-grade HTF and how it should be maintained.
There is no specific legislation to ensure that food grade HTFs are used in the processing of food, so it is the responsibility of the food business owner to ensure food safety throughout the supply chain and more pointedly to design plant, equipment and premises such as to protect against the accumulation of dirt, contact with toxic materials and the shedding of particles into food.
However, as outlined in the Smithfield Foods case, there is the potential for the food to come into contact with an HTF during processing. It is important to consider a few scenarios where a food may be contaminated with an HTF.
Scenario 1. The HTF may be managed by the manufacturer according to HACCP if directly involved in the processing of a product or by GMP prerequisites if the HTF forms part of the facility and services to the production line. Either system will not allow any amount of HTF to be present in food. In the event of incidental contact with food, the manufacturer may choose to dispose of all food. In this scenario, a mineral-based HTF may be used rather than a food-grade HTF.
Scenario 2. The HTF is managed according to the stipulations from the retailer. In this scenario the retailer may stipulate that a food-grade HTF is used. The HTF would be checked during auditing. However, this would be a paper-based audit, and so the HTF would never be physically sampled and analyzed.
Scenario 3. The insurer stipulates the use if a food-grade HTF. Like scenario 2, adoption would be assessed during audits of a facility and paper-based checks would be conducted. Like scenario 2, however, the HTF would never be physically sampled and analyzed. In this case the insurer may be more concerned with the safety of the system and may be more interested in the sampling reports and parameters, such as annual sampling frequency and flash point temperature of the HTF.
The gap highlighted in scenarios 2 and 3 is that a food-grade HTF would never actually be physically analyzed onsite. HTF sampling and chemical analysis is quick and easy to conduct, and can be conducted by professional companies without interrupting production.
This article makes the case for checking that non-fouling, NSF or InS certified food-grade heat transfer fluids are being used in food production. This can be achieved using independent sampling that can be conducted on-site as requested and shared with all stakeholders including the insurer, to show the HTF is being managed and that the HTF system is safe; the retailer, to demonstrate that an appropriate food-grade HTF is being used during the processing of food; and external auditors, to demonstrate that production is consumer safe.
References
Wright CI, Bembridge T, Picot E, Premel J, Food processing: the use of non-fouling food grade heat transfer fluids. Applied Thermal Engineering 2015: 84; 94-103.
Food production facilities are facing greater scrutiny from both the public and the government to provide safe foods. FSMA is being rolled out now, with new regulations in place for large corporations, and compliance deadlines for small businesses coming up quickly. Coverage of food recalls is growing in the era of social media. Large fines and legal prosecution for food safety issues is becoming more commonplace. Improved detection methods are finding more organisms than ever before. Technologies such as pulsed-field gel electrophoresis (PFGE) can be used to track organisms back to their source. PFGE essentially codes the DNA fingerprint of an organism. Using this technology, bacterial isolates can be recovered and compared between sick people, contaminated food, and the places where food is produced. Using the national laboratory network PulseNet, foodborne illness cases can be tracked back to the production facility or field where the contamination originated. With these newer technologies, it has been shown that some pathogens keep “coming back” to cause new outbreaks. In reality, it’s not that the same strain of microorganism came back, it’s that it was never fully eradicated from the facility in the first place. Advances in environmental monitoring and microbial sampling have brought to light the shortcomings of sanitation methods being used within the food industry. In order to keep up with the advances in environmental monitoring, sanitation programs must also evolve to mitigate the increased liability that FSMA is creating for food manufacturers.
Paul Lorcheim of ClorDiSys Solutions will be speaking on a panel of Listeria Detection & Control during the 2016 Food Safety Consortium, December 8 | LEARN MOREPersistent Bacteria
Bacteria and other microorganisms are able to survive long periods of time and become reintroduced to production facilities in a variety of ways. Sometimes construction or renovation within the facility causes contamination. In 2008, Malt-O-Meal recalled its unsweetened Puffed Rice and Puffed Wheat cereals after finding Salmonella Agona during routine testing of its production plant. Further testing confirmed that the Salmonella Agona found had the same PFGE pattern as an outbreak originating from the same facility 10 years earlier in 1998. This dormant period is one of the longest witnessed within the food industry. The Salmonella was found to be originating from the cement floor, which had been sealed over rather than fully eliminated. This strategy worked well until the contamination was forgotten and a renovation project required drilling into the floor. The construction agitated and released the pathogen back into the production area and eventually contaminated the cereal product. While accidental, the new food safety landscape looks to treat such recurring contaminations with harsher penalties.
One of the most discussed and documented cases of recurring contamination involves ConAgra’s Peter Pan peanut butter brand. In 2006 and 2007, batches of Peter Pan peanut butter produced in Sylvester, GA were contaminated with Salmonella and shipped out and sold to consumers nationwide. The resulting outbreak caused more than 700 reported cases of Salmonellosis with many more going unreported. Microbial sampling determined that the 2006 contamination resulted from the same strain of Salmonella Tennessee that was found in the plant and its finished product in 2004. While possible sources of the contamination were identified in 2004, the corrective actions were not all completed before the 2006–2007 outbreak occurred. Because of the circumstances surrounding the incomplete corrective actions, ConAgra was held liable for the contamination and outbreak. A settlement was reached in 2015, resulting in a guilty plea to charges of “the introduction into interstate commerce of adulterated food” and a $11.2 million penalty. The penalty included an $8 million criminal fine, which was the largest ever paid in a food safety case. While the problems at the Sylvester plant were more than just insufficient contamination control, the inability to fully eliminate Salmonella Tennessee from the facility after the 2004 outbreak directly led to the problems encountered in 2006 and beyond.
Many times, bacteria are able to survive simply because of limitations of the cleaning method utilized by the sanitation program. In order for any sanitation/decontamination method to work, every organism must be contacted by the chemical/agent, for the proper amount of time and at the correct concentration by an agent effective against that organism. Achieving those requirements is difficult for some sanitation methods and impossible for others. Common sanitation methods include steam, isopropyl alcohol, quaternary ammonium compounds, peracetic acids, bleach and ozone, all of which have a limited ability to reach all surfaces within a space, and some are incapable of killing all microorganisms.
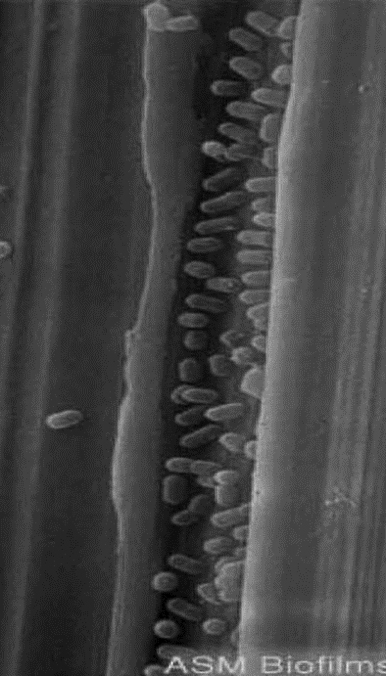
Figure 1. Bacteria in a 10-micron wide scratch.
Liquids, fogs and mists all have difficulty achieving an even distribution throughout the area, with surfaces closer or easier to reach (i.e., the top or front of an item), receiving a higher dosage than surfaces further away or in hard-to-reach areas. Such hard-to-reach areas for common sanitation methods include the bottom, back or insides of items and equipment that don’t receive a “direct hit” from the decontaminant. Liquids, fogs and mists land on and stick to surfaces, which makes it harder for them to reach locations outside the line of sight from where they are injected or sprayed. Hard-to-reach areas also include ceilings, the tops of overhead piping lines, HVAC vents, cooling coils and other surfaces that are located at greater heights than the liquids, fogs and mists can reach due to gravitational effects on the heavy liquid and vapor molecules.
Another common but extreme hard-to-reach area includes any cracks and crevices within a facility. Although crevices are to be avoided within production facilities (and should be repaired if found), it is impossible to guarantee that there are no cracks or crevices within the production area at all. Liquid disinfectants and sterilant methods deal with surface tension, which prevents them from reaching deep into cracks. Vapor, mist and fog particles tend to clump together due to strong hydrogen bonding between molecules, which often leave them too large to fit into crevices. Figure 1 shows bacteria found in a scratch in a stainless steel surface after it had been wiped down with a liquid sterilant. The liquid sterilant was unable to reach into the scratch and kill/remove the bacteria. The bacteria were protected by the crevice created by the scratch, giving them a safe harbor location where they could replicate and potentially exit in the future to contaminate product itself.
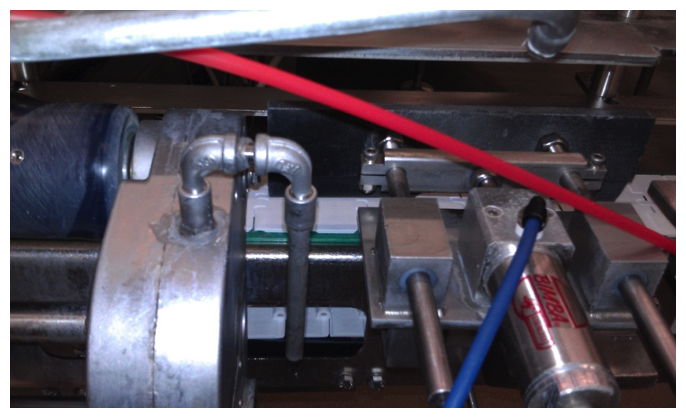
Figure 2. Processing machinery
Processing equipment and machinery in general contain many hard-to-reach areas, which challenge the routine cleaning process. In sanitation, “hard to reach” is synonymous with “hard to clean”. Figure 2 shows processing equipment from an ice cream manufacturing facility. Processing equipment cannot be manufactured to eliminate all hard-to-clean areas. As such, even with all the sanitary design considerations possible, it is impossible to have equipment that does not contain any hard-to-clean areas. While sanitary design is essential, additional steps must be taken to further reduce the possibility of contamination and the risk that comes along with it. This means that in order to improve one’s contamination control and risk management programs, improvements must also be made to the sanitation program and the methods of cleaning and decontamination used.
Chlorine Dioxide Gas
Food safety attorney Shawn K. Stevens recently wrote that “given the risk created by the FDA’s war on pathogens, food companies should invest in technologies to better control pathogens in the food processing environments.”1 One method that is able to overcome the inherent difficulties of reaching all pathogens within a food processing environment is chlorine dioxide gas (ClO2 gas). ClO2 gas is a proven sterilant capable of eliminating all viruses, bacteria, fungi, and spores. As a true gas, ClO2 gas follows the natural gas laws, which state that it fills the space it is contained within evenly and completely. The chlorine dioxide molecule is smaller than the smallest viruses and bacteria. Combined, this means that ClO2 gas is able to contact all surfaces within a space and penetrate into cracks further than pathogens can, allowing for the complete decontamination of all microorganisms with the space. It also does not leave residues, making it safe for the treatment of food contact surfaces. It has been used to decontaminate a growing number of food facilities for both contamination response and contamination prevention in order to ensure sterility after renovations, equipment installations and routine plant shutdowns.
Conclusion
“If food companies do not take extraordinary measures to identify Lm in their facilities, perform a comprehensive investigation to find the root cause or source, and then destroy and eliminate it completely, the pathogen will likely persist and, over time, intermittently contaminate their finished products,” wrote Stevens.1 Environmental monitoring and sampling programs have been improved in terms of both technology and technique to better achieve the goal of identifying Lm or other pathogens within a food production environment. The FDA will be aggressive in its environmental monitoring and sampling under the food safety guidelines required by FSMA. Food production facilities will be closely monitored and tracked using PulseNet, with contaminated product being traced back to their source. Recurring contamination by a persistent pathogen will be viewed more severely. While there are many reasons that pathogens can persist within a food manufacturing environment, insufficient cleaning and decontamination is the most common. Traditional cleaning methods are incapable of reaching all surfaces and crevices within a space. In order to eliminate the risk of pathogens re-contaminating a facility, the pathogens need to be fully eliminated from their source and harbor locations. ClO2 gas is a method capable of delivering guaranteed elimination of all pathogens to maintain a pathogen-free environment. With the new era of food safety upon us, ensuring a clean food production environment is more important than ever, and ClO2 gas is uniquely situated to help reduce the risk and liability provided by both the government and the public.
In the summer of 2015, multiple ice cream manufacturers were affected by Listeria monocytogenes contamination. Part two of this article will detail one such company that utilized ClO2 gas to eliminate Listeria from its facility.
There are several ways in which pathogens can enter a food processing facility. Once inside, pathogens are either temporary visitors that are removed using cleaning and disinfection methods, or they can persist in sites such the floor or drains and require a more intense remediation process. As food processors take on the responsibility to prevent product adulteration in facilities, setting up and maintaining an environmental monitoring program (EMP) is critical. An effective EMP helps a company manage and potentially reduce operational, regulatory and branding reputation risks.
Establishing an EMP begins with identifying and documenting potential pathogen sources in all physical areas (including raw materials, storage and shipping areas) and cross-contamination vectors (employees, equipment, pests, etc.). These areas and vectors should be surveyed, controlled and when possible, eliminated. Implementing effective controls, including microbiological sampling of high-risk areas, should be part of the program. Sampling for pathogens or indicator microorganisms in food contact areas during production is also important. Additionally, the EMP elevates the awareness of what is happening in the plant environment and helps companies measure the efficiency of their pathogen-prevention program—for example, it is not only critical to test for pathogens, but also for the overall effectiveness of cleaning and sanitizing procedures. Both procedures are necessary and must be properly executed to reduce microorganisms to safe levels. The goal of a cleaning process is to remove completely food and other types of soil from a surface. Since soils vary widely in composition, no single detergent is capable of removing all types. In general, acid cleaners dissolve alkaline soils (minerals) and alkaline cleaners dissolve acid soils and food wastes. It is for this reason that the employees involved must understand the nature of the soil to be removed before selecting a detergent or a cleaning regime. The cleaner must also match with the water properties and be compatible (i.e., not corrosive) with the surface characteristics on which it will be applied. However, not only the correct choice of agent is necessary for an optimal result; it should be coupled with a mechanical action, an appropriated contact time and correct operating temperature. As the combination of these parameters is characteristic to each process, it becomes essential to verify effectiveness through sampling. Finally, cleaning is closely related to sanitation, because it can’t be sanitized what hasn’t been previously cleaned.
“Not Your Grandfather’s Environmental Monitoring Program Anymore”: Learn more about this important topic at the 2016 Food Safety Consortium | EVENT WEBSITE
The Association of Official Analytical Chemists defines sanitizing for food product contact surfaces as a process that reduces the contamination level by 99.999% (5 logs). Sanitation may be achieved using either heat (thermal treatment) or chemicals. Hot water sanitizing is commonly used where immersing the contact surfaces is practical (e.g., small parts, utensils). Hot water sanitizing is effective only when appropriate temperatures can be maintained for the appropriate period of time. For example, depending on the application, sanitation may be achieved by immersing parts or utensils in water at 770 C to 850 C for 45 seconds to five minutes. The advantages of this method include easy application, availability, effective for a broad range of microorganisms, non-corrosive, and it penetrates cracks and crevices. However, the process is relatively slow, can contribute to high energy costs, may contribute to the formation of biofilms and may shorten the life of certain equipment parts (e.g., seals and gaskets). Furthermore, fungal spores can survive this treatment.
Regarding chemicals, there is no perfect chemical sanitizer. Performance depends on sanitizer concentration (too low or too high is ineffective), contact exposure time, temperature of the sanitizing solution (generally, 210 C to 380 C is considered optimal), pH of the water solution (each sanitizer has an optimal pH), water hardness, and surface cleanliness. Some chemical sanitizers, such as chlorine, react with food and soil, becoming less effective on surfaces that have not been properly cleaned.
The effectiveness of a plant’s sanitation practices must be verified to ensure that the production equipment and environment are sanitary. Operators employ several methods of verification, including physical and visual inspection, as part of ongoing environmental hygiene monitoring programs. Portable ATP bioluminescence systems are widely used to obtain immediate results about the sanitary or unsanitary condition of food plant surfaces. ATP results should be followed up with more in-depth confirmation testing, such as indirect indicator tests and pathogen-specific tests. Indirect indicator tests are based on non-pathogenic microorganisms (i.e., coliform, fecal coliforms or total counts) that may be naturally present in food or in the same environment as a pathogen. These indicator organisms are used to assess the overall sanitation or environmental condition that may indicate the presence of pathogens. The principal advantages of using indicator organisms in an EMP include:
Detection techniques are less expensive compared to those used for pathogens
Indicator microorganisms are present in high numbers and a baseline can be easily established
Indicator microorganisms are a valid representative of pathogens of concern since they survive under similar physical, chemical and nutrient conditions as the pathogen
However, indicator organisms are not a substitute for pathogen testing. A positive result indicates possible contamination and a risk of foodborne disease. It is recommended that samples be taken immediately before production starts, just after cleaning and sanitation have been completed when information regarding cleaning and sanitation are required. However, when sampling is conducted on surfaces previously exposed to chemical germicide treatment, appropriate neutralizers must be incorporated into the medium to preserve viability of the microbial cells.
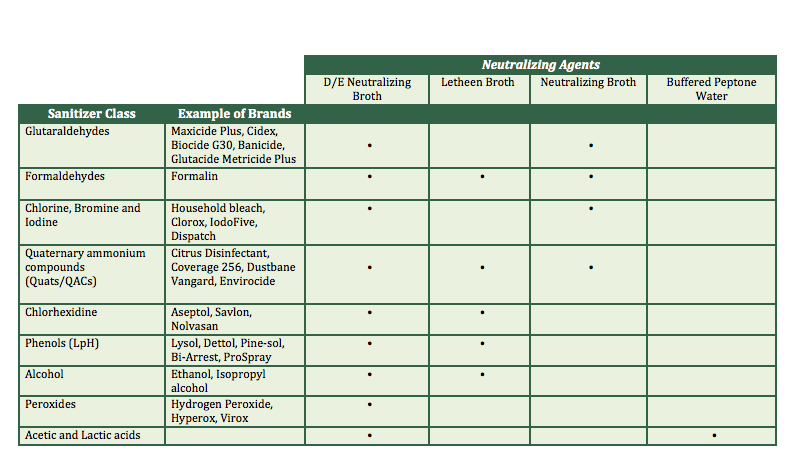
Neutralizers recommended for food plant monitoring include Dey-Engley neutralizing broth (DE), neutralizing buffer (NE), Buffered peptone water (BPW) and Letheen broth (LT) (see Table I). Most of these are incorporated into a support such as a sponge, swab or chiffon to neutralize the residues of cleaning agents and sanitizers that may be picked up during swabbing. The product should be selected based on the surface, the type of cleaning agents and the type of testing (qualitative or quantitative).
Table I. Neutralizing agents
It is critical to verify that the chosen neutralizer has an efficient action against the used sanitizers. Table I show the most effective equivalence among the cleaning agents and the most common neutralizers.
For instance, if a quantitative method is to be used, it is very important to consider a neutralizing agent, such as the neutralizing buffer, that doesn’t support the bacterial growth.
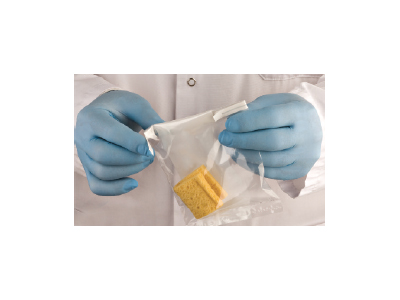
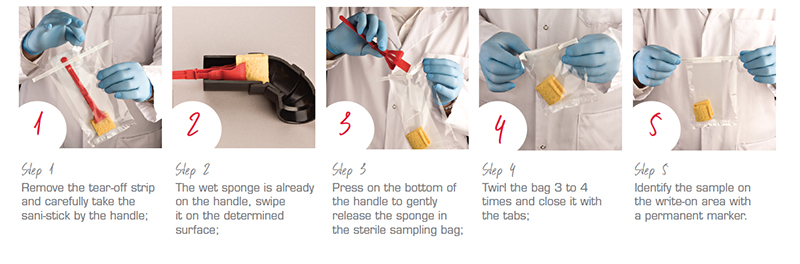
Finally the sponge is a very popular choice due to its versatility. Sponges are used for sampling equipment surfaces, floors, walls, work benches and even carcasses. They enable the sampling of large surfaces and the detection of lower levels of contamination at a lower cost of operation.
The versatility of sponges make them a popular choice for environmental sampling. Image courtesy of Labplas.
To summarize, environmental sampling is an important tool to verify sources of contamination and adequacy of sanitation process, helping to refine the frequency and intensity of cleaning and sanitation, identify hot spots, validate food safety programs, and provide an early warning of issues that may require corrective action. Over all, it provides the assurance that products being manufactured are made under sanitary conditions.
Allergenic foods are a serious safety risk. While harmless to most of the consumer population, they are harmful and even life threatening to some, causing serious medical reactions, such as anaphylactic shock, when foods with the allergenic protein are consumed. Scientific research and legislation have helped us understand a great deal about managing these food allergens in manufacturing. Yet so much more needs to be done in making these risks safer for the growing allergic population. In 2013, the CDC reported that food allergies among children increased by half from 1997 to 2011. As these numbers continue to rise for children and adults alike, what are the best practices for food manufacturers to include in managing food allergens? Here’s what you need to know.
Evan Rosen is participating as a panelist in the session “Rubber Meets the Road: Practical Compliance with FSMA and Preventive Controls” at the 2016 Food Safety Consortium. The session will be moderated by Rajan Gupta and Dana Johnson Downing of TraceGains | LEARN MOREResearch and Development for Allergen Programs
Thorough development and foresight are essential for any food manufacturer to succeed when implementing an allergen program in its processing. It is wise for food manufacturers to select the individuals in their company who are a good fit to lead the allergen program. When developing your program, create an “allergen map” to understand where allergenic ingredients are located in your plant and how they travel while products are processed.
The R&D stage is the optimal time to plan every step of the allergen management process—from supplier sourcing to cross contact in processing, to labeling and every step in between—before the risks are actually encountered. This is in line with the new preventive controls approach to be taken with FSMA’s Food Safety Plan model.
Purchasing, Labeling and Storing Ingredients
When purchasing ingredients from suppliers, your supply sources should be just as stringent about allergen management as you are in order to reduce liability. Require your suppliers to have an allergen map of their own and lettered documentation declaring that the items you are purchasing are free from contact with food allergens. The FDA food label law currently recognizes the top eight food allergens as:
Peanuts,Tree nuts—including almonds, walnuts and hazelnuts, among others
Milk (not to be confused with lactose intolerance)
Also, be mindful of allergens that apply to the country of export, such as Sesame Seeds, Sulfites and Mustard Seed in Canada.
When receiving and storing supplier ingredients, check the labeled contents for any updates and tag the units that contain allergens so they can be easily identified and stored separately. A pictorial system is very effective. Ensure that each unit is tightly sealed, as even slight amounts of leaked allergens can pose recalls and elevated risks to your consumers.
Processing and Cleaning Cross-Contamination
Human error is only one factor that predisposes risk of cross-contact; production timing, processing lines, facility traffic, protein structure (e.g. powder, liquid, paste) and even the type of equipment used can be a game changer when it comes to the proper handling of allergens. In order to prevent allergen cross contact, scheduling long lines of products with common allergens is recommended to minimize changeovers. Dedicate unique tools, utensils and equipment that will handle the allergen if possible, as every piece contacting an allergen must be washed before handling allergen-free processing.
Assign plant employees to specific locations to avoid risk of cross-contact travel—color coding uniforms helps a great deal in managing this concept. Manufacturing equipment that is designed for easy cleaning is also ideal. For cleaning procedure of cross-contact removal, wet cleaning methods are most effective followed by dry methods. These procedures should be validated using a recognized protein-specific test method such as lateral flow or ELISA. When flushing, be sure to keep the flushed material isolated from all allergen-free areas. Careful separation and mindfulness is key to a successful allergen program.
Staff Training and Education
In order for any allergen program to be effective, all plant, production staff, contractors and visitors must be aware of the importance of it and understand the impact it has on consumers. Incorporating different learning methods helps to communicate this to them. Occasional testing and validation of applying this knowledge ensures the integrity of your allergy-free claims and establishes trust. Passion and commitment also play a vital role in achieving success in your program as a whole.
From purchasing ingredients to staff education and cross-contact prevention, one can see that plenty of work and forethought goes into having an allergen management program. With these best practices in place, food manufacturers can be well prepared for the increasing demand of allergen safe products for consumers across national and international markets.
This website uses cookies so that we can provide you with the best user experience possible. Cookie information is stored in your browser and performs functions such as recognising you when you return to our website and helping our team to understand which sections of the website you find most interesting and useful.
Strictly Necessary Cookies
Strictly Necessary Cookies should be enabled at all times so that we can save your preferences for these cookie settings.
We use tracking pixels that set your arrival time at our website, this is used as part of our anti-spam and security measures. Disabling this tracking pixel would disable some of our security measures, and is therefore considered necessary for the safe operation of the website. This tracking pixel is cleared from your system when you delete files in your history.
We also use cookies to store your preferences regarding the setting of 3rd Party Cookies.
If you visit and/or use the FST Training Calendar, cookies are used to store your search terms, and keep track of which records you have seen already. Without these cookies, the Training Calendar would not work.
If you disable this cookie, we will not be able to save your preferences. This means that every time you visit this website you will need to enable or disable cookies again.
Cookie Policy
A browser cookie is a small piece of data that is stored on your device to help websites and mobile apps remember things about you. Other technologies, including Web storage and identifiers associated with your device, may be used for similar purposes. In this policy, we say “cookies” to discuss all of these technologies.
Our Privacy Policy explains how we collect and use information from and about you when you use This website and certain other Innovative Publishing Co LLC services. This policy explains more about how we use cookies and your related choices.
How We Use Cookies
Data generated from cookies and other behavioral tracking technology is not made available to any outside parties, and is only used in the aggregate to make editorial decisions for the websites. Most browsers are initially set up to accept cookies, but you can reset your browser to refuse all cookies or to indicate when a cookie is being sent by visiting this Cookies Policy page. If your cookies are disabled in the browser, neither the tracking cookie nor the preference cookie is set, and you are in effect opted-out.
In other cases, our advertisers request to use third-party tracking to verify our ad delivery, or to remarket their products and/or services to you on other websites. You may opt-out of these tracking pixels by adjusting the Do Not Track settings in your browser, or by visiting the Network Advertising Initiative Opt Out page.
You have control over whether, how, and when cookies and other tracking technologies are installed on your devices. Although each browser is different, most browsers enable their users to access and edit their cookie preferences in their browser settings. The rejection or disabling of some cookies may impact certain features of the site or to cause some of the website’s services not to function properly.
Individuals may opt-out of 3rd Party Cookies used on IPC websites by adjusting your cookie preferences through this Cookie Preferences tool, or by setting web browser settings to refuse cookies and similar tracking mechanisms. Please note that web browsers operate using different identifiers. As such, you must adjust your settings in each web browser and for each computer or device on which you would like to opt-out on. Further, if you simply delete your cookies, you will need to remove cookies from your device after every visit to the websites. You may download a browser plugin that will help you maintain your opt-out choices by visiting www.aboutads.info/pmc. You may block cookies entirely by disabling cookie use in your browser or by setting your browser to ask for your permission before setting a cookie. Blocking cookies entirely may cause some websites to work incorrectly or less effectively.
The use of online tracking mechanisms by third parties is subject to those third parties’ own privacy policies, and not this Policy. If you prefer to prevent third parties from setting and accessing cookies on your computer, you may set your browser to block all cookies. Additionally, you may remove yourself from the targeted advertising of companies within the Network Advertising Initiative by opting out here, or of companies participating in the Digital Advertising Alliance program by opting out here.