Audit

The Multi-Step Process of Third-Party Accreditation

By Charles Breen
No Comments
Audit

The FSMA Third Party Accreditation (TPA) final rule was published in the Federal Register in final form on November 27, 2015. Although TPA is not limited to imported food, its primary use will most likely be for food imports. TPA offers foreign food facilities and food importers a way to show FDA that the items coming to the United States meet federal food safety requirements.

An acceptable audit by a certified auditor is the only way an importer can take advantage of another FDA program, the Voluntary Qualified Importer Program (VQIP), which offers expedited review and entry of food. If FDA deems it necessary, the agency can also require certified audits for the import of specific foods.

The TPA process requires a number of administrative steps by FDA and non-FDA entities before the first third-party inspection is made. The four major steps are:

  • FDA is responsible for officially recognizing accreditation bodies.
  • An officially recognized accreditation body will accredit third-party certification bodies.
  • The accredited third-party certification body will certify third-party auditors.
  • The certified auditors will conduct consultative and regulatory audits of food facilities.

If FDA does not find an applicant that it can officially recognize as an accreditation body within two years, it may directly accredit third-party certification bodies.

In order to recognize an accreditation body, FDA must review an applicant’s legal authority, competency, capacity, conflict-of-interest safeguards, quality assurance and record procedures. By using an already existing framework familiar to industry, accreditation bodies and certification bodies will be allowed to use documentation of their conformance with the International Organization for Standardization and the International Electrotechnical Commission (ISO/IEC) standards, supplemented if necessary, in meeting program requirements under this rule. An official recognition of an accreditation body is granted for up to five years.

FDA is authorized to recognize a foreign government/agency or a private third party as an accreditation body under TPA.

Recognized accreditation bodies under TPA will be required to:

  • Evaluate potential third-party certification bodies for accreditation, including observing representative samples of the prospective certification body’s work
  • Monitor performance of the third-party certification bodies it has accredited, including periodical on-site observations, and notifying the FDA of any change in, or withdrawal of, accreditations it has granted
  • Self-evaluate and correct any problems in their own performance
  • Submit monitoring and self-assessment reports and other notifications to the FDA
  • Maintain and provide the FDA access to records required to be kept under the program

Once accredited, third-party certification bodies under TPA are required to perform unannounced facility audits, and to notify the FDA if a condition is found that could cause or contribute to a serious risk to public health.

Employee learning, Huddle guide

Trends in Digital Learning

By Holly Mockus
No Comments
Employee learning, Huddle guide

The food industry is becoming increasingly fast-paced. Regulations are changing, the supply chain is becoming more transparent, and resources are harder to access. To meet the needs of an ever-changing industry, digital learning is becoming the go-to solution for training managers and frontline food handlers alike, as it can be done quickly and efficiently. Now that most people have smartphones and mobile devices, there are multiple ways to make learning accessible.

Employee learning
Image courtesy of Alchemy Systems

The “Mind of the Food Worker” study conducted by the Center for Research and Public Policy (CRPP) points out that food workers have developed a preference for digital training over traditional classroom or instructor-conducted training. There are many new approaches to learning, including web-based eLearning, kiosk, gamification/competition, social media, digital signage, and coordinated communication programs. Let’s take a closer look at each of these.

eLearning

eLearning is no longer about reading through a PowerPoint presentation or watching a pre-recorded video. The number of companies offering eLearning continues to increase, as do the topics, content and format of the content. In addition, eLearning carries the added benefit of being affordable. For many companies, saving on the cost of travel when an individual attends a workshop provides an attractive incentive.

The ability to learn at one’s own pace at the time and place of one’s choosing has special appeal for today’s learners. The availability of eLearning via mobile devices is meeting that desire. It can be seen everywhere—people glued to their mobile devices while waiting in line, taking a lunch break, or in the evenings on their own time. This is multitasking at its finest.

Kiosks

The ability to take a device to a quiet environment helps with concentration and efficiency in training. Kiosks can be set up in an area that is conducive to learning with no traffic, noise or other distractions and are popping up at workplaces more and more. Learners can come and go at their convenience. A learning lab set up in a manufacturing facility will pay for itself very quickly. Sending workers to the lab one at a time is much more cost effective than shutting down a line or area of the plant for group or classroom training.

Gamification

Gamification, the use of interactive tools in conjunction with learning, is a term being used more often in training industry vocabulary. For example, it can involve the addition of a word and a definition-matching exercise in conjunction with a training module to encourage learners to retain what they have just learned. It also makes the education process more fun—and it seems to be working.

Gone are the days of sitting through hours and hours of dry lectures or reading textbooks that simply do not resonate. This method has always been especially difficult for employees working in a food plant. Sitting in a warm darkened room listening to a droning presentation is an invitation to sleep. Gamification eliminates the droning, and requires attention and participation.

The Association for Psychological Science has confirmed that competition engages learners, drives retention, and leads to higher test scores. Got a boring topic for training?  Get your game on!  A great example of gamified learning that is readily available is Merriam-Webster’s Word of the Day. Sign up for free and receive a daily email with a new word, along with its pronunciation, definition(s), use and history. The email also links to several great games that provide word calisthenics for the brain.

Social Media

Leveraging social media helps to expand and continuously improve training programs. This mode of technology will ensure that every employee in a company has timely, consistent answers to questions. Using private company social media provides a safe environment for posting questions and answers while complementing a training program and filling any knowledge gaps. The CRPP study points out that 80% of workers regularly use public social media platforms such as Facebook and LinkedIn.

Companies can take full advantage of this familiarity with social media by providing an internal forum that encourages open discussion and group learning. This approach enables the workforce to engage in an interactive learning path that is continually up to date. Internal social media also encourages networking, which fosters a sense of camaraderie between individuals, along with company loyalty. One major food company that has used this approach has seen employee questions flourish from 3,000 entries in the first year to more than 15,000 the following year. What an incredible way to keep the workforce updated minute by minute with appropriate, relevant answers to their inquiries.

The Future of Technology, Compliance and Food Safety

By Jason Dea
No Comments

There is no question that we are in the midst of a unique time period in history. Technology is continuing to innovate at an increasingly rapid rate, which has led to drastic changes that affect nearly every corner of day-to-day life. From the way we find information to our food choices, technology is influencing our lives in new ways.

The Rise of the Internet

Mary Meeker, the venture capitalist who was dubbed the “Queen of the Internet” more than 15 years ago, has described the current Internet age as a period of reimagining. At the heart of this reimagining has been the rapid growth, maturity and adoption of the Internet and Internet-enabled technologies.

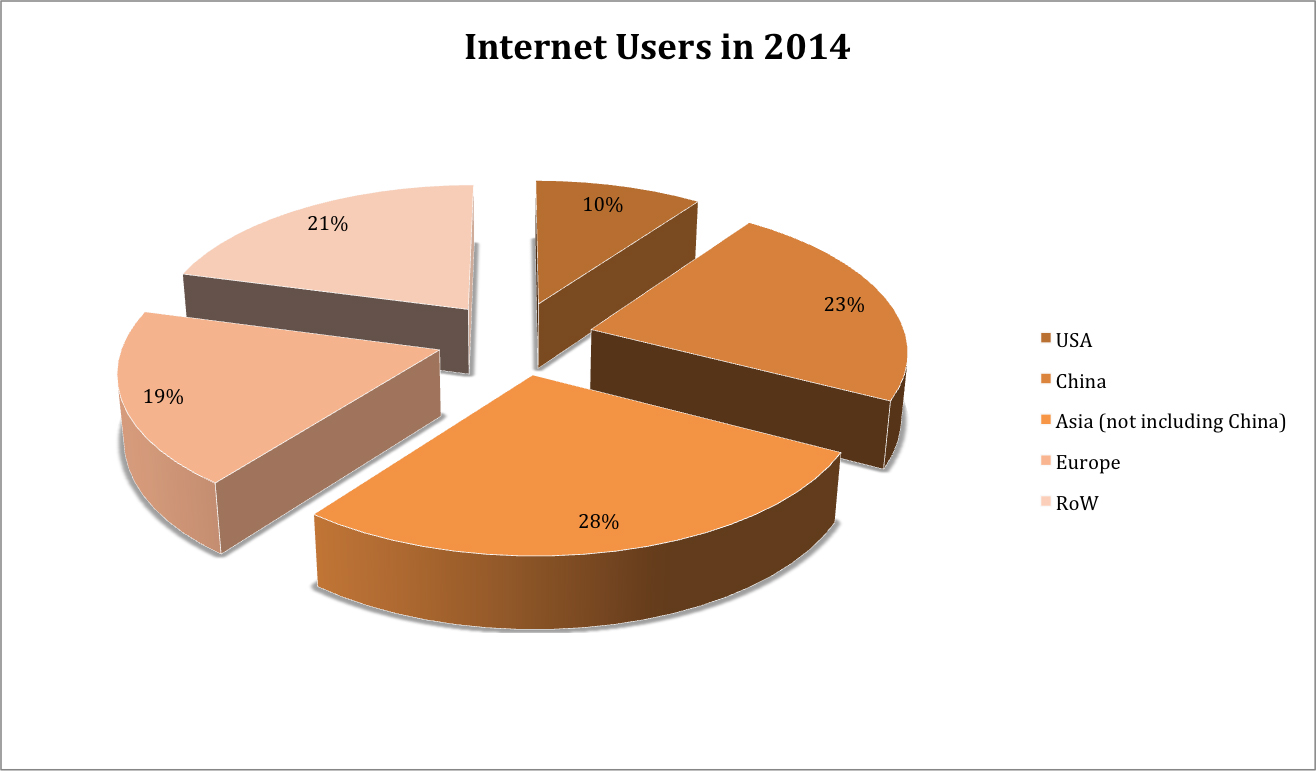
In her most recent 2015 research, Meeker published some fascinating statistics. The number of people online has ballooned more 80 times, from a user base of a mere 35 million in 1995 to a staggering 2.8 billion users in less than 20 years. This figure translates into nearly 40% of the total global population.

InternetUsers_2014
A breakdown of the 2.8 billion Internet users in 2014. This figure (39% global penetration) exploded from the approximately 35 million users in 1995. Source: Internet Trends 2015 – Code Conference

It hasn’t just been the volume of usage that has evolved radically. The nature by which those billions of users are signing online has also changed. It’s hard to believe that the original iPhone was released in 2007, less than 10 years ago. In that time, the mobile Internet has gone from a novelty to a necessity for many of us in our daily lives. This smartphone adoption has fueled Internet use and has drastically increased the ease with which consumers can get online.

Reimagining Communication and Compliance

The result of our new “always-on,” globally connected world (to borrow Meeker’s term) is a complete reimagining of communication. Consumers expect a velocity and volume of communication that the world has never before experienced. We now take for granted that we can reach friends, family and acquaintances anywhere in the world—at any time—in an instant. This has also drastically changed our expectations of business relationships.

Consumers in an ever-connected world have an expectation of availability and transparency of information from the brands with which they interact and the establishments they frequent. What this means for businesses is that customers expect to have a degree of access to business data that they’ve never asked for previously.

A tangible side effect of this desire for data transparency can be seen within the regulatory environment that organizations operate. Governments and regulatory bodies have increased their expectations of data access and availability over time, resulting in more stringent regulations across the board.

Research from Enhesa shows that the regulatory growth rate is nearly as staggering as Internet growth rates. According to the firm’s research, from 2007–2014 regulatory increases by region were as follows:

  • North America: +146%
  • Europe: +206%
  • Asia: +104%

Impact on Food Safety: Consumer Engagement and Regulatory Growth

One particular area of regulatory growth has occurred within the food and beverage sector. Arguably no product category has a more direct impact on consumers than food, as it literally fuels us each day. It’s no wonder that in an environment of increasing regulations and more empowered consumers that food quality and food safety are under increased scrutiny.

In today’s environment, it becomes much more challenging to brush aside product recalls and food safety incidents or bury these stories in specialized media. The latest news is not just a fleeting negative headline. In a worst-case scenario these incidents are viral, voracious and more shareable than ever before. From Listeria outbreaks to contaminated meat to questionable farming practices—when fueled by the Internet, the negative branding impact of these stories can be staggering. Consumers are paying attention and engaging with these stories—for example, during a Listeria or Salmonella outbreak, online searches for these terms significantly rise.

The rise of hyper-aware consumers has had a measurable impact. As a result, governments have been quick to respond and have beefed up existing regulations for the food and beverage sector via FSMA and GFSI.

FSMA

Are You Ready for the Produce Rule? You Just Might Be

By Marsha Madrigal
No Comments
FSMA

At last the new Produce Rule is out, issued on November 13, 2015.  For the first time in FDA history, the rule establishes a science-based minimum standard for growing, harvesting, packing and holding of fruits and vegetables grown for human consumption.  The rule can be found in Part 112 of the Code of Federal Regulations (CFR). It applies to both domestic and imported produce.

The new rule provides assurance that produce on the market is not adulterated under the Food, Drug, and Cosmetic Act.  It will accomplish this by establishing procedures, processes and practices that are known to minimize the risks of serious adverse health consequences or death to humans, and to prevent the introduction of known biological hazards into and or on produce.

The definition for a farm, covered under the rule, includes two kinds of farming operations, primary production farm and secondary activities farm. The primary production farm operates under one management, and the secondary activities farm is an operation. Where as the primary production farm owns, or jointly owns, a majority of interest in the secondary activities farm.

Food Safety Consortium
During the FDA Town Hall, an audience member asks about the Produce Rule and the work being done with Mexico. Watch the video

For the most part, the new mandated FDA Produce Rules, mirror what farmers, packers and others in the farm business have been doing all along.  For years now, produce buyers have required some kind of written guarantee from their suppliers such as a third-party audit certificate showing that the supplying farm or packing shed is complying with the farm food safety standards. Most farms and packing sheds have already undergone, if not one, but perhaps two or more third-party audits such as a Good Agricultural Practices (GAP) or, one of the Harmonized GAP audits, or a Good Manufacturing Practices (GMP) audit, or one of the Global Food Safety Initiative (GFSI) audits such as GlobalGAP, Safe Quality Foods (SQF) or BRC Global Standards (BRC).

This means that those covered under the Produce Rule for growing, harvesting, packing and holding of fruits and vegetables grown for human consumption and have received a third-party audit should have no trouble achieving compliance with the new Produce Rule.

The above-mentioned third-party standards cover most aspects of the key requirements of the Produce Rule regarding agricultural water, biological soil amendments, domesticated and wild animals, worker training, health and hygiene, and equipment, tools, and buildings.

However, some key requirements of the new rule not noted in existing third-party standards include:

  • Water testing of untreated water, sample collection and survey creation for agricultural water.
  • Microbial standard limits for detectable amounts of microorganisms to include Listeria monocytogenes, Salmonella species, and E. coli 0157:H7 for the treatment process of soil amendments, including manure.
  • The final Produce Rule includes requirements to help prevent the contamination of sprouts. For example, requires testing of spent sprout irrigation water for pathogens and requires environmental monitoring for Listeria. Documentation or letters from seed and/or bean supplier for the prior treatment of seed and beans are acceptable.
  • The requirements of Domesticated and Wild Animals relies more on monitoring and assessing conditions during growing season. If you find evidence of potential contamination like animal excreta, you must take action and evaluate whether produce can be harvested or if there is a likelihood of contamination. The produce must not be harvested.

This rule does not apply to:

  • Farms that have an average annual value of produce sold during the previous three year period of $25,000/yea
  • Produce for personal or on-the farm consumption
  • If the produce is on the list of “rarely consumed raw commodities” such as sweet potatoes and
  • A food grain such as wheat or oats

The rule provides also for exemptions:

  • Produce that will receive commercial processing (kill-step) to reduce microorganisms of public health concerns.
  • Provides a qualified exemption and modification requirement for farms that meet certain requirements based on monetary value and direct sales to qualified end users such as consumers or restaurants. The farm must also meet associated modified requirements like establishing and maintaining certain documentation.

Under certain conditions the FDA may withdraw a farm’s qualified exemption.

The rule focuses on sources of produce contamination found in the past: Agricultural water, biological soil amendments, domesticated and wild animals, worker training, health and hygiene, and equipment, tools and buildings.

This rule and others under FSMA such as Preventive Controls for Human Food, Preventive Controls for Animal Food, and the Foreign Supplier Verification Program are a long overdue yet great achievement for FDA. The agency now shifts its gear into focusing on preventing food safety problems instead of reacting to food safety outbreaks.

FDA estimates that about 348,000 illnesses per year will be prevented by the implementation of this rule.

The compliance dates for the new rule are staggered and based on business size.

Resources

  1. Produce Rule: Standards for the Growing, Harvesting, Packing, and Holding of Produce for Human Consumption
  2. FSMA Webinar Series: Final Rules for Produce Safety, Foreign Supplier Verification Program (FSVP), and Third Party Auditors

Top 10 Tips for Creating a Sustained Food Safety Culture

By Holly Mockus
5 Comments

After much anticipation, FDA has finally published the FSMA final rules. If you’ve had time to dig into the details, you most likely noted the new initiative that requires companies to measure food safety culture. The industry is also seeing SQF, BRC and other GFSI audit schemes ramping up discussions around measuring food safety culture. However, FDA and GFSI audits aside, how do you create a culture for sustained compliance with this initiative? Follow these 10 tips to ensure your food safety culture is constant and in line with the new requirements

Photo credit: Dennis Burnett for Alchemy Systems
Set clear expectations for employees across the board. Photo credit: Dennis Burnett for Alchemy Systems

1: Create a solid foundation of programs, procedures and policies

Have a preset annual schedule for review and update of all programs, procedures and policies. Don’t let the schedule slide because there are competing priorities. A small pebble is all it takes to start ripple effect in the company, making it difficult to recover.

2: Set clear expectations, driven from the top down

Everyone should follow the rules and guidelines—from visitors to the CEO to the plant manager to the hourly employee. A “no exceptions” policy will drive a culture that is sustainable and drive a “this-is-just-how-we-do-things” mindset.

3: Use record keeping to ensure that food safety culture is well documented and data-driven

Collect the data that is measureable and non-subjective to help drive continuous improvement. If you collect it, you must do something with it. Good documentation is imperative to proving you did what you said you were going to do, especially in the event of an audit. Be stringent in training, and review all documentation before it hits the file cabinet to ensure it is accurate and appropriate.

4: Implement a robust continuous improvement process

Forward momentum through a continuous improvement process cannot be achieved unless management nurtures the program. If you are not continuously improving, you are falling behind.

5: Have a 360-degree approach to employee engagement with 24/7 awareness and communication

Top-down communication is critical to highlighting the priorities and needs of an organization and will not be effective unless an organized program is in place. Organizations that are not making the necessary pivots to communicate with the multiple generations within their workplace today will struggle to sustain change.

6: Foster an atmosphere of mutual respect

Treat people as you would like to be treated, turn the other cheek, etc. There may be lots of adages you quote, but which one best describes your facility and the relationships with management and peers on a daily basis?

7: Be sure employees have consumer awareness for the products they produce

Do your employees know who the end consumer is of the product that they are producing every day?  Does your culture include a review of consumer complaints and customer complaints with your frontline workers?  Listening in to a call center is a very powerful way to help employees understand what affects consumers and how their job is critical to avoiding a food safety or quality issue.

8: Create accountability across the board

Hold folks who do not support the culture in which you are striving to develop or maintain accountable, regardless of their position or stature.

9: Provide positive reinforcement. It’s the best motivator

Work to catch people doing things right and make a big fuss when you do. Positive reinforcement for a job well done is the most powerful motivator. It helps keep every team member on board with food safety commitments.

10: Celebrate often

We spend too much time at work not to celebrate all the good things that are accomplished. Whether it’s a cake and recognition for those that served in the armed forces on Veterans Day or a successful launch of a new product—celebrations are a great way to recognize and reinforce your employees’ hard work. Identifying and correcting mistakes should also be celebrated; they are fertile ground for making changes and provide great nutrients for continuous improvement.

Prevent Contamination from Defects in Metal Can Food Packaging

By Wayne D. Niemeyer
1 Comment

Millions of aluminum and tin-plated steel cans enter the marketplace every day, yet despite the extensive efforts of manufacturing plant quality control systems, a small percentage of the cans may have defects that can result in loss of the can integrity and subsequent contamination of the food products. Quality control operations within manufacturing plants typically have limited analytical chemistry capabilities and must rely on the manufacturer’s laboratory or independent laboratories to help identify and characterize the defects and troubleshoot the operations to eliminate the root cause of the defects. This article will present some of the current technology utilized for evaluating metal can defects.

Metal cans made from aluminum for beer and beverage products have been in use for about 50 years, whereas tin-plated steel cans for food products, have been in use for more than 100 years. Throughout that time, many improvements have been made to the design of the cans, the materials used for the cans (metal and internal/external protective organic coatings), the manufacturing equipment, chemical process monitoring, and quality control methods/instrumentation. The can manufacturing plants and their material suppliers are responsible for product integrity prior to distribution of the cans to food and beverage manufacturing operations throughout the world. Incoming quality control and internal quality control are also quite extensive at those manufacturing locations. Many of the can defects that would result in potential consumer issues are quickly eliminated from the consumer pipeline as a result of the rigorous quality control procedures. Occasionally, defective cans find their way into the marketplace, resulting in consumer complaints that must be addressed by the manufacturers.

The cause of the defects must be determined quickly, even if it means shutting down production lines while waiting for answers and corrective actions. Anything that results in a major product recall will have a high priority for the manufacturers to determine the root cause and take corrective actions. Major manufacturers have extensive analytical laboratories with a vast array of instrumentation and technical expertise for troubleshooting the defects. Smaller manufacturers usually have to rely on a network of independent laboratories to assist with their troubleshooting analyses.

Instrumentation and Methodology

Most major can manufacturing plants produce several hundred thousand to several million cans per day, and any can defects detected during quality control inspections will obviously have major implications. Most aluminum and tin-plated steel cans have an organic protective coating applied on the interior surface. One of the major quality control tests is to determine the amount of metal exposure inside the cans. This is done through the use of Enamel Rater instrumentation in which a sampling of cans are filled with an electrolyte. An electrode is immersed into the liquid and external contact is made with the can’s bottom or side wall. When a voltage is applied to the system, the current generated is directly proportional to the amount of exposed metal; a very small amount of exposed metal is acceptable. By reversing the polarity of the system, exposed metal regions produce gas bubbles as a result of the electrochemical reactions. This allows the inspector to identify the location of the exposed metal.  When too much metal exposure is encountered, the troubleshooting process begins immediately.

Crater defect, stereomicroscope
Figure 1. Stereomicroscope image of a crater defect with an iron oxide (rust) particle in the center. (Click to enlarge)

Visual examination of additional cans from the production line is done, followed by examination with a low-power microscope, typically a stereo microscope, in order to characterize metal exposure defects. Typical defects are craters and/or fisheyes, which are seen as circular dewetting (also known as pullback) of the coating from a solid contaminant on the metal (see Figure 1) or an incompatible liquid, such as machine oil mist (fisheye). Additionally, broken blisters in the coating, known as solvent pops, can occur in the curing oven for the coating, resulting in exposed metal. The metal exposure produces two main problems for the filled food product: Metal migration into the product and corrosion of the metal, which eventually results in perforation and product leakage. Manufacturing plants typically do not have the necessary analytical instrumentation available to identify the contaminants and must send selected samples to the laboratory for the analysis.

Another critical test that is conducted in the can manufacturing plants looks for adhesion characteristics of the internal coatings and external coatings (inks and over varnish). A typical adhesion test involves cutting open the sidewalls and immersing the cans into hot water for a period of time. Upon removal from the water, the cans are dried and a tool is used to scribe the coatings. A tape is applied over the scribe marks and rapidly pulled off. If any coating comes up with the tape, the troubleshooting process must begin. Often, over-cure and under-cure conditions can result in coating adhesion failure. The failure can also be caused by a contaminant on the surface of the metal. Loss of internal coating adhesion can result in flakes of the coating contaminating the product and also metal exposure issues. Adhesion failure analysis is typically conducted in the analytical laboratories.

Analytical laboratories are well equipped with a vast array of instrumentation used to identify and characterize various can defects, including:

  • Optical microscopes, both stereomicroscopes and compound microscopes, are used with a variety of lighting conditions and filters to observe/photograph the defects and in some cases perform microchemical tests to help characterize contaminants. They are also used to examine metal fractures and polished cross sections of metals looking for defects in the metal that may have caused the fractures.
  • Scanning electron microscope (SEM) equipped with the accessory for energy dispersive X-ray spectrometry (EDS) are used, in conjunction with the optical microscopes, to observe/photograph the defects in the SEM and then obtain the elemental composition of the defect material with the EDS system. This method is typically used for characterizing inorganic materials. Imaging can be done at much higher magnifications compared to the optical microscopes, which is particularly useful for analysis of fractures.
  • Infrared spectroscopy, commonly referred to as Fourier Transform Infrared (FTIR) spectroscopy, is used mainly to identify organic materials, such as, oils, inks, varnishes, cleaning chemical surfactants that are commonly found in the can manufacturing operations. Solvent extractions from adhesion failure metal surfaces and the mating back side of the coating are often done to look for very thin films of organic contamination.
  • Differential scanning calorimetry (DSC) instrumentation is often used to determine the degree of cure for protective coatings on cans exhibiting adhesion failure issues.

Other more specialized instrumentation that is more likely available in independent analytical laboratories includes:

  • X-ray photoelectron spectroscopy (XPS), also known as electron spectroscopy for chemical analysis (ESCA), is used to analyze the outermost molecular layers of materials. The technique is particularly useful for detecting minute quantities of contaminants, typically thin films involved in adhesion failures. Depth profiles can also be done on the metal to determine thickness of oxidation or the presence/absence of surface enhancement chemical treatments. High-resolution binding energy measurements on various elements can provide some chemical compound information as part of the characterization.
  • Secondary ion mass spectrometry (SIMS) is also an outer molecular layer type of analysis method. Depth profiling also be accomplished with this instrumentation, but one of the major advantages is the ability to detect boron and lithium which are found in some greases and other materials in the manufacturing facility. To help identify organic films that may have resulted in the adhesion failures, it is often crucial to know if boron or lithium is present, which helps identify a potential source.
  • X-ray diffraction (XRD) instrumentation is used to identify crystalline compounds, mainly inorganic materials but can also be used for certain organic materials. Inorganic materials, isolated from coating craters, are often identified with a combination of SEM/EDS and XRD analyses.

Three case studies are presented to show how analytical lab instruments can be used to identify and characterize metal can defects.Metal can defects can take on numerous forms, some of which have been discussed in this article. Extensive quality control activities in can manufacturing plants often prevent defective cans from entering the marketplace. Characterizing the cause of the defects often requires major troubleshooting activities within the production plants, supplemented by the analytical laboratories with a vast array of instrumentation and personnel expertise. Due to the huge quantities of metal cans produced each day, it is inevitable that some defective cans will make it to the marketplace, resulting in consumer complaints. High priorities must be assigned to consumer complaints to not only identify and characterize the defects, but also to determine how widespread the defective cans are within the marketplace. In this way, decisions can be made regarding product recalls.

Spherulites under can coating

Case Study: Using Analytical Lab Instruments to Find Defects in Cans

By Wayne D. Niemeyer
No Comments
Spherulites under can coating

Learn more about using current technology to evaluate defects in cans: “Prevent Contamination from Defects in Metal Can Food Packaging”


Case 1

Dark stains were observed on the outer surfaces of ends on tin-plated steel food cans when the cans came out of the retort sterilization system. During gentle scraping with a needle, it was determined that the stains were deposits on the surface of the clear organic protective coating. Portions of the deposits were mounted for analysis by SEM/EDS and revealed a composition mainly of iron oxide with elevated levels of calcium, chlorine and silicon. Other minor and trace elements included sodium, magnesium, aluminum, phosphorus, potassium, and zinc. It was concluded that the residues were water salts and iron corrosion products, which would be consistent with retort water residue. Apparently the retort water was not sufficiently rinsed from the cans upon exiting the retort system. These deposits, being rather loosely adhered to the surface of the coating, could easily wash off into the product when the steel ends are opened with a circumferential can opener.

Case 2

Drawn & Ironed (D&I) tin plated steel food cans are formed in high-speed machines using an emulsified lubricant in the tooling. The cans then go through a cleaning process and as a final step in the process, a water-soluble organic coating, known as a wash coat, is put on the outside of the cans by a flow curtain application method. Numerous consumer complaints were received in which the internal protective coating on the cans was losing adhesion and depositing into the product brine. Examination of the interior sidewalls of sample cans revealed film-like stains near the top of the cans where the adhesion failure was occurring. FTIR analysis of the stains identified them as the wash coat. In this case, some of the wash coat had migrated into the inside of the cans by capillary action during the can washing process. The internal protective coating that was applied later in the can manufacturing operation was not compatible with the wash coat. Several corrective actions had to be taken, which included some modifications to the wash coat flow curtain system and reformulations of the wash coat and internal coatings to make them more compatible for adhesion.

Case 3

Spherulites under can coating
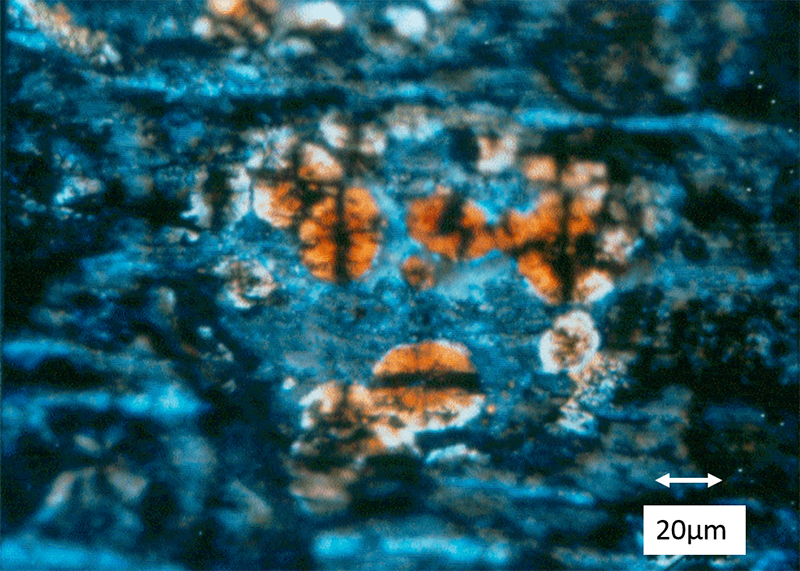
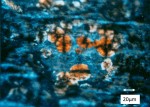
Figure 1. Polarized light microscope image, with fully crossed polarizing filters, of the spherulites under the can coating. Click to enlarge

Consumer complaints were received concerning orange/brown stains in or under the internal protective coating of tin-plated steel food cans. Optical microscopy examination revealed that the stains were underneath the coating. Polarizing filters, added to the compound microscope, revealed more optical properties of the stains as shown in Figure 1. They appeared as clusters of spherulites with black crossing lines, known as isogyre lines, and seemed, at first, like typical starch grains. The coating was carefully sliced away with a razor blade in order to expose the spherulites. SEM/EDS analysis of the exposed spherulites revealed high iron, carbon and oxygen content. In order to obtain a better identification of the spherulites, a portion of the can wall was placed into a low-temperature ashing system that removed the organic coatings exposing the spherulites, which could then be isolated and mounted for analysis by XRD. The analysis revealed that the spherulites were iron carbonate. To further confirm the carbonate composition, additional spherulites were mounted on a glass microscope slide and covered with a thin glass coverslip. While observing with a stereo microscope, a drop of 1N HCl acid was placed at the side of the coverslip to wick under the coverslip to make contact with the spherulites. Upon contact with the acid, the spherulites dissolved while emitting large quantities of gaseous bubbles, which is indicative of carbon dioxide gas evolution when carbonates are dissolved in acid.

Imports

FSMA’s FSVP: Clearing the Confusion of Importing Rules

By Charles Breen
No Comments
Imports

On November 27, 2015, the Foreign Supplier Verification Programs for Food Importers (FSVP Rule) published in the Federal Register. The most significant new element is that importers are now responsible for assuring that the food they import complies with FDA requirements. Instead of action against violative food, FDA is now equipped to take regulatory action against importers that fail to provide necessary assurance of food safety.

“Importer” is defined as: “the U.S. owner or consignee of an article of food that is being offered for import into the United States. If there is no U.S. owner or consignee of an article of food at the time of U.S. entry, the importer is the U.S. agent or representative of the foreign owner or consignee at the time of entry, as confirmed in a signed statement of consent to serve as the importer under the FSVP regulations.” This differs from the importer of record as defined by Customs and Border Protection (CBP) as the person primarily responsible for paying any duties or an authorized agent acting on his behalf.

Under FSVP, an importer’s basic responsibilities are to:

  • Determine hazards reasonably likely to cause illness or injury
  • Evaluate the risk, using hazard analysis
  • Evaluate the foreign supplier’s performance
  • Perform supplier verification activities

Determining hazards and evaluating risk parallel the preventive control rules for human food (PCHF) and animal food (PCAF). Evaluation of a foreign supplier’s food safety performance and conducting verification activities are substantially aligned with supply-chain verification in 21 CFR 117 Subpart F (PCHF) and 21 CFR 507 Subpart E (PCAF). The importer is responsible for assuring compliance with FDA standards and requirements.

Deciding what parts of FSVP are applicable to each importer’s operation requires a comparison between what the importer does, and the exemptions, exceptions and modified requirements offered in the rule. These depend on what is imported, the food safety system in country of origin, the size of the importer, and the size of the foreign supplier. FDA delivered on its promise of flexibility, but deciding what applies requires some analysis.

If a food importer meets the definition of importer and does not fall into an exempted category or qualify for exceptions or modifications, then some or all of the FSVP rule applies to them. FDA estimates that about 55,000 importers will be covered by FSVP or some portion of it.

Who Is an Importer?

The U.S. owner or consignee of an article of food that is being offered for import into the United States is the importer. If there is no U.S. owner or consignee of an article of food at the time of U.S. entry, the U.S. agent or representative of the foreign owner or consignee at the time of entry is the importer.

All importers must provide an identification number for each entry line of food that the importer brings into the country. FDA will be issuing more guidance on what it considers “an acceptable identification number.”  The agency is not mandating that each facility use a DUNS number, but is has ruled out other suggestions for the unique identification number that is required.

Exemptions to FSVP

FSVP does not apply to the following foods:

  • Fish and fishery products (in compliance seafood HACCP in 21 CRF 123)
  • Juice (in compliance with juice HACCP in 21 CFR 120)
  • Food for research or evaluation
  • Alcoholic beverages
  • Meat, poultry, and egg products regulated by USDA
  • Food imported for personal consumption,
  • Food that is transshipped through the United States
  • Food that is imported for processing and later export
  • U.S. food that is exported and returned without further manufacturing or processing in a foreign country (U.S. foods returned)

Partial exemption for import of low-acid canned foods (LACF). LACF are exempt from FSVP with respect to microbiological hazards for that food. To be exempt, the importer must verify and document that the food was produced in accordance with LACF requirements (21 CFR part 113). Other hazards not controlled by the LACF rule, if any, must be documented as controlled under FSVP.

Modified Requirements

Modified requirements for a receiving facility in compliance with the PCHF or PCAF rules that imports food:

  • If the process used controls the hazards of the imported food, the facility is considered in compliance with most of the FSVP rule.
  • If the food does not have any identified hazards requiring control, then the facility is considered in compliance with most of the FSVP rule.
  • If the facility has implemented a supply-chain program for the food in compliance with either PCHF or PCAF requirements, the facility is considered to be in compliance with most of the FSVP rule.

Receiving facilities must also accurately identify themselves to FDA for each entry line of food being imported.

Modified requirements for imported dietary supplements manufactured in compliance with CGMP requirements in 21 CFR part 111:

The importer must accurately identify itself to FDA for each entry line of dietary supplement or dietary ingredient being imported.

Modified requirements for very small importers:

Defined as less than $1 million in sales of human food a year, or less than $2.5 million in sales of animal food per year, very small importers would not have to conduct hazard analyses and would be able to verify their foreign suppliers by obtaining written assurances of compliance from those facilities.

Modified requirements for imports from small suppliers (i.e., qualified facilities under PCHF or PCAF, and some small farms not covered farms under the produce safety standards, and some small egg producers):

The importer must obtain written assurance before importing the food, and at least every two years after, that the foreign supplier is producing the food in compliance with applicable FDA food safety regulations or the laws and regulations of a country whose food safety system FDA has officially recognized as comparable or determined to be equivalent to that of the United States.

Modified requirements for food imported from a country with an officially recognized or equivalent food safety system:

Importers must determine that the supplier is in compliance with FDA requirements, or that the supplier is in compliance with food safety regulations or relevant laws in the country that FDA recognizes as equivalent.

At present, only New Zealand is officially recognized as comparable to the United States. FDA is in the process of auditing and evaluating audit results for mutual recognition with additional countries. The next countries to be recognized will most likely be Australia and Canada.

One final note: FSVP requires coverage of food contact surfaces, such as packaging. Manufacturers of food contact surfaces are not required to register with FDA. PCHF and PCAF rules are limited to those facilities required to register. The language requiring FSVP makes no exception for food contact surfaces.

Mobile technology and food safety

The Digital Revolution in Food Safety

By Manik Suri
2 Comments
Mobile technology and food safety

News concerning the safety of food seems to be everywhere these days. On a daily basis there’s a story about a salmonella outbreak or a company initiating a product recall due to possible contamination. Why is this the case?

If you visit most food businesses, whether it’s a restaurant, grocery store, manufacturer or foodservice operator, chances are you’ll see the same thing: Employees using pen and paper checklists, forms and log books to manage their food safety operations.

The recent E. coli outbreak traced to Chipotle Mexican Grill infected more than 50 people and led the company to shut down several restaurants. The outbreak was also a PR disaster for the company and damaged its reputation as a reliable provider of safe meals. Chipotle lost out on potential revenue and probably spent a good amount of money on hiring outside food safety consultants to examine its safety standards.

Since starting the business, Chipotle has remained focused on a core mission: Make great-tasting food, and more recently, food that is not modified with GMOs. While its goal has not changed, running a food company is vastly different today than in the past.

Modern Food Safety Isn’t So Modern

For one thing, there is a lot more paper to manage in today’s world. Between time and temperature controls, HACCP and HARPC requirements, and a whole host of industry certifications and brand standards, food businesses implement several safety processes. Even with advancements in technology, food safety operations are often run manually and therefore are error-prone.

In the early 1990s, food companies could handle the volume of paperwork themselves. Today, they’re swamped. Visit a food business, and you’ll see the same thing everywhere: Stacks of documents that need to be typed up and sent to food agencies. As one quality assurance manager recently stated, “We can barely keep track of them all.”

Surrounded by stacks of paper in their office, quality assurance (QA) managers explain that much of the pileup is due to more rules and regulations related to food safety. Food companies must comply with a growing number of local, state and federal laws that regulate food safety. The focus of recent laws such as FSMA is toward prevention of foodborne illness, placing even more emphasis on internal audits and recordkeeping. In addition to these laws, food companies must compete with the wealth of information available to customers about how their food safety operations work. Especially in the realm of social media, as Taco Bell has learned, one photo of an employee playing with food can lead to a PR nightmare.

A Day in the Life of a QA Manager

Complying with food safety laws often falls on a company’s QA manager who supervises food safety. She walks through the facility several times a day with clipboard in hand, reviewing a list of safety and quality measures.

The QA manager will then manually key this data into a spreadsheet, create reports, and file the results with industry partners and government regulators. These seemingly routine and time-consuming compliance tasks matter. Failing to comply with the appropriate laws can lead to costly penalties, permitting delays, loss of business from industry partners (such as retailers with strict requirements), and even legal action.

The legal requirements are often complex, overlapping, and they change every couple of years. The laws are designed, of course, to ensure that food preparation and delivery is safe, thereby protecting consumers. But an expanding body of regulations and fear of litigation have increased the time, cost and stress that play into compliance.

Mobile technology and food safety
Mobile tools can help companies improve food safety processes.

Improve Food Safety with Technology

So how can companies improve their food safety operations? By using food safety technology, particularly mobile software tools, to improve their processes. Since food safety operations are still manual, they tend to be hard to standardize and difficult to track—especially at larger companies where employees are working in multiple shifts across dozens of locations. Mobile food safety software offers several major benefits:

  • No More Pen and Paper. Replacing paper-and-pencil clipboards with digital tools saves time and money. Digital audits and task-lists can be logged and tracked, ensuring that staff are performing tasks in real-time. Digital entries are more accountable; managers can confirm when and where tasks where conducted and completed (including requiring photos to be taken). And digital clipboards can be loaded with reference materials like images and training videos, which helps staff learn best practices and prepare for real inspections by government agencies.
  • Quality and Safety Checklists. Instead of letting employees complete tasks ad hoc and make notes on clipboards and log books, companies can use quality and safety checklists to ensure that key tasks are standardized across the organization. For example, data can be collected to show that a company is always forgetting to label produce with an expiration date. Digital food safety and quality checklists that are loaded on smartphones or tablets makes it easier to ensure that all employees are following brand standards and best practices.
  • Automated Reports. Instead of sifting through binders filled with audit logs, food safety software captures and stores data in a structured format, making it easy to search and analyze. Why waste hours at the end of every week or month sifting through binders full of paper, when software lets you generate insights with the click of a button?
  • Real-Time, Centralized Management. Food companies often have multiple locations in which employees are conducting food safety operations in their own way. For companies that have multiple locations, mobile software being used by employees at each location can help corporate managers track performance by location, provide critical alerts, and give employees real-time feedback to help standardize food safety operations.

Here’s an example of a QA manager running a food safety audit using mobile software. During a random spot check, the manager shows up on the line with a smartphone in hand. As she walks around, she pulls up a food safety application and answers a series of pre-set multiple choices questions that cover key criteria, dictates comments into the device using the built-in voice recognition, and takes high-resolution color photos of several problematic issues. If a QA manager is unsure about food safety requirements, she can use her mobile device to quickly pull up a reference document (or even the official code citation) from state, FDA, USDA or other agencies.

After running a digital audit with food safety software, the QA manager can immediately print or e-mail a report that shows all of the items out of compliance, creating actionable intelligence for her team. The QA manager can then share this with line workers during their weekly team meeting, which help to train staff on best practices in food safety.

The data the QA manager collected through her mobile device is immediately stored in the cloud. From there it can be easily accessed by a colleague (i.e., her manager at corporate headquarters) at any time. Over time, the data from each of these spot checks is stored in a central database that a manager can analyze, looking for trends in performance, issues that keep arising, or locations that may need extra training and attention. Mobile software makes it easier to generate insights that can drive major improvements in an organization’s safety and performance.

By using software to help manage food safety audits, logs and line checks, businesses can save time and money on compliance, train staff on best practices, and most importantly, keep customers safe and satisfied.

Today, food safety technology, especially mobile software, should be a critical part of any modern food company’s operations. Mobile audit and task-management software allows QA managers to streamline and standardize quality and safety operations across large teams and multiple locations, helping save valuable time and money. Whether you’re a mobile food vendor or a large-scale food processor, modern software tools can help food businesses of all sizes effectively manage time-consuming tasks around food safety and compliance, from digitizing audit logs for analysis to created automated filings for supply chain partners.

How Automated Inventory Tracking Systems Contribute to Food Safety

By Ryan Hardy
No Comments

When a business decides to invest in technology, the primary driver is usually to save money over the long term. As with most automated systems, inventory management tools can reduce costs by saving time and resources used to manage inventory.

But the benefits that automated inventory tracking can provide through traceability (of lots, batches, and even individual items) go beyond the financial. These systems can also be used in every aspect of your food safety program from helping with compliance, to improving your quality controls.

Exchange knowledge about managing your supply chain at the Best Practices in Food Safety Supply Chain conference | June 5–6, 2017 | LEARN MORE

In a nutshell, having an automated system that allows full visibility into the supply chain—that is, one that identifies in real time where items are being used and where they are sent, while retaining a historical record of that flow through the chain—makes it much simpler and faster to implement procedures to ensure the safety of the food you produce.

All about Accuracy and Speed

Speed and accuracy make a huge difference when it comes to dealing with potentially contaminated food. Being faster and more accurate than a manual inventory method is the most immediate benefit that an automated system brings to your food safety program.

The most compelling reason for having accurate and readily accessible track-and-trace data is to handle food recalls and to comply with requests for documentation from government agencies such as the FDA. In cases where consumer health is at risk, that information needs to be delivered quickly to prevent further harm, and it must be accurate to enable investigators to move in the right direction. Responding to requests for detailed documentation within a 24-hour timeframe can be nearly impossible if you are not using an automated system.

Even when the situation doesn’t involve a federal investigation, once a situation in which possible contamination or mislabeling arises, the faster you have accurate and detailed data, the faster your internal processes can move forward.

If the issue is identified through your quality control process, you will be more likely to be able to prevent contaminated product from reaching the retail outlet and thus getting into the hands of the consumer. Having traceability built into your inventory management systems provides immediate knowledge about whether a product using ingredients from the same batch have entered the distribution chain, and if so, where they are going. This greatly improves the likelihood of limiting the cost and scope of a recall.

Depending on the specific technology you employ, an automated system can provide immediate access to the track and trace information for specific ingredients at least one step backward and one step forward, as required by the Bioterrorism Act of 2002. A supply chain that integrates the most sophisticated technology, such as DNA tracking, can trace an item all the way from the farm or border to the individual consumer or restaurant kitchen.

This traceability means that if an ingredient was already contaminated before it entered your production line, the inventory tracking system can identify all products using that ingredient from the contaminated lot and thus will help you define the scope of the problem. This automation can go a step further by identifying where the ingredient lot originated, and thus help trace the ingredient at least one step backward to the vendor. If the vendor (whether a distribution company or a direct supplier) has traceability in an automated system, or if you are using a system hosted by a distribution partner, tracing the source farther back than one step is possible.

Such information can help you respond more quickly to FDA requests for product information and support the agency’s efforts in product traceability.

Protect Your Reputation

Just as using tracing technology can help identify potential contamination sources quickly, it can also be used to eliminate sources more quickly and accurately, thereby speeding up investigations into food contamination incidents. The faster a company can be eliminated from an investigation, the less time is taken away from normal production. In addition, quick exclusion can protect a company’s reputation from harm.

Additional Benefits

Through their ability to store specific data that can be used to identify potential risks, automated track and trace systems contribute to many preventive food safety measures as well as to the following corrective responses:

  • For perishable products, automated traceability can identify how long specific perishables have been in supply chain. This allows you to avoid using ingredients close to spoilage and to remove overdue products from the distribution chain.
  • During mock recalls, automated tracking systems reduce the time spent away from regular production and allow you consistent information throughout the organization, eliminating wasted effort due to miscommunications.
  • Automated systems reduce the time needed for notifications both internally and externally in the case of an incident affecting food quality or safety. This leads to faster line clearance and faster isolation of the possibly contaminated product.
  • With more effective accounting for possibly affected batches, you can better identify where to apply cleanup measures in the production chain.

In short, automated tracking can improve implementation of preventive controls to stop the contaminated product from reaching the marketplace, and in cases in which corrective actions are required, the automated system can help you respond more quickly and can reduce the scope of risk.

Not just Foodstuffs

Although raw ingredients and food products obviously require traceability, they aren’t the only traceable inventory that can impact food safety. Automated lot tracking can enhance food safety efforts related to all inventory items used in food processing/manufacturing:

  • Packaging. A sub-standard packaging lot can allow incursion of harmful substances or the growth of harmful bacteria. Leakers can contaminate an entire batch of meat or poultry product. Automated lot tracking can help you rapidly isolate the bad lot and know which production lines have already used the sub-standard materials.
  • Labeling. If an inferior adhesive has been applied to a batch of labels, you can identify which product lots to pull from the distribution chain. You can do the same if your quality controls find a batch of inaccurate labels.
  • Protective equipment and clothing. Gloves, masks and other protective gear must function properly to ensure the safety of your workers and also to prevent contamination from being introduced on the production line. An inferior batch of protective gloves that tear during use, for example, could violate your food safety practices. Identifying the bad batch quickly and removing it from the operations area immediately can save potential contamination.
  • Cleaning solutions. Even a batch of cleaning solution can be sub-par. If tests show that cleaning has not eliminated the targeted bacteria, for example, you can more quickly take measures to determine whether the root cause of the problem was a procedural issue or a quality issue with the batch of cleaner.

Beyond the Production Line

The benefits of automated tracking systems to your food safety program extend beyond the production line. They can also enhance decision-making, vendor management and communications functions.

When it comes to potential contamination, decision making needs to be both timely and based on the best information available. Automated systems can provide you with accurate information quickly to help you answer these and other key questions, so that the decision on what actions to take can be based on good information:

  • How widespread is the potential contamination?
  • Where is the product in the production and distribution chains?
  • Have we already exposed consumers?

These systems can put the answers to these questions in front of the appropriate decision makers early in the process. The technology can be configured to allow access to the data via a browser, so if those who make the final decisions are located elsewhere, they can see in real time the same information that you are seeing in the plant. This makes communication about potential contamination more effective and clear, since everyone can see the same thing at the same time, and it can eliminate the potential for miscommunication up the chain of command.

By identifying where bad lots entered your supply chain, automated track-and-trace can enhance supplier accountability. You can accurately see if you have vendors with recurring issues in the quality of the supplies they are providing.

Automated Inventory Tracking Technologies

An automated inventory tracking system depends on three components:

  • A physical component, such as a label or tag, which contains detailed information identifying the specific lot or item.
  • A database, where each discrete data item is stored.
  • A reporting interface that allows people to access and use the identification information. This is the programming code that performs searches, retrieves the data, and formats the information in a formatted report, which is then presented on the screen, saved to a file, or sent to a printer.

The most common physical components used by automated inventory tracking systems rely on barcode or RFID technology, or a combination of both. The choice of which technology to use to integrate into the inventory management database layer of the system depends on a number of factors, but both have been proven extremely accurate (some sources say up to 99%). What is more important than the choice of tracking tools is the quality of the data encoded in them.

The latest in tracking technology uses an engineered DNA marker, in the form of an edible spray. When applied to produce, this DNA marker can track the individual item (i.e., an apple, head of lettuce or onion), along the entire food supply chain, identifying where it was farmed, the date it was picked, and where it was processed.

Whatever form of technology you employ, ensuring that your data is complete and accurate and can be integrated into both your supply and distribution chain is critical to realizing the benefits of that system in supporting your food safety efforts.

The WDS Food Safety Team also contributed to this article.